

[Sugar Cane Pneumatic Conveying: A Material Handling Solution to Overcome Distance Limitations]
Efficient material handling is a critical factor in the sugar industry, where the transportation of raw materials like sugar cane or processed sugar products requires reliable and effective systems. Traditional methods such as belt conveyors or manual handling often face limitations when it comes to long-distance transport, especially in large-scale sugar processing facilities. This is where pneumatic conveying systems offer a compelling alternative, providing a solution that can overcome distance barriers while maintaining efficiency and product integrity.
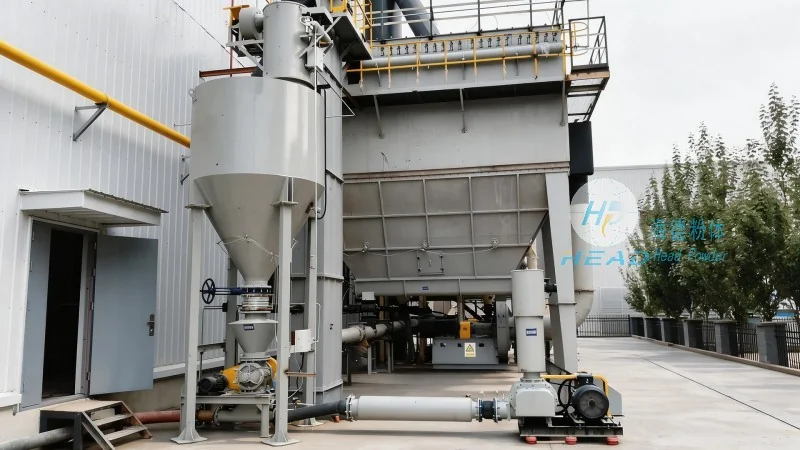
Pneumatic Conveying Technology for Sugar Processing
Pneumatic conveying, also known as air-powered conveying, utilizes compressed air to transport bulk materials through a pipeline system. This method is particularly suitable for sugar cane and other granular or powdered materials, as it minimizes product degradation, dust generation, and contamination compared to mechanical systems. The technology works by creating a pressure differential within the pipeline, which draws the material along with the air stream, ensuring a smooth and continuous flow from the source to the destination.
Overcoming Distance Limitations with Advanced Pneumatic Solutions
One of the key advantages of pneumatic conveying for sugar processing is its ability to transport materials over significant distances without the need for intermediate transfer points or complex infrastructure. Unlike traditional conveyor belts that may require multiple segments and support structures, pneumatic systems can span long distances with a single, continuous pipeline, reducing installation costs and operational complexity. This capability is especially valuable in large sugar mills where raw materials need to be moved from storage areas to processing units or from processing stages to packaging facilities, often covering distances of several hundred meters or more.
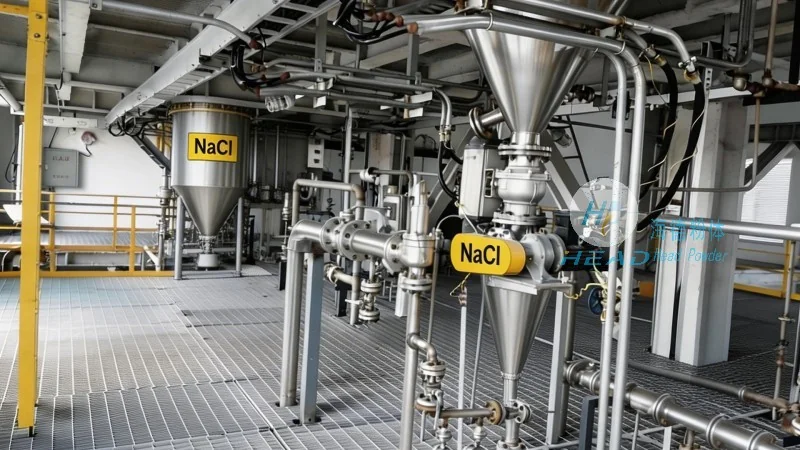
HeadPowder Engineering: Expertise in Sugar Cane Pneumatic Conveying
Shandong HeadPowder Engineering Co., Ltd., a leading provider of material handling solutions, specializes in designing and implementing advanced pneumatic conveying systems tailored to the specific needs of the sugar industry. With years of experience in the field, HeadPowder has developed a comprehensive range of solutions that address the unique challenges faced by sugar processing facilities. The company's expertise lies in understanding the physical properties of sugar cane and processed sugar products, such as moisture content, particle size, and flow characteristics, and tailoring the conveying system to optimize performance and efficiency.
Key Features and Benefits of HeadPowder's Pneumatic Conveying Systems
HeadPowder's pneumatic conveying systems for sugar processing offer several key features that enhance operational performance and product quality. These include: high conveying capacity to handle large volumes of sugar cane or sugar products efficiently; low maintenance requirements due to the absence of moving parts in the pipeline, reducing downtime and operational costs; flexible system design that allows for easy integration with existing processing equipment and future expansion; and environmental friendliness with minimal dust generation and reduced energy consumption compared to traditional mechanical systems.
Customized Solutions for Diverse Sugar Processing Applications
Every sugar processing facility has unique requirements, and HeadPowder recognizes the importance of providing customized solutions that meet these specific needs. Whether the application involves transporting raw sugar cane from fields to the mill, moving refined sugar from processing units to storage silos, or handling byproducts such as molasses, the company's engineers work closely with clients to design a system that maximizes efficiency and minimizes operational challenges. The solutions are designed to handle varying material characteristics, including different moisture levels, particle sizes, and flow rates, ensuring consistent performance across different stages of the sugar production process.
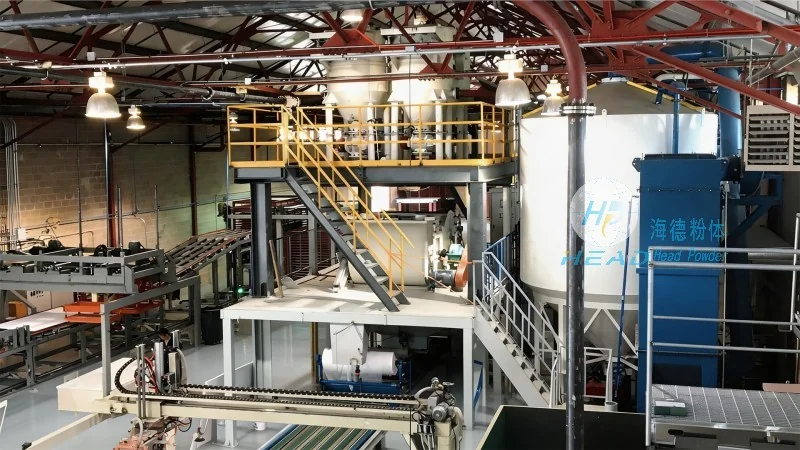
Ensuring Product Integrity and Safety in Pneumatic Conveying
Product integrity is paramount in the sugar industry, and HeadPowder's pneumatic conveying systems are engineered to maintain the quality of sugar products throughout the transport process. The systems use gentle handling techniques that minimize product breakage, caking, or contamination, preserving the quality and market value of the final product. Additionally, the company prioritizes safety in its designs, incorporating features such as pressure relief valves, air filtration systems, and emergency shut-off mechanisms to ensure safe operation and compliance with industry standards.
Conclusion: The Future of Sugar Cane Material Handling
As the sugar industry continues to evolve and face increasing demands for efficiency and cost-effectiveness, pneumatic conveying systems offer a forward-thinking solution to traditional material handling challenges. With its ability to overcome distance limitations and provide reliable, efficient transport of sugar cane and processed sugar products, pneumatic conveying is becoming an essential component of modern sugar processing facilities. Shandong HeadPowder Engineering Co., Ltd. remains at the forefront of this technology, providing innovative and customized solutions that help sugar mills optimize their operations and achieve sustainable growth.