

Detailed Explanation of Silica Fume Pneumatic Conveying Systems
When it comes to handling and transporting silica fume—a fine, pozzolanic material widely used in concrete production—efficient and reliable systems are essential. The HeadPowder brand, representing Shandong HeadPowder Engineering Co., Ltd., specializes in advanced pneumatic conveying solutions tailored for silica fume applications. This article provides a comprehensive overview of the silica fume pneumatic conveying system, highlighting its design, functionality, and industrial advantages.
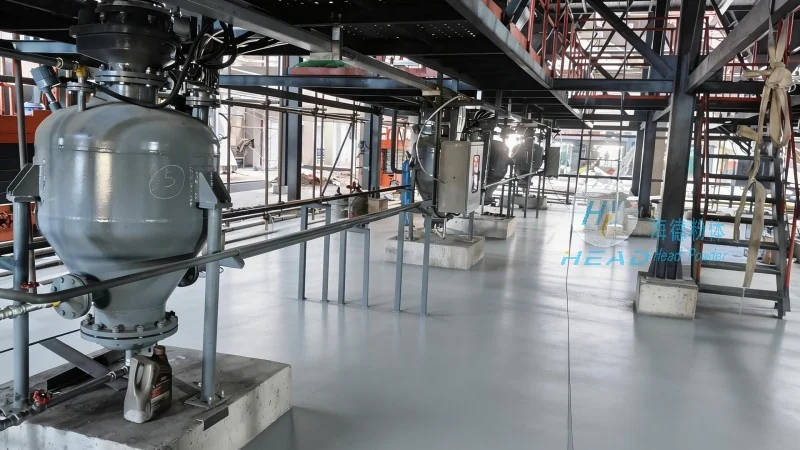
Understanding Silica Fume and Pneumatic Conveying Technology
Silica fume, also known as microsilica, is a byproduct of silicon metal or ferrosilicon production. It consists of extremely fine particles (typically 0.1–0.2 microns) that enhance concrete strength, reduce permeability, and improve durability. Traditional handling methods like bagging or manual loading can be labor-intensive and inefficient, leading to dust exposure and material loss. Pneumatic conveying offers a solution by using air to transport bulk materials through pipelines, minimizing handling steps and ensuring a clean, controlled process.
Key Features of the HeadPowder Silica Fume Pneumatic Conveying System
The HeadPowder silica fume pneumatic conveying system is engineered to address the unique challenges of silica fume transport. Key features include:
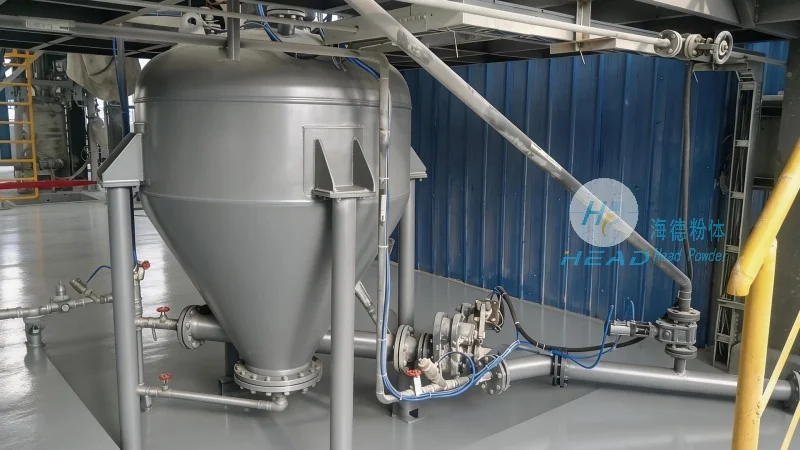
- High-precision air flow control to maintain consistent material velocity, reducing particle degradation and system wear.
- Specialized material handling components, such as rotary valves and cyclone separators, designed to handle fine, abrasive particles without clogging or damage.
- Integrated dust collection and filtration systems to comply with environmental regulations and ensure workplace safety.
- Modular design for easy installation and scalability, allowing systems to adapt to varying production volumes and facility layouts.
Technical Specifications and Performance Metrics
The system is built to meet rigorous industrial standards, with performance metrics tailored for silica fume applications:
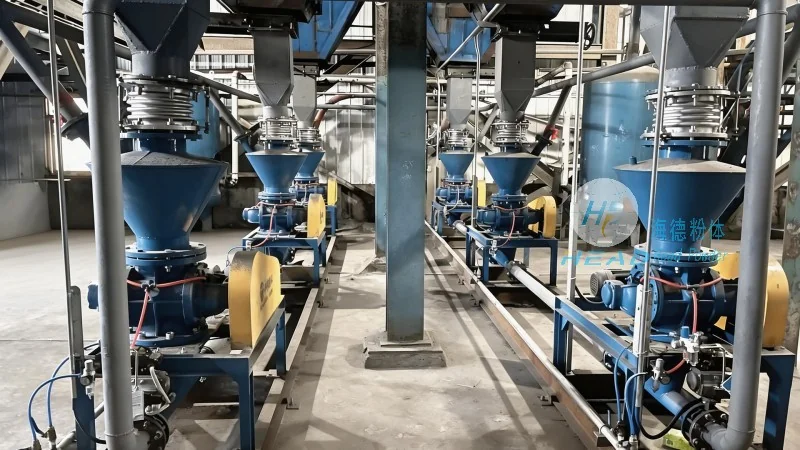
- Maximum conveying capacity: Up to 50 tons per hour, depending on pipeline length and air pressure.
- Operating pressure range: 0.5–1.5 bar (7.25–21.75 psi), adjustable to match facility requirements.
- Particle size compatibility: Effective for particles as fine as 0.1 microns, ensuring no loss or degradation during transport.
- Energy efficiency: Optimized air consumption reduces operational costs while maintaining high throughput.
Application Scenarios and Industry Benefits
The HeadPowder silica fume pneumatic conveying system is widely adopted in the cement, concrete, and construction materials industries. Its benefits include:
- Improved material handling efficiency, reducing labor costs and minimizing downtime.
- Enhanced product quality through consistent mixing and reduced contamination.
- Compliance with environmental regulations by minimizing dust emissions and waste.
- Increased production flexibility, allowing seamless integration with existing manufacturing lines.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a division of Shandong HeadPowder Engineering Co., Ltd., is a leading manufacturer of pneumatic conveying systems in China. With operations based in Shandong, the company combines decades of engineering expertise with advanced technology to deliver customized solutions for bulk material handling. The company’s commitment to quality, reliability, and customer satisfaction has established it as a trusted partner in the construction materials sector. For businesses seeking to optimize silica fume transport, HeadPowder offers tailored systems that enhance operational efficiency and product quality.