

Pharmaceutical Pneumatic Conveying Turnkey Systems
Pharmaceutical pneumatic conveying systems represent a critical component in modern pharmaceutical manufacturing, offering efficient, safe, and reliable material handling solutions. These turnkey projects are designed to meet the stringent requirements of the pharmaceutical industry, ensuring compliance with regulatory standards while optimizing operational efficiency.
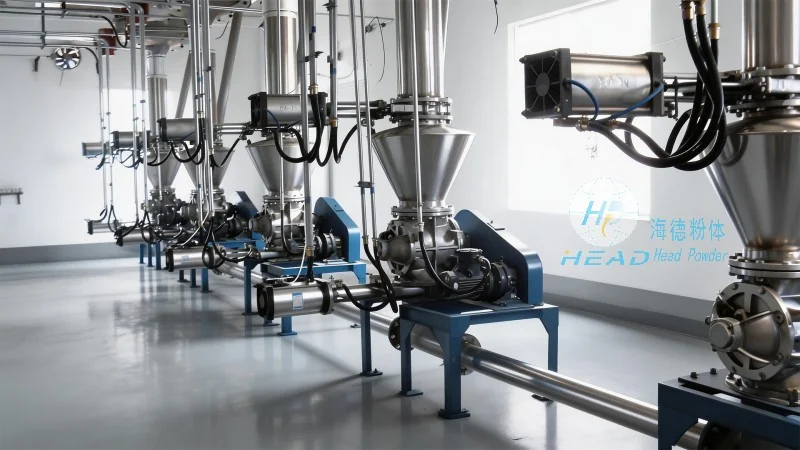
Introduction to Pharmaceutical Pneumatic Conveying Systems
Our company, Shandong HeadPowder Engineering Co., Ltd., specializes in the design, development, and implementation of comprehensive pharmaceutical pneumatic conveying systems. These systems utilize air or other gases to transport bulk powders and granules, providing a dust-free, closed-loop operation that minimizes contamination risks and enhances product integrity. The turnkey nature of our solutions ensures that clients receive a fully integrated system, from initial design and engineering to installation, commissioning, and ongoing support.
About Shandong HeadPowder Engineering Co., Ltd.
Headpowder, the professional brand of Shandong HeadPowder Engineering Co., Ltd., is a leading provider of advanced material handling solutions tailored for the pharmaceutical sector. With a strong presence in China, particularly in Shandong, our company has built a reputation for delivering high-quality, customized systems that address the unique challenges of pharmaceutical production. Our team of experienced engineers and technicians leverages cutting-edge technology and industry expertise to develop solutions that meet the evolving needs of the pharmaceutical industry.
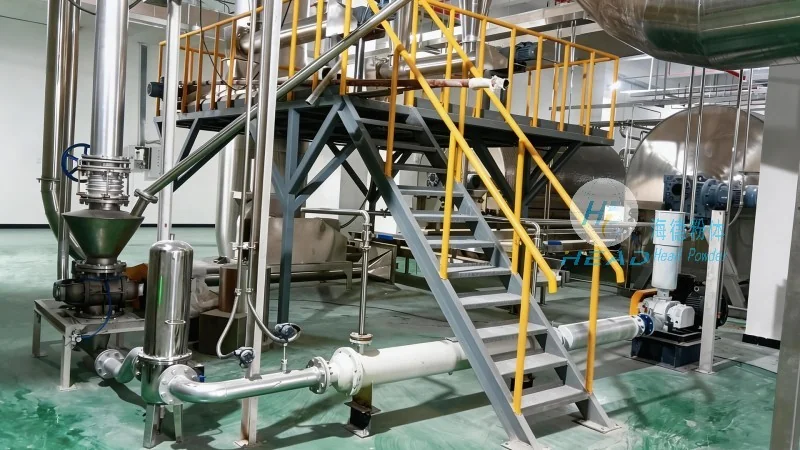
Key Features of Our Turnkey Solutions
Our pharmaceutical pneumatic conveying turnkey projects are characterized by several key features that set them apart in the industry. Firstly, the systems are engineered to operate in a closed environment, preventing dust contamination and ensuring product purity. This is achieved through advanced filtration and air purification systems that maintain a clean air quality within the conveying lines. Secondly, the systems are designed for high efficiency, with optimized air flow and pressure control mechanisms that minimize energy consumption while maximizing material throughput. Additionally, our solutions incorporate user-friendly control panels and monitoring systems, enabling real-time tracking of operational parameters and facilitating quick troubleshooting.
Technical Advantages and Application Benefits
The adoption of pharmaceutical pneumatic conveying systems offers numerous technical advantages and practical benefits for pharmaceutical manufacturers. From a technical standpoint, these systems provide a dust-free and hygienic material handling process, which is essential for maintaining product quality and meeting regulatory compliance. The closed-loop design reduces the risk of cross-contamination between different batches, enhancing product safety. From an operational perspective, the systems improve production efficiency by reducing downtime associated with manual handling and material transfer. Furthermore, the compact design of our systems allows for flexible integration into existing production facilities, minimizing space requirements and installation complexities.
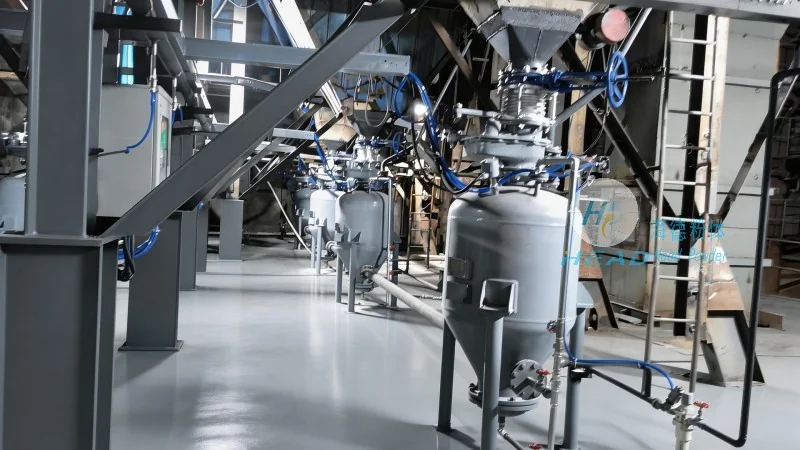
Customization and Integration Capabilities
At Shandong HeadPowder Engineering Co., Ltd., we understand that each pharmaceutical facility has unique operational requirements and space constraints. Therefore, our turnkey solutions are highly customizable to meet specific client needs. We work closely with clients to design systems that align with their production processes, material characteristics, and regulatory obligations. Our engineering team can integrate various components, such as feeders, classifiers, and storage silos, into a cohesive system that ensures seamless material flow from raw material input to final product packaging. This level of customization ensures that the system operates at peak performance while adhering to the highest standards of safety and efficiency.
Quality Assurance and Compliance Standards
Quality is at the core of our operations, and all pharmaceutical pneumatic conveying systems are developed and manufactured in accordance with international quality standards and industry regulations. Our company adheres to strict quality control protocols throughout the entire production process, from component sourcing to final system testing. This ensures that each system meets the rigorous requirements of the pharmaceutical industry, including compliance with GMP (Good Manufacturing Practice) guidelines and other relevant regulatory frameworks. We also provide comprehensive documentation and certification to support client compliance and audit processes, providing peace of mind regarding the quality and reliability of our solutions.