

What is a Powder Bin Powder Handling System? What are its Design Principles?
A powder bin powder handling system is a specialized industrial solution designed to store, transport, and manage bulk powders efficiently. These systems are critical in various industries, including pharmaceuticals, food processing, and chemical manufacturing, where precise handling of powders is essential for product quality and operational safety. The system typically consists of a storage bin, feeding mechanisms, and conveying equipment that work in tandem to ensure smooth material flow from storage to processing or packaging stages.
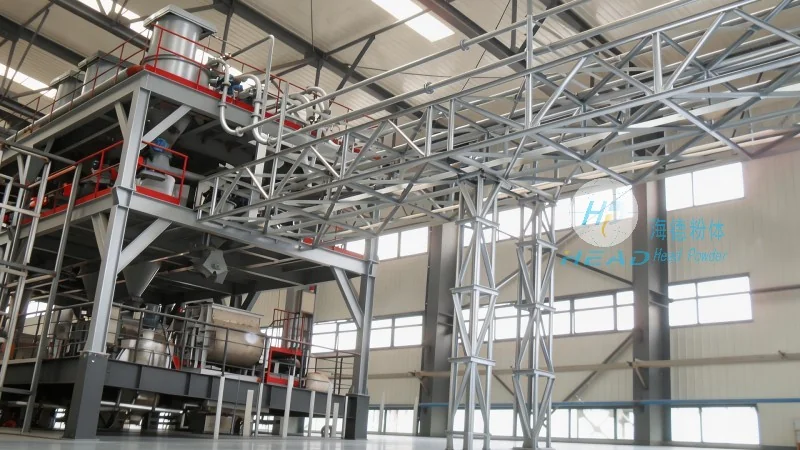
Key Components of a Powder Bin System
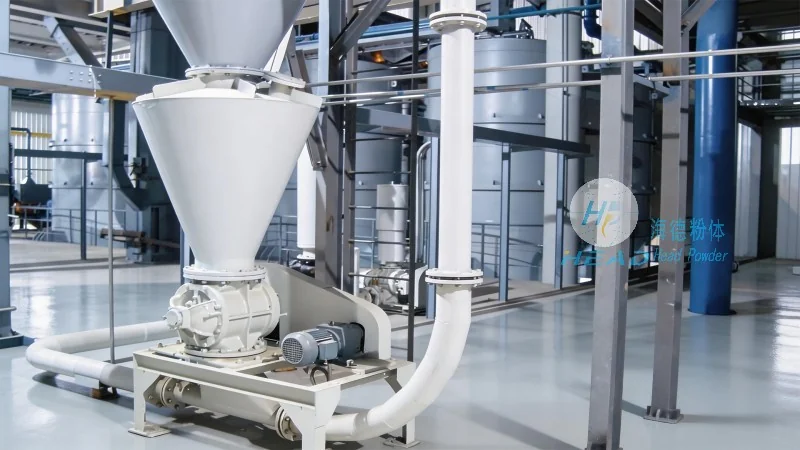
The core components of a powder bin powder handling system include the storage bin itself, which is often made from durable materials like stainless steel or food-grade plastics to prevent contamination and ensure longevity. The bin is equipped with a hopper or outlet at the bottom to facilitate material discharge. Feeding devices, such as rotary valves or vibratory feeders, are integrated to control the flow rate and consistency of the powder discharge. Conveying systems, including pneumatic or mechanical conveyors, transport the powder from the bin to the processing equipment. Additionally, the system may include dust collection and filtration components to maintain air quality and comply with environmental regulations.
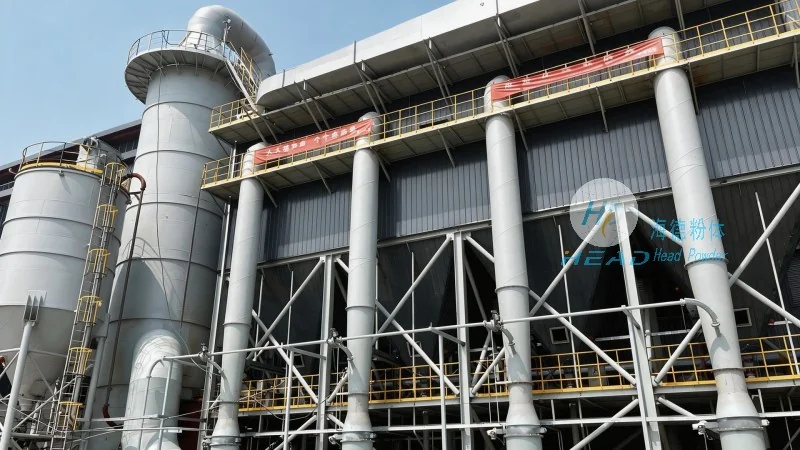
Design Principles for Efficient Powder Handling
The design of a powder bin powder handling system is guided by several key principles to ensure optimal performance. First, the system must address the unique challenges of powder flow, such as bridging, arching, or segregation, which can impede material movement. Engineers employ techniques like bin design optimization, including the use of conical or hopper-shaped bins with appropriate angles to promote smooth flow. Second, the system prioritizes material containment and safety, with features like sealed bins and explosion-proof designs to prevent dust explosions and ensure worker safety. Third, the system is built for scalability and adaptability, allowing for adjustments to accommodate different powder types, flow rates, and processing requirements. The integration of sensors and control systems further enhances operational efficiency by monitoring flow rates, pressure, and other critical parameters in real-time.
Application in Industrial Settings
Powder bin powder handling systems are widely used in industries where bulk powder handling is a standard practice. In pharmaceutical manufacturing, these systems ensure the safe and hygienic handling of active pharmaceutical ingredients (APIs) and excipients, maintaining compliance with stringent regulatory standards. In the food industry, they are used to handle ingredients like flour, sugar, and spices, ensuring consistent quality and preventing contamination. In chemical processing, the systems manage raw materials and intermediates, supporting processes like mixing, blending, and packaging. The versatility of these systems makes them indispensable in any facility where bulk powders need to be managed efficiently and reliably.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd. is a leading manufacturer of powder handling equipment, specializing in the design and production of high-quality powder bin systems. With headquarters in Shandong, China, the company has built a reputation for delivering reliable, efficient, and cost-effective solutions tailored to the specific needs of its clients. HeadPowder's team of engineers and technicians leverages advanced technology and industry expertise to develop systems that meet or exceed industry standards. The company's commitment to quality and customer satisfaction has made it a trusted partner for businesses across various sectors, providing them with the tools they need to optimize their powder handling processes and enhance overall operational performance.