

What is a Positive Pressure Powder Conveying System? And Its Design Principles?
Positive pressure powder conveying systems are specialized equipment used to transport bulk powders and granular materials from one location to another. Unlike traditional vacuum systems, these systems operate by generating positive pressure within the conveying line, ensuring that the material is continuously pushed forward through the pipeline. This approach offers several advantages, including efficient material handling, reduced product degradation, and enhanced safety in handling potentially hazardous powders. The core of such a system lies in its design, which integrates various components to achieve reliable and effective powder transport.
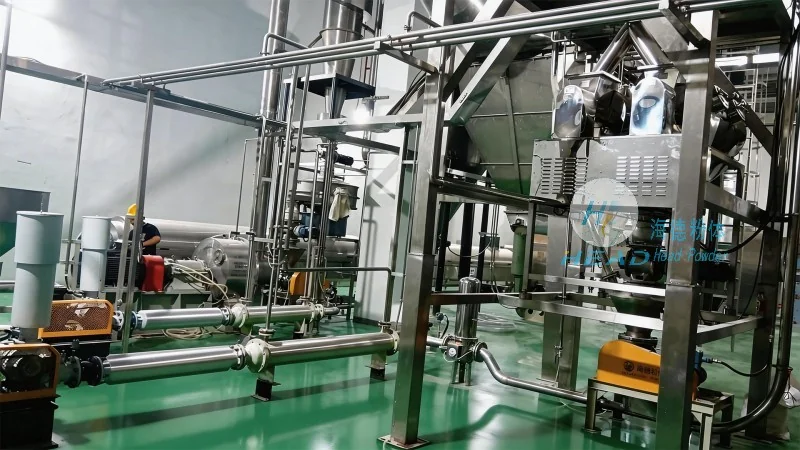
Key Components and Design Principles of Positive Pressure Powder Conveying Systems
The design of a positive pressure powder conveying system typically involves several critical components, each playing a vital role in the overall operation. The system generally consists of a powder feeder, a positive displacement blower or compressor, a conveying pipeline, and a discharge device. The powder feeder is responsible for metering and feeding the material into the system, ensuring a consistent flow rate. The positive displacement blower or compressor provides the necessary pressure to move the material through the pipeline. The conveying pipeline, often made of materials like stainless steel or plastic, is designed to withstand the pressure and prevent material leakage. The discharge device, such as a rotary valve or a dust collector, controls the release of the material at the destination.
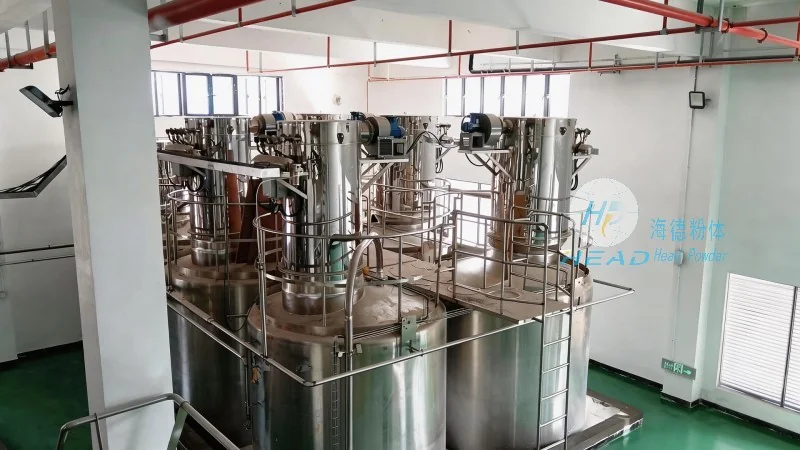
How Positive Pressure Conveying Works: A Step-by-Step Explanation
When the system is activated, the powder feeder releases the material into the pipeline. The positive displacement blower then generates a high-pressure air stream that pushes the powder forward. As the material moves through the pipeline, it is carried by the air stream, which maintains the material's suspension and prevents clogging. The pressure within the system is carefully controlled to ensure that the material is transported efficiently without excessive pressure loss. At the end of the pipeline, the discharge device regulates the release of the material, allowing it to be deposited into a storage bin or processing equipment. This process is continuous and can handle large volumes of material with minimal maintenance.
Advantages of Positive Pressure Powder Conveying Systems
Positive pressure powder conveying systems offer numerous benefits over other conveying methods. One of the primary advantages is the ability to handle a wide range of materials, including those that are abrasive, sticky, or prone to bridging. The positive pressure design prevents material buildup and ensures consistent flow, reducing the risk of product degradation. Additionally, these systems are more energy-efficient compared to vacuum systems, as they operate at lower pressures and use less power. The enclosed pipeline design also enhances safety by containing dust and preventing exposure to airborne particles. This makes them ideal for applications in pharmaceuticals, food processing, and chemical industries where product purity and worker safety are paramount.
Applications and Industries Served by Positive Pressure Conveying Systems
Positive pressure powder conveying systems are widely used in various industries that require the handling of bulk powders. In the pharmaceutical industry, these systems are essential for transporting raw materials and finished products, ensuring that the materials remain sterile and free from contamination. In the food processing sector, they are used to convey ingredients like flour, sugar, and spices, maintaining the quality and safety of the food products. The chemical industry also relies on these systems for transporting powders such as pigments, catalysts, and reagents, which may be hazardous or sensitive to moisture. Other applications include the handling of minerals, fertilizers, and construction materials, where efficient and reliable transport is crucial for production efficiency.

About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of advanced powder handling equipment. With a focus on innovation and quality, the company specializes in designing and producing positive pressure powder conveying systems tailored to the specific needs of various industries. HeadPowder's products are known for their durability, efficiency, and compliance with industry standards. The company is committed to providing reliable solutions that enhance productivity and ensure product integrity. HeadPowder's headquarters is located in Shandong, China, where the company conducts research, development, and manufacturing to meet global market demands.