

What is a Fly Ash Silo Powder Conveying System Equipment? What Are Its Design Principles?
At Shandong HeadPowder Engineering Co., Ltd., we specialize in providing advanced solutions for the efficient handling and transportation of fly ash, a byproduct of coal combustion. The fly ash silo powder conveying system equipment is a critical component in modern industrial processes, designed to ensure safe, reliable, and efficient movement of this fine powder material. This article explores the functionality of such systems and delves into the underlying design principles that make them effective.
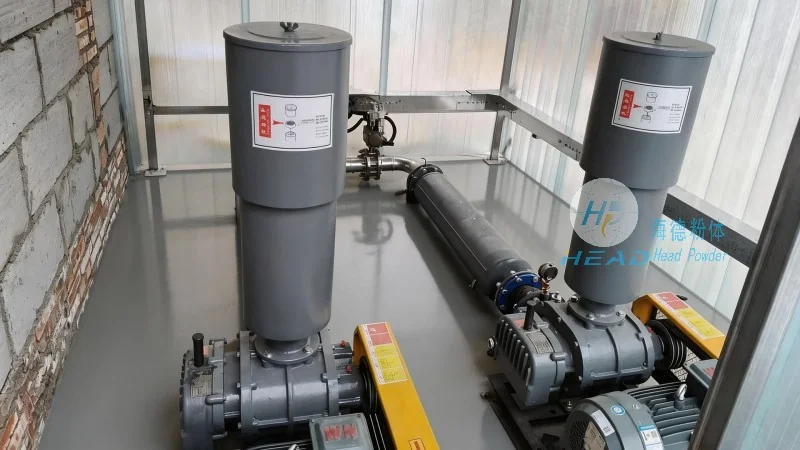
Key Components of the Fly Ash Conveying System
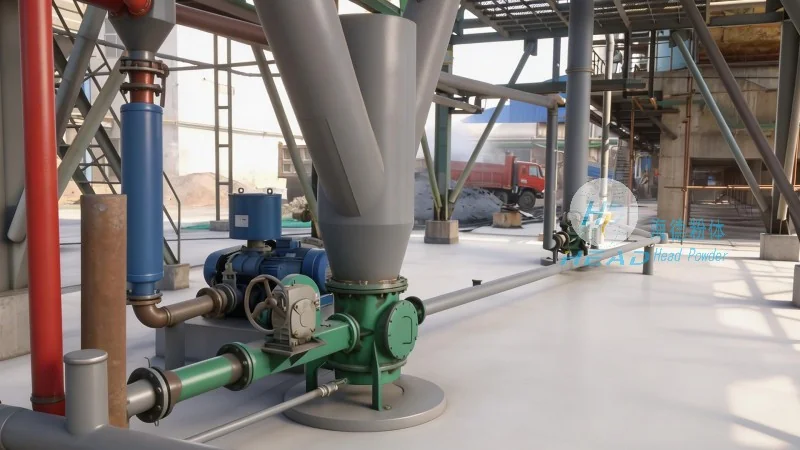
The fly ash silo powder conveying system typically consists of several key components that work in tandem to achieve optimal performance. These include the fly ash silo itself, which serves as the storage vessel for the material; a conveying mechanism, such as a screw conveyor, pneumatic conveyor, or belt conveyor, depending on the specific application; and control systems that regulate the flow and operation of the equipment. Each component is engineered to handle the unique properties of fly ash, including its fine particle size, moisture content, and potential for dust generation.
Design Principles for Efficient Material Handling
The design of a fly ash silo powder conveying system is guided by several fundamental principles aimed at maximizing efficiency, safety, and reliability. One of the primary considerations is the prevention of material buildup and blockages, which can occur due to the cohesive nature of fly ash. To address this, the system incorporates features like anti-stick coatings on silo walls, proper angle of repose in the silo design, and regular maintenance schedules. Additionally, the conveying mechanism is designed to minimize friction and wear, ensuring long-term durability and low maintenance costs. The control systems are equipped with sensors and monitoring tools to detect anomalies in flow rates, pressure, or temperature, allowing for immediate intervention to prevent system failures.
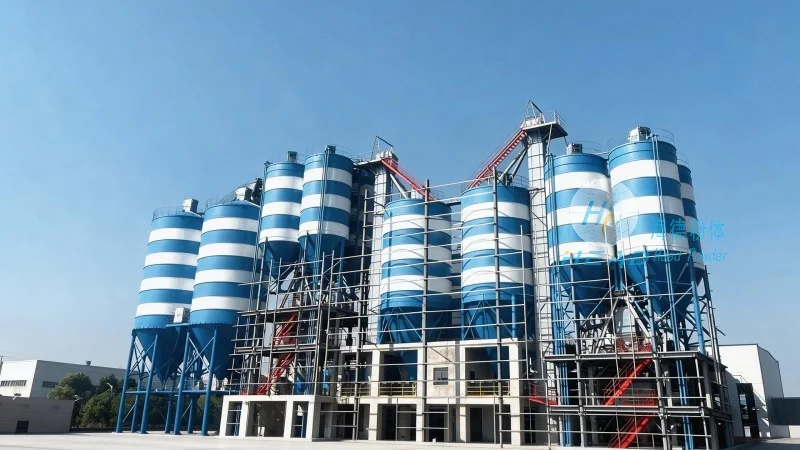
Application and Operational Benefits
These systems are widely used in power plants, cement factories, and other industrial facilities where fly ash is a byproduct. The efficient conveying of fly ash not only improves the overall productivity of the facility but also enhances safety by reducing the risk of dust explosions and material spills. By maintaining a consistent flow of material, the system ensures that downstream processes, such as cement production or waste management, operate smoothly without interruptions. Furthermore, the design of the system minimizes energy consumption, contributing to cost savings and environmental sustainability.
Company Overview: HeadPowder Engineering
As a leading manufacturer in the field, Shandong HeadPowder Engineering Co., Ltd. has been at the forefront of developing innovative solutions for powder handling systems. With a strong commitment to quality and customer satisfaction, the company has built a reputation for delivering reliable and high-performance equipment. HeadPowder's expertise lies in understanding the unique challenges of handling materials like fly ash and designing systems that meet the specific needs of each client. The company's team of engineers and technicians work closely with clients to provide customized solutions that enhance operational efficiency and reduce costs.
Conclusion
In conclusion, the fly ash silo powder conveying system equipment is a vital asset for industries dealing with fly ash. Its design, based on sound engineering principles, ensures efficient and safe material handling. By choosing a system from a reputable manufacturer like Shandong HeadPowder Engineering Co., Ltd., facilities can benefit from improved productivity, enhanced safety, and long-term cost savings. The continued development of such systems reflects the industry's focus on optimizing material handling processes and contributing to sustainable industrial practices.