

Working Principle and Features of Bulk Bag Pneumatic Conveying Systems
For industrial applications requiring efficient and reliable material handling, bulk bag pneumatic conveying lines offer a sophisticated solution. These systems are designed to transport bulk materials from storage bags to processing equipment with minimal human intervention. In this article, we will explore the working principle and key features of bulk bag pneumatic conveying systems, with a focus on the expertise of Shandong HeadPowder Engineering Co., Ltd., a prominent manufacturer based in China.
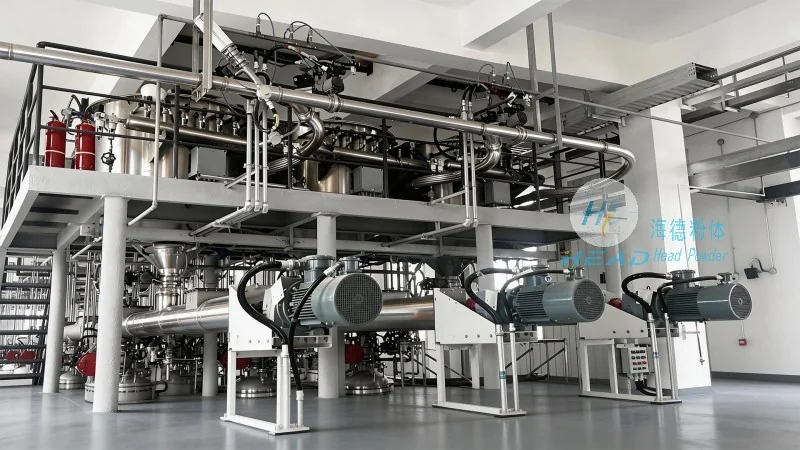
About HeadPowder: A Leading Provider of Bulk Bag Pneumatic Conveying Solutions
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a reputable company specializing in the design, manufacturing, and installation of bulk material handling equipment. With a strong presence in China, particularly in Shandong province, HeadPowder has established itself as a trusted partner for businesses seeking advanced pneumatic conveying solutions. The company’s commitment to quality and innovation ensures that their systems meet the highest industry standards, providing durability and performance for diverse industrial applications.
Working Principle of Bulk Bag Pneumatic Conveying Lines
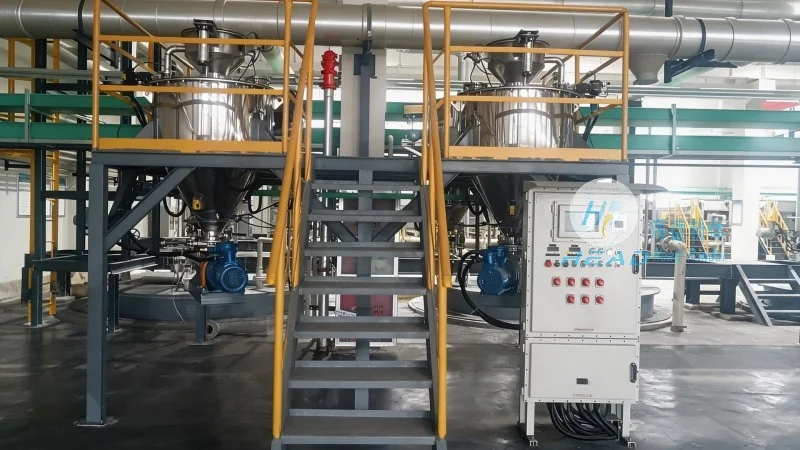
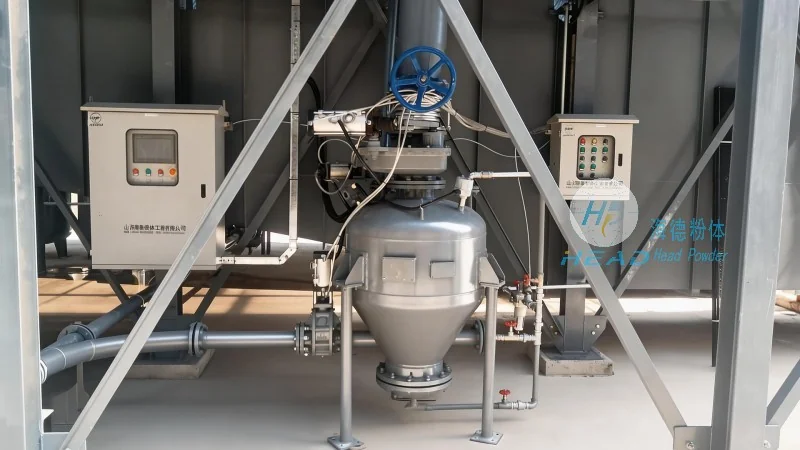
The core of a bulk bag pneumatic conveying system lies in its ability to transfer dry bulk materials through an air stream. The process typically begins with the bulk bag, which is placed on a hopper or a dedicated loading platform. The material inside the bag is then drawn into the conveying line using either positive pressure (compressed air) or negative pressure (vacuum). The system comprises several key components, including a hopper with a discharge valve, a pneumatic conveyor, and an unloading device. As the material is drawn into the system, it is carried by the air flow through the pipeline to the destination point, such as a silo, storage tank, or processing unit. The unloading device then releases the material into the receiving equipment, completing the transfer process. This method eliminates the need for manual handling and reduces the risk of material contamination or spillage.
Key Features and Advantages of Bulk Bag Pneumatic Conveying Systems
Bulk bag pneumatic conveying systems offer several advantages that make them ideal for various industrial settings. One of the primary benefits is their high efficiency in material transfer, as they can move large quantities of bulk materials quickly and with minimal downtime. The systems are also highly flexible, allowing for easy integration into existing production lines and adaptability to different material types and processing requirements. Additionally, pneumatic conveying reduces the need for manual labor, enhancing workplace safety and reducing operational costs associated with manual handling. The enclosed nature of the system also minimizes dust emissions and prevents material contamination, which is crucial for industries dealing with sensitive or hygienic products. Furthermore, these systems are designed for low maintenance, with components that are easy to access and replace, ensuring consistent performance over time. The use of compressed air as the driving force also provides a clean and energy-efficient method of material transport, contributing to a more sustainable operational environment.
Applications and Industries Served by Bulk Bag Pneumatic Conveying Systems
Bulk bag pneumatic conveying systems are widely used across various industries, including food and beverage, pharmaceuticals, chemicals, and mining. In the food industry, for example, these systems are employed to transfer ingredients like flour, sugar, and spices from bulk bags to processing equipment, ensuring hygienic and efficient handling. In the pharmaceutical sector, the enclosed and dust-free nature of the system is critical for maintaining product purity and compliance with regulatory standards. Chemical manufacturers benefit from the ability to handle abrasive or corrosive materials without damaging the conveying equipment, while mining operations use these systems to transport raw materials from storage to processing plants. The versatility of bulk bag pneumatic conveying systems makes them a preferred choice for businesses looking to streamline their material handling processes and improve overall operational efficiency.
Conclusion: Choosing the Right Bulk Bag Pneumatic Conveying System
When selecting a bulk bag pneumatic conveying system, it is essential to consider the specific requirements of your industrial application, including the type of material, volume, and operational environment. Shandong HeadPowder Engineering Co., Ltd. offers a range of customized solutions tailored to meet these needs, leveraging their expertise in material handling technology. By understanding the working principle and features of these systems, businesses can make informed decisions that enhance productivity, reduce costs, and ensure compliance with industry standards. The combination of efficiency, flexibility, and reliability makes bulk bag pneumatic conveying systems a valuable investment for any organization seeking to optimize their material handling processes.