For industrial applications that require the efficient handling of bulk powders, the silo powder conveying system is a critical component. This system is designed to store, transport, and manage dry powders with precision and reliability. Understanding its working principle and key features is essential for optimizing operational efficiency and ensuring consistent performance in various industrial settings.
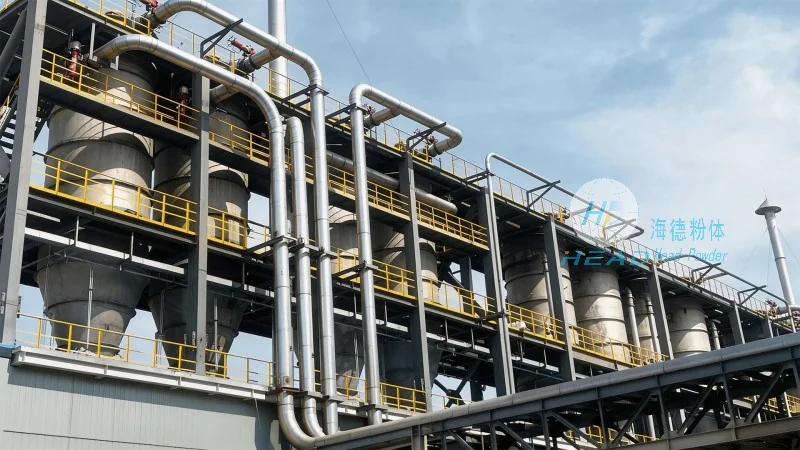
The silo powder conveying system, as offered by Shandong HeadPowder Engineering Co., Ltd., is a sophisticated piece of equipment tailored for the storage and transport of bulk materials. At its core, the system combines a silo for material storage with advanced conveying mechanisms to facilitate seamless material movement. The company, known in the industry as headpowder, specializes in engineering solutions that meet the diverse needs of powder handling processes.
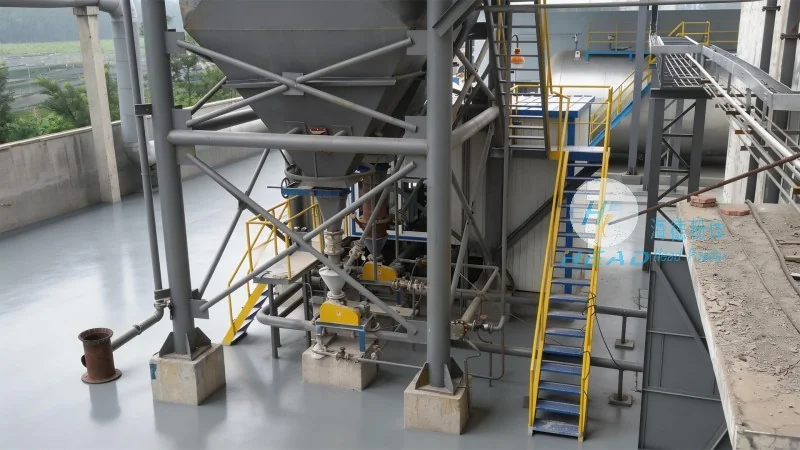
The system operates on a straightforward yet highly effective principle. Initially, bulk powders are loaded into the silo, which serves as a storage vessel. The silo is typically equipped with a hopper at the bottom, which allows for controlled discharge of the material. Once the material is in the silo, a conveying mechanism, such as a screw conveyor or pneumatic system, is activated to transport the powder from the silo to the desired destination, such as a processing unit or packaging line. The headpowder system ensures that the material flows smoothly and without blockages, thanks to its design that minimizes friction and maintains consistent pressure.
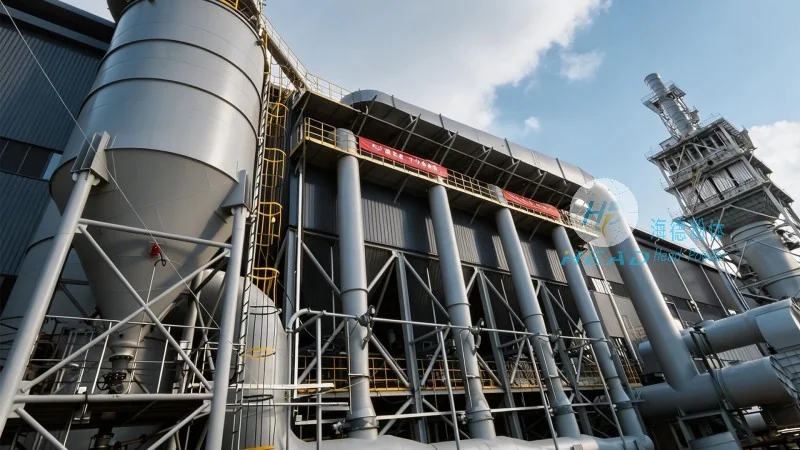
Several distinct features make the silo powder conveying system an ideal choice for industrial applications. First, the system offers high efficiency in material handling, allowing for continuous operation with minimal downtime. The design of the silo and conveying components ensures that the material is transported at a consistent rate, which is crucial for maintaining production line stability. Second, the system is highly reliable, with robust construction that can withstand the demands of heavy-duty industrial use. The materials used in the construction, such as stainless steel or corrosion-resistant alloys, enhance durability and longevity. Third, the system provides excellent control over the flow of powders, which is essential for preventing issues like clogging or uneven distribution. This control is achieved through adjustable speed settings and precise valve management, ensuring that the material is delivered as needed. Fourth, the system is designed for easy maintenance and cleaning, which helps to reduce operational costs and downtime. The modular design allows for quick access to components, making routine checks and repairs straightforward. Finally, the system is scalable, allowing it to be adapted to different production volumes and material types. This flexibility makes it suitable for a wide range of industries, including food processing, pharmaceuticals, and chemical manufacturing.
The silo powder conveying system is widely used in various industries due to its versatility and effectiveness. In the food industry, it is used to handle ingredients like flour, sugar, and spices, ensuring that they are stored and transported hygienically and efficiently. In the pharmaceutical sector, the system is employed to manage active pharmaceutical ingredients (APIs) and other powders, maintaining strict quality control and preventing contamination. In the chemical industry, it is used to transport raw materials and finished products, supporting the production of chemicals and other industrial compounds. The benefits of using this system extend beyond efficiency and reliability. It also contributes to improved safety in the workplace by reducing the need for manual handling of powders, which can be hazardous. Additionally, the system helps to minimize material waste by ensuring that the powders are transferred with minimal loss. This not only reduces costs but also supports environmental sustainability by reducing the amount of material that needs to be disposed of.
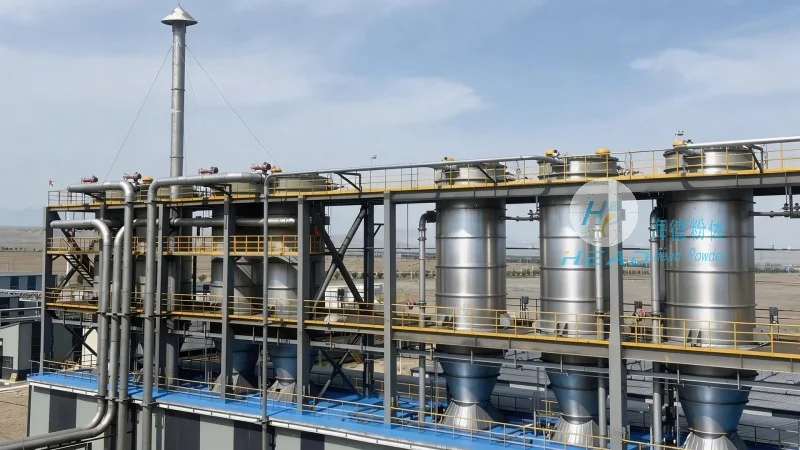
In summary, the silo powder conveying system from Shandong HeadPowder Engineering Co., Ltd. is a highly effective solution for the storage and transport of bulk powders. Its working principle, which combines a silo with advanced conveying mechanisms, ensures that materials are handled efficiently and reliably. The key features of the system, including high efficiency, robust construction, precise control, easy maintenance, and scalability, make it a valuable asset for various industrial applications. By understanding these aspects, businesses can make informed decisions about implementing this system to enhance their operational performance and achieve their production goals.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan City, Shandong Province, China

telephone
WeChatconsult
top