Welcome to Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer specializing in advanced powder handling solutions. In this article, we will explore the working principle and key features of negative pressure dilute phase powder conveyors, a technology that has revolutionized the efficient and safe transportation of powders in various industrial applications.
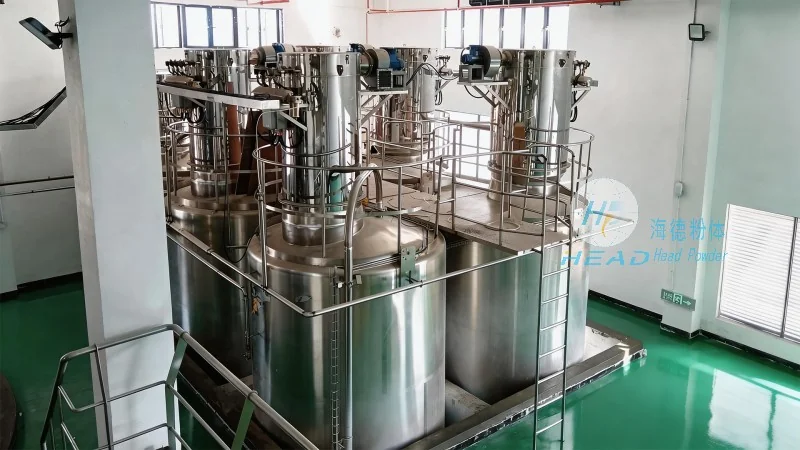
Negative pressure dilute phase powder conveyors are a type of pneumatic conveying system designed to transport dry powders and granular materials over long distances with minimal pressure drop and energy consumption. Unlike positive pressure systems that force air and material through a pipeline, negative pressure systems create a vacuum at the receiving end, drawing the material from the source to the destination. This approach offers several advantages, including reduced air leakage, lower operating costs, and improved safety in handling hazardous or sensitive powders.
The operation of a negative pressure dilute phase powder conveyor involves a series of coordinated steps to ensure efficient material transport. The process begins with the material being fed into a hopper or feeder at the source location. From there, the material is introduced into a pipeline where it is mixed with a controlled amount of air or gas. The mixture is then drawn through the pipeline by a vacuum created at the receiving end, typically using a fan or blower. The vacuum system maintains a consistent negative pressure throughout the pipeline, ensuring that the material is continuously pulled towards the destination. At the receiving end, the material is separated from the air stream through a separator or filter, and the air is either recirculated or vented, depending on the system design. This cycle repeats continuously, allowing for the steady and reliable transport of powders from the source to the destination.
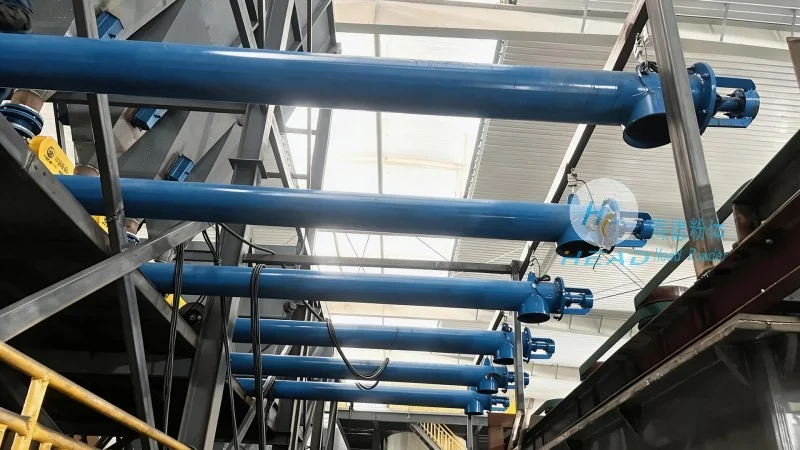
HeadPowder Engineering Co., Ltd. offers negative pressure dilute phase powder conveyors that are characterized by several key features and advantages, making them ideal for a wide range of industrial applications. One of the primary advantages is the ability to handle a variety of powder types, including fine powders, granules, and bulk materials, with minimal degradation or agglomeration. The system's low pressure drop design reduces energy consumption and operating costs, while the negative pressure environment minimizes dust emissions and improves workplace safety. Additionally, the system's compact design and flexible layout allow for easy integration into existing production lines, and the modular components enable easy maintenance and repair. The conveyors are also equipped with advanced control systems that provide real-time monitoring of material flow, pressure, and air consumption, ensuring optimal performance and reliability.
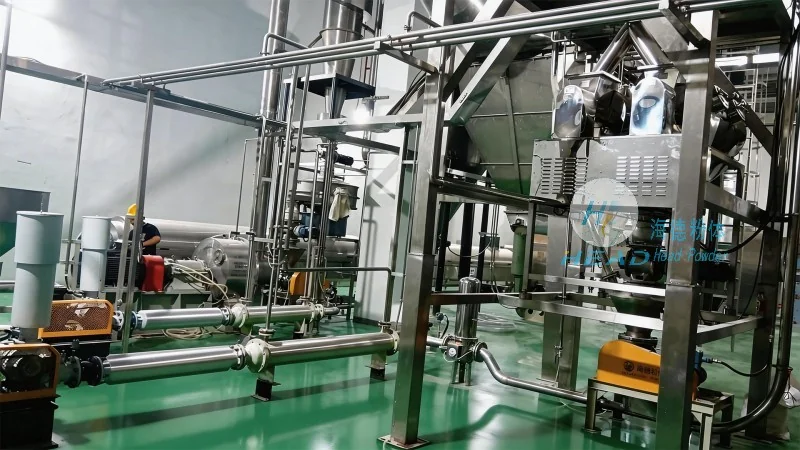
Negative pressure dilute phase powder conveyors are widely used in various industries, including pharmaceuticals, food processing, chemical manufacturing, and mining. In the pharmaceutical industry, these systems are used to transport active pharmaceutical ingredients (APIs) and excipients with high precision and minimal contamination. In food processing, they are used to handle powders such as flour, sugar, and spices, ensuring hygienic and efficient transportation. In chemical manufacturing, they are used to transport bulk chemicals and reagents, reducing the risk of exposure and improving safety. In mining, they are used to transport raw materials such as coal, ore, and minerals, improving the efficiency of material handling and reducing labor costs.
At Shandong HeadPowder Engineering Co., Ltd., we are committed to providing high-quality negative pressure dilute phase powder conveyors that meet the diverse needs of our clients. Our team of experts is dedicated to developing innovative solutions that enhance productivity, improve safety, and reduce operating costs. With years of experience in the industry, we have established ourselves as a trusted partner for companies seeking reliable and efficient powder handling solutions. Whether you are in the pharmaceutical, food, chemical, or mining industry, our negative pressure dilute phase powder conveyors are designed to meet your specific requirements and help you achieve your production goals.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan City, Shandong Province, China

telephone
WeChatconsult
top