For industrial applications that require the efficient and reliable transport of bulk fertilizer powders, specialized equipment is essential. This article provides an overview of the working principle and key features of fertilizer powder conveying systems, highlighting how they enhance operational efficiency and safety in material handling processes.
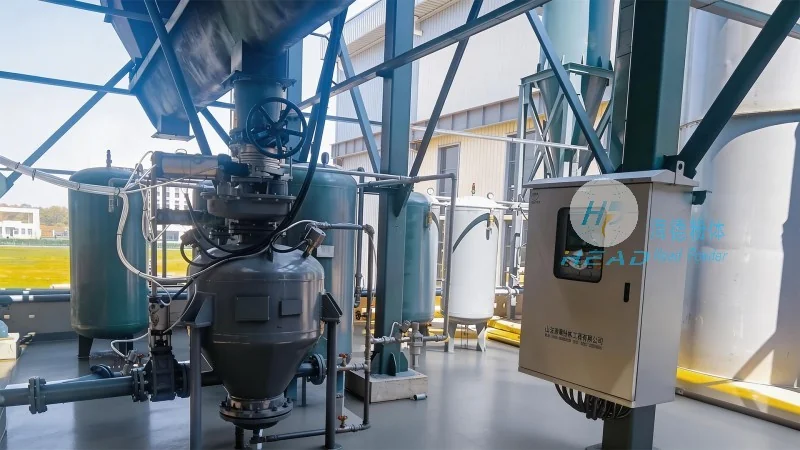
At Shandong HeadPowder Engineering Co., Ltd., we specialize in the design and manufacturing of advanced fertilizer powder conveying systems tailored to meet the diverse needs of agricultural and industrial sectors. Our equipment is engineered to handle the unique challenges associated with transporting fine, dry powders, ensuring minimal dust generation, and maintaining product integrity throughout the process.
The core of a fertilizer powder conveying system involves a combination of mechanical components that work in tandem to move material from a source to a destination. Typically, these systems utilize positive displacement or pneumatic conveying methods, depending on the specific characteristics of the fertilizer and the distance it needs to be transported.
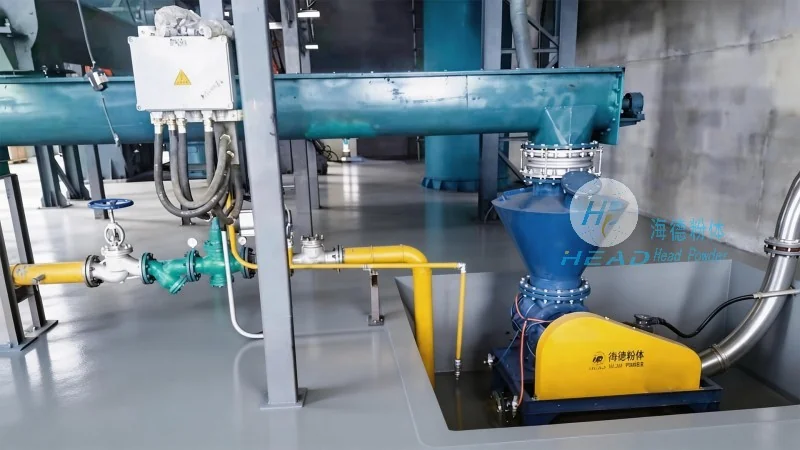
Positive displacement systems, such as rotary lobe blowers or rotary valves, use a rotating mechanism to create a vacuum or pressure that draws or pushes the powder through a pipeline. This method is particularly effective for high-density or abrasive powders, as it provides consistent flow rates and reduces the risk of clogging. In contrast, pneumatic conveying systems rely on compressed air to transport the material, which is ideal for lighter, more delicate powders that require gentle handling.
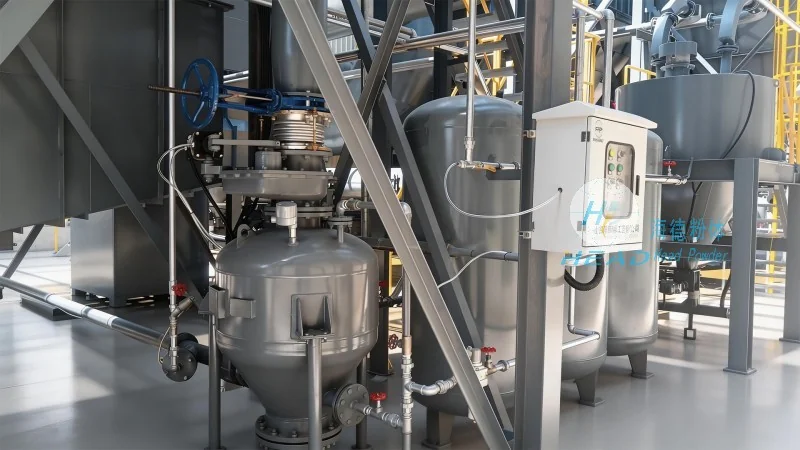
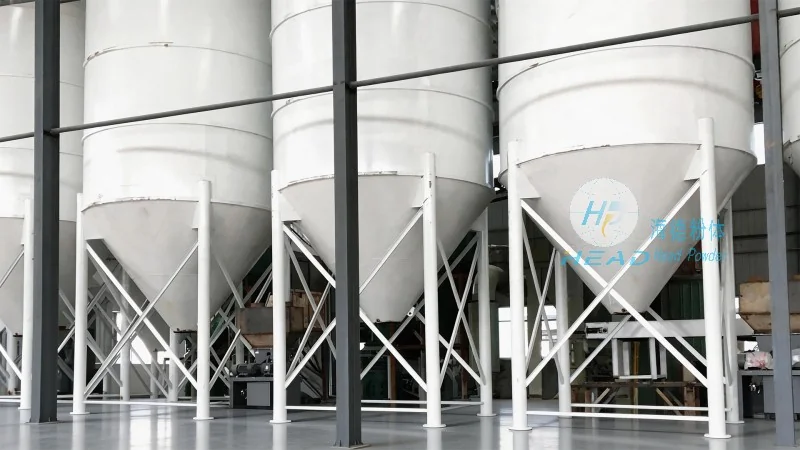
Regardless of the specific technology used, the system generally includes a hopper for material storage, a feeding mechanism to control the flow rate, a conveying line, and a discharge unit. The hopper is designed to minimize material bridging and ensure a steady supply of powder. The feeding mechanism, often a rotary valve or a screw feeder, regulates the amount of material entering the conveying line, preventing overloading and maintaining consistent performance. The conveying line itself is typically made of stainless steel or other corrosion-resistant materials to withstand the chemical properties of fertilizers and prevent contamination. The discharge unit then delivers the material to the target location, such as a storage silo or a processing unit.
Modern fertilizer powder conveying systems from HeadPowder are equipped with several advanced features that enhance their performance and reliability. One of the most notable features is the integration of dust suppression technology, which minimizes airborne particles and improves workplace safety. This is achieved through enclosed systems and efficient filtration, ensuring compliance with environmental regulations and reducing the risk of respiratory issues for operators.
Another critical feature is the ability to handle a wide range of fertilizer types, from nitrogen-based to phosphorus-based products, without compromising system performance. The adjustable speed and pressure controls allow operators to optimize the conveying process for different powder densities and flow rates, ensuring efficient operation even with varying material characteristics.
Furthermore, our systems incorporate robust material handling capabilities, including anti-clogging mechanisms and self-cleaning features. These features help prevent blockages in the conveying line, which can lead to system downtime and product loss. By using materials like stainless steel and high-quality seals, our equipment is designed to withstand the abrasive nature of fertilizers and maintain long-term durability.
Energy efficiency is also a key consideration in our design. By optimizing the conveying process and using energy-saving components, such as variable frequency drives (VFDs), we reduce operational costs while maintaining high performance. This not only benefits the end-user financially but also aligns with sustainability goals in the agricultural and industrial sectors.
Investing in a high-quality fertilizer powder conveying system from Shandong HeadPowder Engineering Co., Ltd. offers numerous benefits for businesses in the fertilizer industry. The primary advantage is improved operational efficiency, as these systems can handle large volumes of material with minimal downtime. By reducing the need for manual handling and manual loading, they also enhance workplace safety and reduce labor costs.
Another significant benefit is the preservation of product quality. Our systems are designed to minimize exposure to air and moisture, which can degrade the nutritional value of fertilizers. The enclosed design and gentle handling mechanisms ensure that the powder remains in optimal condition until it reaches its final destination, reducing waste and improving overall product performance.
Additionally, the durability and reliability of our equipment contribute to long-term cost savings. With proper maintenance and regular inspections, our systems can operate for extended periods without major repairs, reducing the total cost of ownership. This makes them a cost-effective solution for businesses looking to enhance their material handling capabilities.
In conclusion, fertilizer powder conveying systems are essential for efficient and safe material handling in the agricultural and industrial sectors. The working principle, which combines mechanical and pneumatic technologies, ensures consistent and reliable transport of bulk powders. Key features such as dust suppression, adjustable controls, and anti-clogging mechanisms enhance performance and safety. By choosing a system from Shandong HeadPowder Engineering Co., Ltd., businesses can benefit from improved efficiency, product quality, and cost savings, making it a valuable investment for their operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan City, Shandong Province, China

telephone
WeChatconsult
top