Shandong HeadPowder Engineering Co., Ltd. is a professional manufacturer specializing in the design, development, and production of advanced powder conveying systems. With a focus on precision and efficiency, our company is dedicated to providing high-quality solutions for the handling and transportation of various powders, including magnesium sulfate. HeadPowder has established itself as a trusted partner in the industry, delivering reliable equipment that meets the stringent requirements of modern industrial applications.
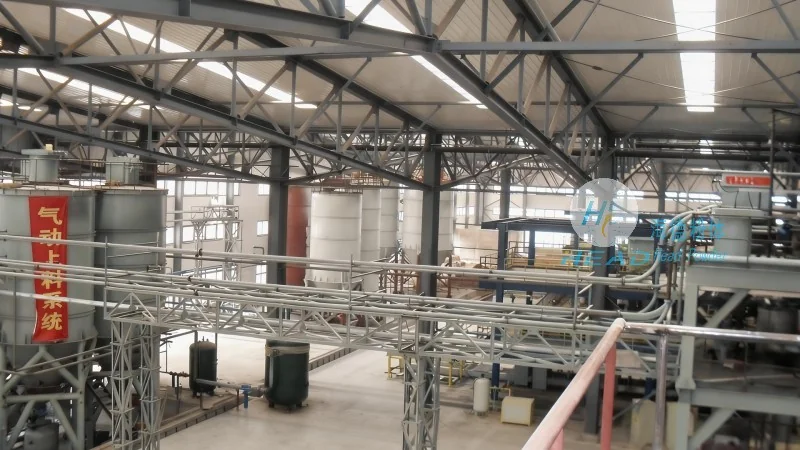
The magnesium sulfate powder conveying system operates on a principle of pneumatic or mechanical transport, depending on the specific design and application requirements. Typically, the system uses a combination of air pressure and mechanical components to move the powder from the source to the destination. The process begins with the powder being fed into a hopper or feeder, where it is then transferred to a conveyor or pneumatic duct. The conveying medium, often compressed air, creates a flow that propels the powder through the system. This method ensures a consistent and controlled movement of the powder, minimizing the risk of clogging or material degradation. The system is equipped with sensors and controls that monitor the flow rate and pressure, allowing for real-time adjustments to maintain optimal performance. Additionally, the design incorporates features such as dust collection and filtration to ensure a clean and safe operation environment. The working principle is engineered to handle the unique properties of magnesium sulfate, such as its fine particle size and hygroscopic nature, ensuring that the powder is conveyed without agglomeration or loss of quality.
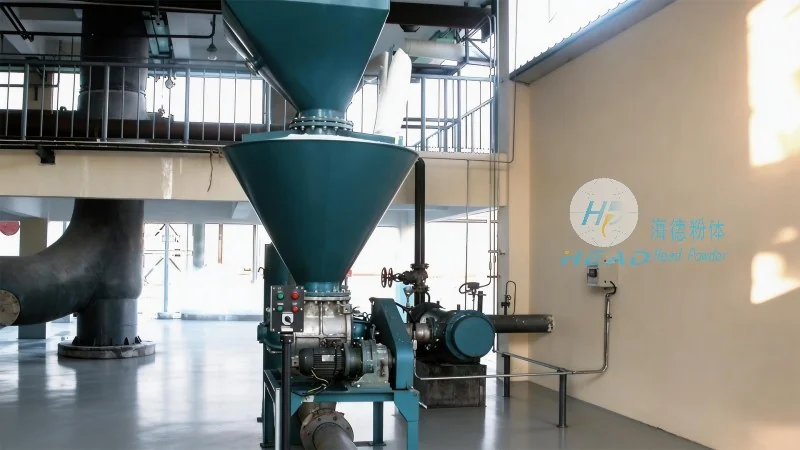
HeadPowder's magnesium sulfate powder conveying system is characterized by several key features that enhance its performance and reliability. One of the primary features is the robust construction, which is designed to withstand the abrasive and corrosive properties of magnesium sulfate. The system utilizes high-quality materials, such as stainless steel and special alloys, to prevent corrosion and ensure long-term durability. Another important feature is the adjustable speed and flow control, which allows operators to customize the conveying rate based on the specific needs of the application. This flexibility is crucial for maintaining product quality and preventing over-processing. The system also includes advanced safety features, such as emergency shut-off valves and pressure relief mechanisms, to protect both the equipment and personnel. Additionally, the design incorporates easy maintenance components, such as quick-release connections and accessible service points, reducing downtime and maintenance costs. The integration of dust suppression technology is another notable feature, as it helps to minimize airborne dust and improve workplace safety. Furthermore, the system is equipped with monitoring and diagnostic tools that provide real-time data on performance, enabling proactive maintenance and troubleshooting. These features collectively contribute to the system's efficiency, safety, and longevity, making it an ideal solution for industrial applications.
The magnesium sulfate powder conveying system is widely used in various industries, including chemical manufacturing, pharmaceuticals, and food processing. Its primary benefit is the ability to handle fine powders like magnesium sulfate efficiently and safely. The system's design minimizes material loss and ensures consistent product quality, which is critical in industries where purity and uniformity are paramount. Additionally, the system reduces labor costs by automating the powder handling process, allowing for higher throughput and productivity. The compact and modular design of the system makes it suitable for both new installations and retrofitting into existing facilities. The system's energy efficiency is another advantage, as it uses less power compared to traditional methods of powder transport. Furthermore, the system's low maintenance requirements contribute to long-term cost savings. The ability to handle hygroscopic materials like magnesium sulfate without moisture absorption or degradation is a significant advantage, as it maintains the material's properties throughout the conveying process. Overall, the magnesium sulfate powder conveying system offers a reliable and efficient solution for the transportation of this essential chemical, supporting the operational needs of various industrial sectors.
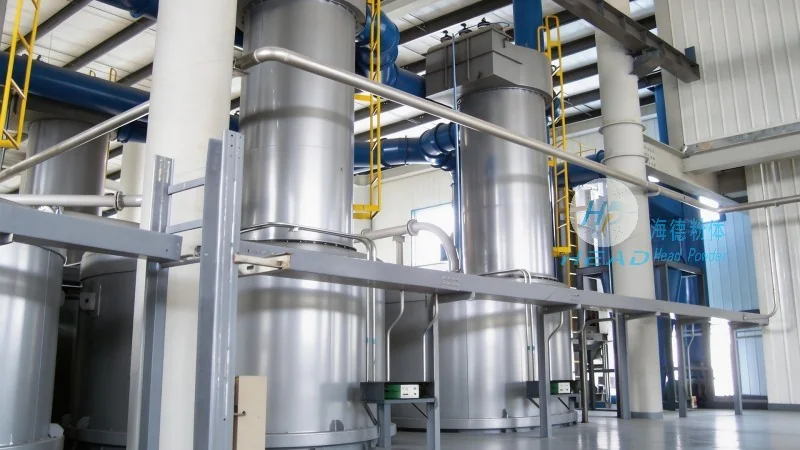
Shandong HeadPowder Engineering Co., Ltd. provides a comprehensive magnesium sulfate powder conveying system that combines advanced technology with robust engineering. The system's working principle, based on pneumatic or mechanical transport, ensures efficient and controlled movement of the powder. Key features such as durable construction, adjustable flow control, and safety mechanisms enhance its performance and reliability. The system is designed to meet the specific requirements of industrial applications, offering benefits like improved product quality, reduced labor costs, and energy efficiency. With its focus on precision and efficiency, HeadPowder's system is a trusted solution for handling magnesium sulfate and other fine powders, supporting the operational needs of various industries. The company's commitment to quality and customer satisfaction ensures that clients receive a reliable and long-lasting product that meets their specific needs.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan City, Shandong Province, China

telephone
WeChatconsult
top