

Common Compound Fertilizer Conveying Methods: Advantages and Features of HeadPowder's Pneumatic Conveying Systems
Compound fertilizers are a cornerstone of modern agriculture, providing essential nutrients to crops and enhancing overall productivity. The efficient and reliable transportation of these materials from production sites to storage facilities or application points is critical for maintaining supply chain integrity and operational efficiency. As the demand for high-quality fertilizers grows, so does the need for advanced conveying technologies that can handle the unique challenges associated with compound fertilizers, such as bulk density, particle size variation, and moisture content. This article explores common compound fertilizer conveying methods and highlights the advantages of HeadPowder's pneumatic conveying systems, a leading solution in the industry.
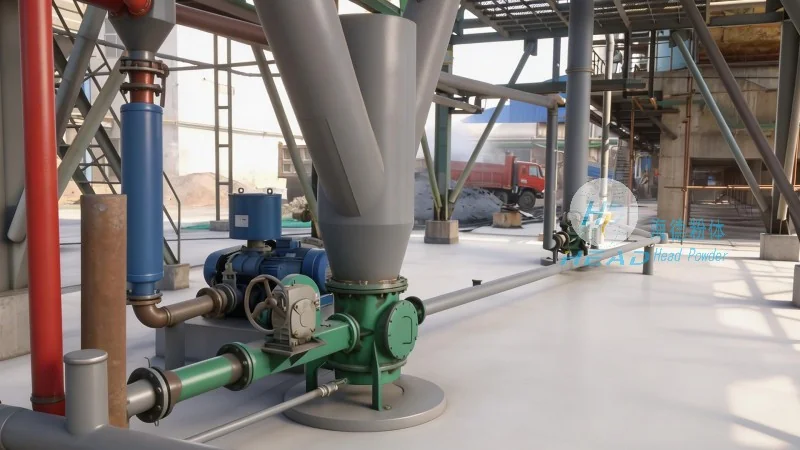
Conventional methods for transporting compound fertilizers include belt conveyors, screw conveyors, and bucket elevators. Belt conveyors are widely used for horizontal and slight incline transport, offering high capacity and durability. However, they may struggle with material buildup or spillage, especially with fine or powdery fertilizers. Screw conveyors are effective for vertical or inclined transport but can cause excessive friction and heat generation, potentially degrading the fertilizer's quality. Bucket elevators are suitable for vertical lifting but require regular maintenance to prevent mechanical failures. While these methods have been in use for decades, they often face limitations in handling the diverse characteristics of modern compound fertilizers, leading to operational inefficiencies and increased maintenance costs.
Pneumatic conveying, or air-based transport, has emerged as a preferred solution for compound fertilizer handling due to its flexibility, efficiency, and ability to handle a wide range of material properties. Unlike mechanical systems, pneumatic conveyors use compressed air to move materials through a pipeline system, eliminating the need for moving parts in contact with the product. This design reduces wear and tear, minimizes product contamination, and allows for seamless integration with storage and processing equipment. HeadPowder, a renowned manufacturer of pneumatic conveying systems, specializes in custom solutions tailored to the specific needs of fertilizer producers, ensuring optimal performance and reliability.
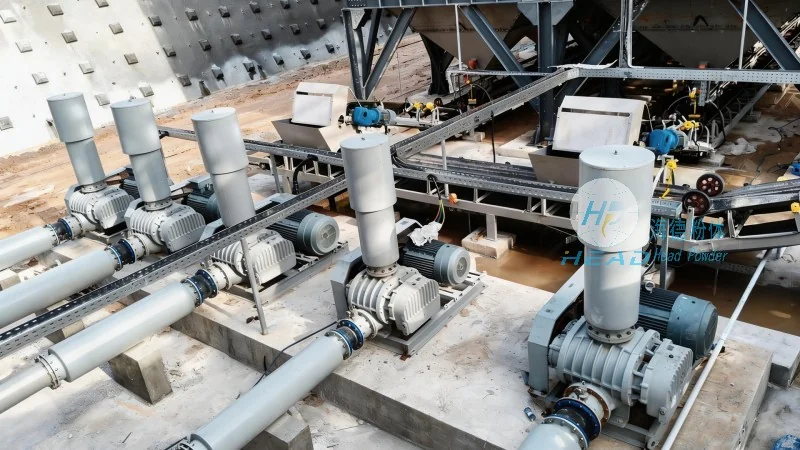
HeadPowder's pneumatic conveying systems offer several key advantages that set them apart from traditional methods. First, the technology provides high conveying rates with minimal energy consumption, making it cost-effective for large-scale operations. The systems are designed to handle various compound fertilizers, including granular, powdered, and liquid-based formulations, without compromising product quality. This versatility is particularly valuable for manufacturers producing multiple fertilizer types or those dealing with fluctuating raw material compositions. Additionally, pneumatic conveyors can be easily scaled to accommodate growing production volumes, allowing for future expansion without significant infrastructure changes.
From a technical perspective, HeadPowder's systems incorporate advanced features that enhance efficiency and safety. The use of positive or negative pressure systems allows for precise control over material flow, ensuring consistent delivery to storage silos or packaging lines. The pipeline design minimizes pressure drops and reduces the risk of material blockages, which are common issues in mechanical conveyors. HeadPowder also employs high-quality materials, such as stainless steel and corrosion-resistant alloys, to prevent contamination and extend the lifespan of the equipment. These technical innovations contribute to lower maintenance costs and longer operational lifespans, making the systems a long-term investment for fertilizer companies.
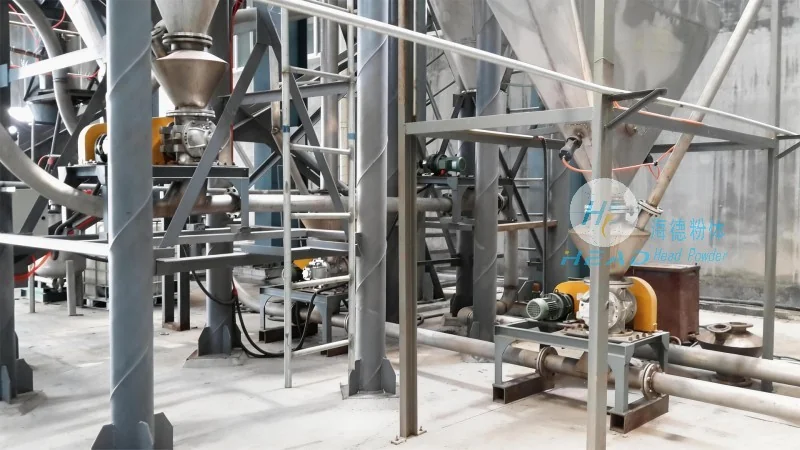
HeadPowder's pneumatic conveying solutions are applied in diverse scenarios across the fertilizer industry. For example, in large-scale production facilities, the systems are used to transport raw materials from storage silos to mixing and granulation units, ensuring a continuous and uninterrupted supply chain. In storage and distribution centers, pneumatic conveyors efficiently move finished products to loading docks or trucks, reducing labor costs and speeding up delivery times. The technology is also utilized in small-scale or remote operations, where traditional mechanical systems may be impractical due to space constraints or terrain challenges. By adapting to different operational environments, HeadPowder's solutions provide flexibility and reliability for businesses of all sizes.
When considering the implementation of a compound fertilizer conveying system, companies must evaluate factors such as material characteristics, production capacity, and operational requirements. HeadPowder's expertise in pneumatic conveying allows them to provide tailored solutions that address these specific needs. The company's team of engineers works closely with clients to assess their current infrastructure, identify bottlenecks, and design a system that maximizes efficiency while minimizing downtime. This collaborative approach ensures that the final solution not only meets current demands but also supports future growth and expansion. By choosing HeadPowder's pneumatic conveying systems, fertilizer producers can enhance their operational performance, reduce costs, and maintain the high quality of their products, ultimately contributing to the success of their business.