

Working Principle and Features of Pneumatic Conveying Equipment for Wood Dust Materials
HeadPowder, a leading provider in the field, specializes in pneumatic conveying solutions tailored for wood dust materials. This equipment is designed to efficiently transport fine wood dust particles from one location to another, ensuring a reliable and effective material handling process. The following sections will delve into the working principle and key features of such systems, providing a comprehensive understanding of their functionality and benefits.
Working Principle of Pneumatic Conveying Equipment
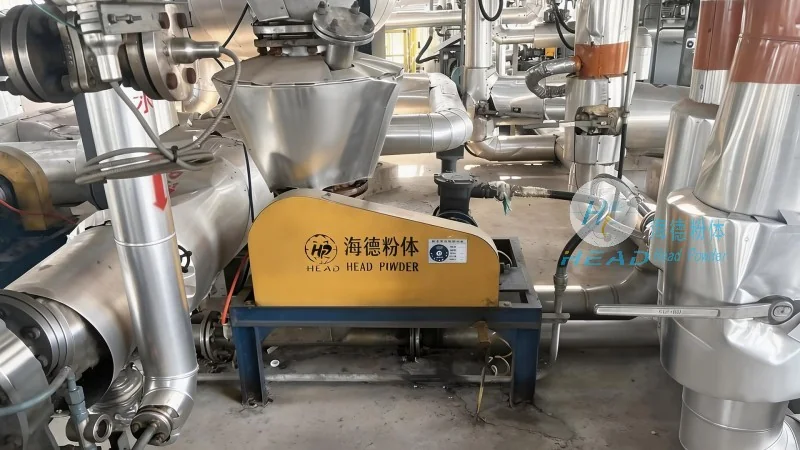
The core mechanism of pneumatic conveying equipment for wood dust involves the use of air to move material through a pipeline system. The process typically operates under either positive or negative pressure, depending on the specific application requirements. In positive pressure systems, compressed air is introduced into the material feed point, creating a pressure differential that propels the wood dust particles forward. Conversely, negative pressure systems draw the material into the system using vacuum, which is particularly useful for applications where dust control and containment are critical. The equipment comprises several key components, including a material feeder, a conveying line, a separator, and a receiver. The material feeder ensures a consistent flow of wood dust into the system, while the conveying line transports the particles through the pipeline. The separator then separates the conveyed material from the air stream, and the receiver collects the final product. This integrated approach ensures efficient material transport with minimal loss and contamination.
Key Features of Pneumatic Conveying Equipment for Wood Dust Materials
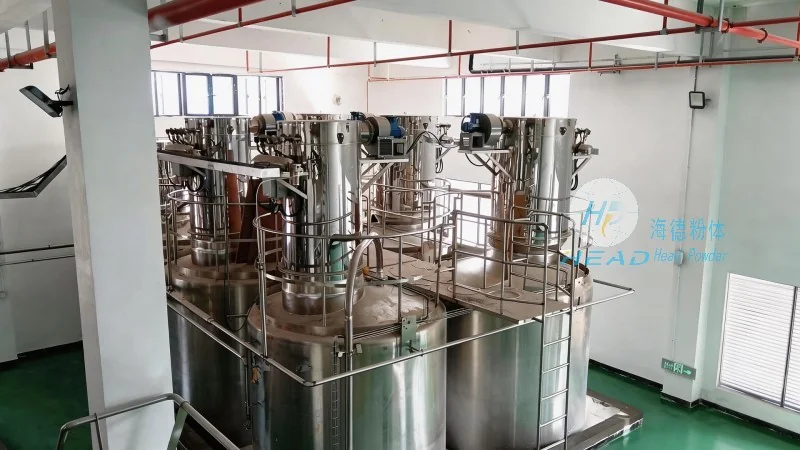
Several notable features distinguish the pneumatic conveying equipment used for wood dust materials. Firstly, the system offers high efficiency in material transport, capable of handling large volumes of fine particles with minimal energy consumption. This efficiency is achieved through optimized air flow and pipeline design, which reduces pressure drop and energy waste. Secondly, the equipment provides excellent dust control and containment, which is crucial for maintaining a safe and clean working environment. The sealed pipeline system prevents dust from escaping into the atmosphere, reducing the risk of respiratory issues and environmental contamination. Thirdly, the equipment is designed for easy maintenance and operation, with user-friendly controls and accessible components that simplify routine checks and repairs. This reduces downtime and operational costs, making it a cost-effective solution for industrial applications. Additionally, the system offers flexibility in terms of layout and integration, allowing it to be adapted to various production setups and space constraints. This adaptability ensures that the equipment can be seamlessly incorporated into existing workflows without significant modifications.
Company Information and Location
HeadPowder, the manufacturer of this advanced pneumatic conveying equipment, is based in Shandong, China. The company, known for its expertise in engineering and manufacturing, has established itself as a trusted provider of material handling solutions. With a focus on quality and innovation, HeadPowder ensures that its products meet the highest standards of performance and reliability. The company’s location in Shandong provides easy access to key markets and supply chains, facilitating efficient production and distribution. This strategic positioning enables HeadPowder to deliver high-quality equipment to customers worldwide, supporting their operational needs and growth objectives.