

Principle and Working Scene Characteristics of Bin Pump Powder Material Handling
Bin pump technology is a critical component in modern powder handling systems, offering efficient and reliable methods for transporting bulk materials. This article explores the fundamental principles behind bin pump powder transport and highlights the key characteristics of its working scenes, providing insights into how this technology enhances operational efficiency in various industrial settings.
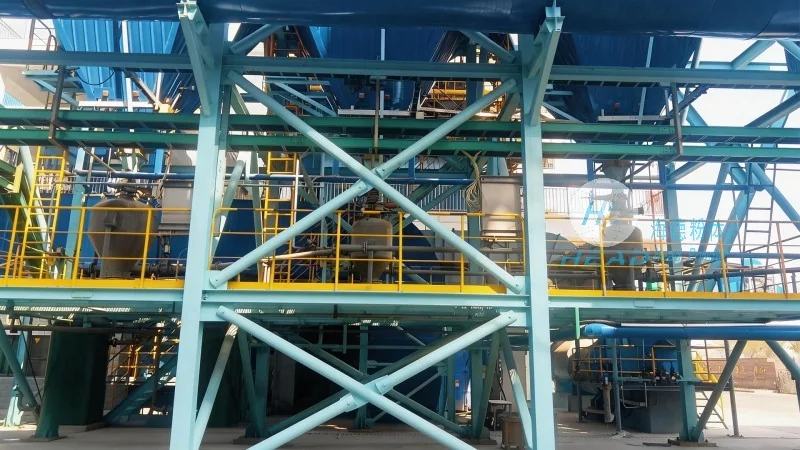
Introduction to Bin Pump Powder Handling Technology
Bin pumps, also known as pressure-type or pneumatic pumps, are specialized equipment designed to transport dry bulk materials such as powders, granules, and fine particles. Unlike traditional conveyor systems, bin pumps operate by creating a pressure differential to move material from a storage bin or hopper to the destination point. This method is particularly effective for materials that are difficult to handle with conventional methods, such as those with high moisture content, abrasive properties, or those prone to caking. The technology is widely adopted across industries including pharmaceuticals, chemicals, food processing, and mining, where precise and controlled material transport is essential.
About HeadPowder: A Leading Provider in Powder Handling Solutions
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a reputable company based in Shandong, China, dedicated to developing and manufacturing advanced powder handling equipment. With a strong focus on innovation and customer satisfaction, HeadPowder has established itself as a trusted partner for businesses seeking reliable solutions for their material transport needs. The company's expertise lies in designing customized bin pump systems that meet the specific requirements of various industries, ensuring optimal performance and durability. By leveraging years of experience and technical expertise, HeadPowder delivers high-quality products that enhance operational efficiency and reduce downtime for its clients.
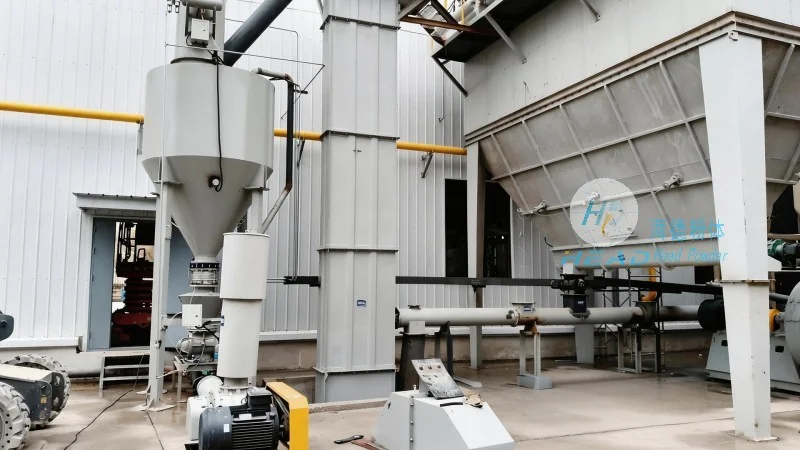
The Working Principle of Bin Pump Powder Transport
The core principle of bin pump powder transport involves the use of compressed air or other gases to create a pressure difference between the storage bin and the discharge point. The process typically begins with the material being fed into the bin pump from a hopper or silo. As the material accumulates, the pump's internal chamber is pressurized by the introduced gas, which forces the material to move through a pipeline to the target location. The pressure is carefully controlled to ensure the material flows smoothly without causing blockages or excessive wear on the equipment. Key components of a bin pump system include the hopper, the pump body, the pressure vessel, and the discharge valve, each playing a crucial role in the overall operation. The system is designed to handle a wide range of materials, from fine powders to larger granules, with adjustable settings to accommodate different material properties and flow rates.
Key Characteristics of Working Scenes for Bin Pump Applications
The working scenes where bin pump technology is applied vary significantly based on the industry and the specific material being handled. In pharmaceutical manufacturing, for example, bin pumps are used to transport active pharmaceutical ingredients (APIs) and excipients with strict purity requirements, ensuring that the material remains uncontaminated during transport. The controlled environment and precise pressure management in these settings are critical to maintaining product quality. In the chemical industry, bin pumps are employed to handle abrasive and corrosive materials, such as cement and chemicals, where traditional conveyors may cause wear and tear or contamination. The ability of bin pumps to handle these challenging materials without damage makes them an ideal choice for such applications. Additionally, in food processing facilities, bin pumps are used to transport ingredients like flour, sugar, and spices, where hygiene and safety are paramount. The sealed design of the system prevents contamination and ensures that the materials remain in compliance with food safety regulations. In mining operations, bin pumps are utilized to transport ore and other minerals from storage bins to processing plants, improving the efficiency of material handling and reducing the risk of material loss or spillage.
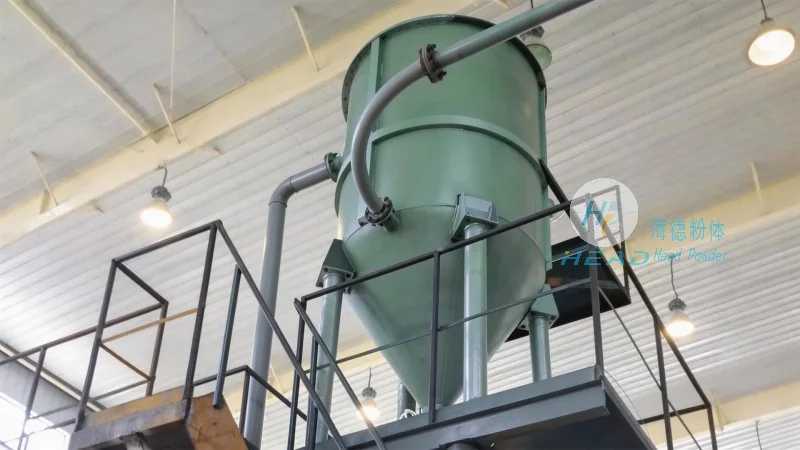
Advantages in Practical Applications
Bin pump technology offers several advantages over traditional material handling methods, making it a preferred choice for many industries. One of the primary benefits is its ability to handle a wide range of materials, including those that are difficult to transport with conventional systems. The controlled pressure and flow rates allow for precise material delivery, reducing waste and improving product quality. Another advantage is the reduced risk of material degradation or contamination, as the system is designed to maintain a clean and sealed environment. This is particularly important in industries where product purity is critical, such as pharmaceuticals and food processing. Additionally, bin pumps are more energy-efficient compared to other methods, as they use compressed air rather than mechanical power to move the material. This results in lower operational costs and a smaller environmental footprint. The flexibility of bin pump systems also allows for easy integration with existing infrastructure, making them a cost-effective solution for businesses looking to upgrade their material handling capabilities. Furthermore, the compact design of bin pumps makes them suitable for applications with limited space, such as in urban or industrial settings where floor space is at a premium.
Conclusion
Bin pump powder transport technology is a sophisticated and effective solution for handling bulk materials in various industrial applications. By understanding the fundamental principles and characteristics of this technology, businesses can make informed decisions about implementing bin pump systems to enhance their operational efficiency and product quality. With the expertise of companies like Shandong HeadPowder Engineering Co., Ltd., businesses can access reliable and customized solutions that meet their specific needs. As the demand for efficient material handling continues to grow, bin pump technology will remain a vital component in the modern industrial landscape, driving innovation and improving productivity across industries.