

Operation Process and Working Principle of Sodium Chlorate Powder Conveying System Equipment
The sodium chlorate powder conveying system is a specialized industrial equipment designed to handle the transportation of sodium chlorate, a critical chemical used in various industrial applications such as pulp and paper production, chemical synthesis, and water treatment. This system ensures efficient and safe material handling, minimizing dust generation and optimizing operational efficiency. The design incorporates advanced engineering principles to meet the stringent requirements of handling sodium chlorate, which is known for its reactivity and potential hazards if not managed properly.
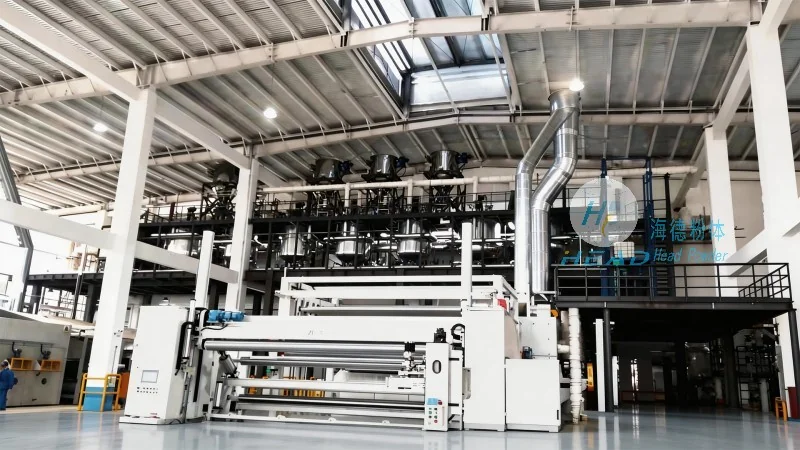
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, the manufacturer of this advanced conveying system, is a leading company in the field of powder handling technology. Based in Shandong, China, HeadPowder has established itself as a trusted provider of high-quality industrial solutions tailored to the needs of the chemical and material processing industries. The company specializes in the design, development, and manufacturing of equipment for handling hazardous and sensitive powders, leveraging years of experience and technical expertise to deliver reliable and efficient systems.
Key Components and Their Functions in the Conveying System
The sodium chlorate powder conveying system consists of several key components, each playing a crucial role in the overall operation. The primary components include:
• Hopper and Feeder: The hopper is used to store the sodium chlorate powder, while the feeder regulates the flow of material into the conveyor. This component ensures a consistent and controlled feed rate, preventing overloading or underfeeding.
• Conveyor Belt or Screw Conveyor: Depending on the system design, a conveyor belt or screw conveyor is used to transport the powder from the hopper to the discharge point. The conveyor is equipped with appropriate sealing and dust control mechanisms to maintain a safe and clean environment.
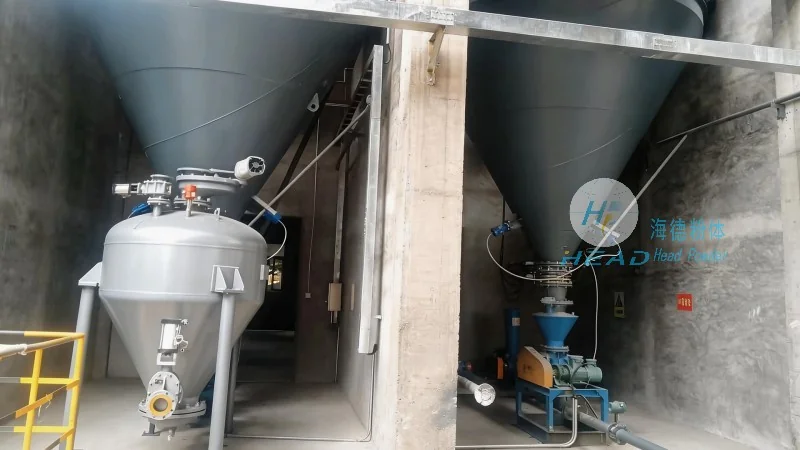
• Dust Collection System: An integrated dust collection system is essential to capture any airborne particles, ensuring compliance with environmental regulations and maintaining a safe working environment.
• Control Panel and Sensors: The control panel allows operators to monitor and control the system's operation, while sensors provide real-time feedback on material levels, flow rates, and system performance.
Detailed Operation Process of the System
The operation of the sodium chlorate powder conveying system follows a systematic process to ensure efficient and safe material handling. The process begins with the loading of sodium chlorate into the hopper. The feeder then regulates the flow of material, which is transferred to the conveyor. The conveyor transports the powder to the discharge point, where it is collected in a designated container or processing unit. Throughout the process, the dust collection system continuously captures any airborne particles, preventing dust accumulation and maintaining a clean environment.
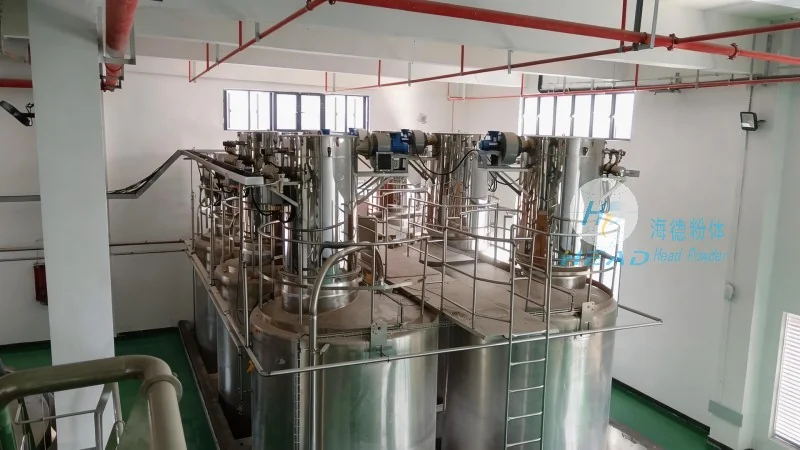
Working Principle Explained
The working principle of the sodium chlorate powder conveying system is based on mechanical transport mechanisms. The system utilizes gravity and mechanical force to move the powder from the hopper to the discharge point. The feeder controls the flow rate, ensuring a consistent supply of material to the conveyor. The conveyor then transports the powder through a sealed and enclosed system, minimizing dust generation and exposure to the environment. The control panel and sensors provide real-time monitoring, allowing operators to adjust the system parameters as needed to maintain optimal performance.
Technical Specifications and Performance Characteristics
The sodium chlorate powder conveying system is engineered to meet the specific requirements of handling sodium chlorate. Key technical specifications include:
• Capacity: The system is designed to handle capacities ranging from low to high, depending on the application requirements.
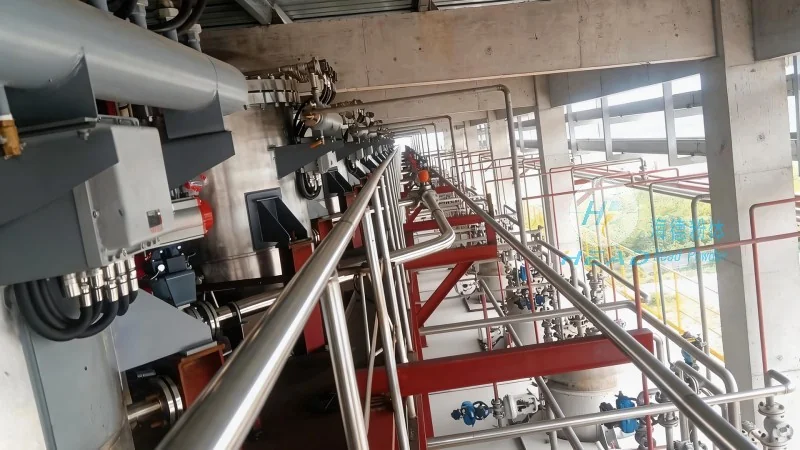
• Material Handling: The system is capable of handling sodium chlorate powder with specific characteristics such as particle size, moisture content, and reactivity.
• Dust Control: The integrated dust collection system ensures that dust levels are maintained within safe limits, complying with environmental regulations.
• Safety Features: The system incorporates safety features such as emergency stop buttons, overload protection, and material leakage detection to ensure safe operation.
Application Scenarios and Industry Relevance
The sodium chlorate powder conveying system is widely used in various industrial applications where sodium chlorate is a key component. In the pulp and paper industry, it is used as a bleaching agent, while in chemical synthesis, it serves as a precursor for other chemical products. The system's ability to handle sodium chlorate safely and efficiently makes it an essential part of many industrial processes. By ensuring consistent and reliable material handling, the system contributes to improved productivity and reduced operational costs.