

Introduction to the Rice Pneumatic Conveyor: Structure and Working Principle
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying systems. The rice pneumatic conveyor is a key equipment in the grain processing industry, engineered to efficiently transport rice and other similar bulk materials with precision and reliability. This article provides a comprehensive overview of the rice pneumatic conveyor, focusing on its structural components and operational principles.
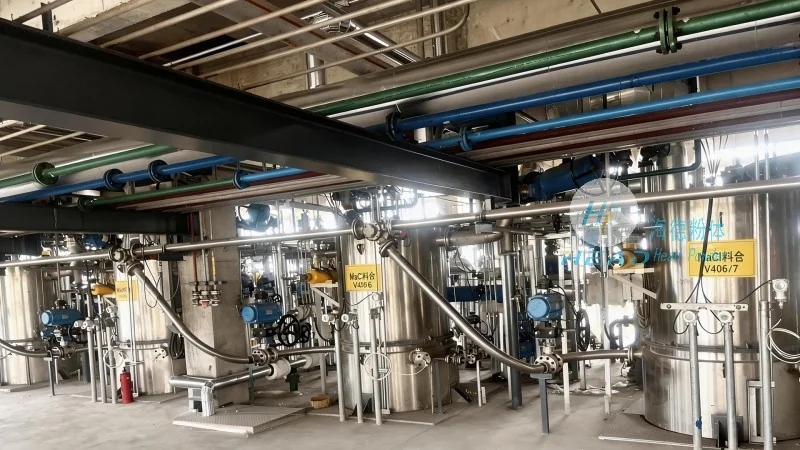
The rice pneumatic conveyor operates on the principle of air flow to move materials. It consists of several core components that work in tandem to ensure smooth and efficient material handling. The main parts include the hopper, which serves as the material storage and feeding unit; the conveying pipe, which transports the material through the system; the air compressor or blower, which generates the necessary air pressure; and the control system, which regulates the flow of air and material. Each component plays a critical role in the overall functionality of the conveyor.
The hopper is typically made of durable materials such as stainless steel or high-grade plastic, designed to withstand the weight and abrasion of bulk rice. It features a feeding port at the top for material input and a discharge outlet at the bottom connected to the conveying pipe. The design of the hopper ensures uniform material flow, preventing blockages and ensuring consistent feeding rates. The conveying pipe is usually made of corrosion-resistant materials like PVC or metal, with smooth inner surfaces to minimize friction and material degradation. The pipe is arranged in a series of bends and straight sections, optimized to maintain the air flow velocity required for effective material transport.
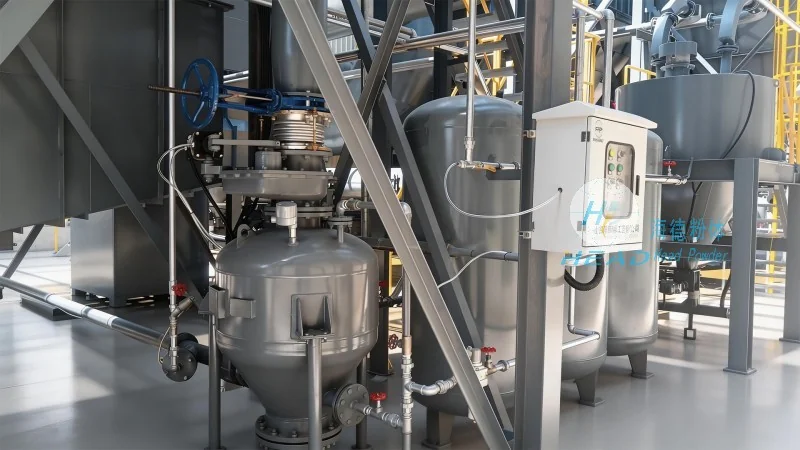
The air compressor or blower is the power source of the pneumatic conveyor. It generates a high-pressure air stream that propels the rice particles through the conveying pipe. The choice of compressor depends on the material characteristics, conveying distance, and system capacity. For rice, which is relatively light and non-abrasive, a positive displacement blower is commonly used due to its efficiency and ability to maintain consistent air pressure. The control system, often integrated with sensors and valves, monitors the pressure, flow rate, and material level, allowing for real-time adjustments to optimize performance and prevent system failures.
The working principle of the rice pneumatic conveyor involves the following steps: First, rice is fed into the hopper from a storage silo or other feeding equipment. The material then flows into the conveying pipe through the discharge outlet. Simultaneously, the air compressor supplies compressed air into the pipe, creating a high-velocity air stream. The rice particles are entrained by the air flow and carried through the pipe to the discharge point. At the receiving end, the air and rice are separated, typically using a cyclone separator or a filter, and the rice is collected in a storage bin or processing unit. The air is then filtered and returned to the compressor, completing the cycle.
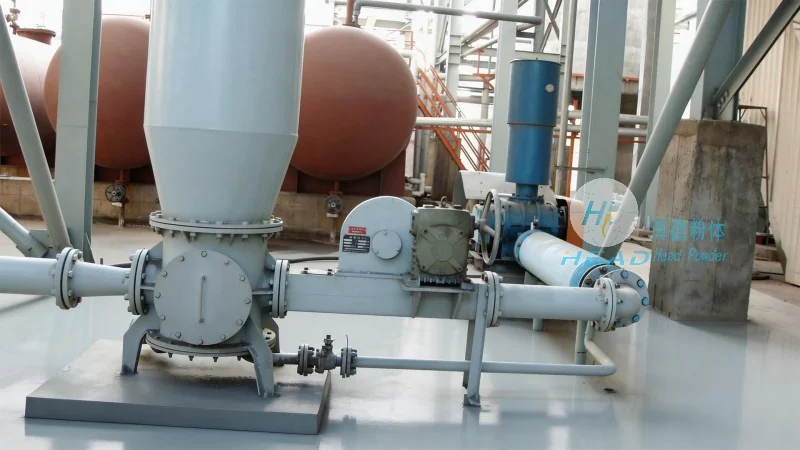
Key advantages of the rice pneumatic conveyor include its ability to handle bulk materials without the need for mechanical parts like belts or chains, reducing maintenance costs and increasing operational efficiency. It also minimizes material contamination and degradation, which is crucial for high-quality rice products. The system is compact and can be easily integrated into existing grain processing facilities, making it a versatile solution for various applications, from small-scale rice mills to large industrial processing plants.
HeadPowder, with its headquarters in Shandong, China, has been at the forefront of developing advanced pneumatic conveying solutions tailored to the rice industry. The company's expertise in material handling and engineering ensures that their rice pneumatic conveyors are designed to meet the specific needs of rice processing, offering reliable performance and durability. By leveraging cutting-edge technology and rigorous quality control, HeadPowder provides customers with equipment that enhances productivity and maintains the quality of rice throughout the conveying process.