

Introduction to Sulfur Powder Pneumatic Conveying Equipment and Its Structural Principles
Sulfur powder pneumatic conveying equipment is a specialized system engineered for the efficient and safe transportation of sulfur powder in industrial processes. As a critical component in sulfur handling operations, this equipment ensures reliable material transfer while maintaining operational safety and environmental compliance. The system is designed to address the unique characteristics of sulfur powder, such as its fine particle size and potential for dust generation, making it an essential solution for industries including chemical manufacturing, metallurgy, and fertilizer production.
Structural Design and Working Principle
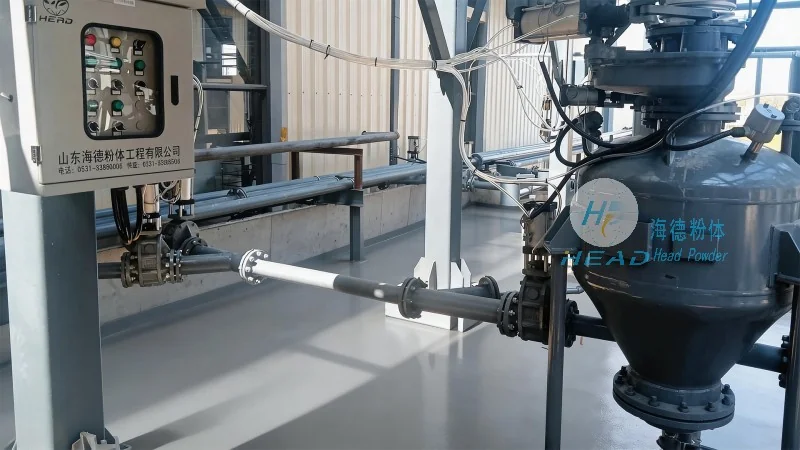
The sulfur powder pneumatic conveying system operates on the principle of air movement to transport solid particles. The core structure typically consists of a feeding unit, a conveying pipeline, a separation and recovery system, and a control unit. The feeding unit, often equipped with a rotary valve or screw feeder, introduces sulfur powder into the system under controlled conditions. The conveying pipeline, usually constructed from corrosion-resistant materials like stainless steel or polyethylene, transports the powder using compressed air or vacuum. The separation system, including cyclones or bag filters, separates the powder from the air stream, enabling material recovery and air purification. The control unit manages the entire process, regulating air pressure, flow rates, and operational parameters to ensure optimal performance.
Key Components and Their Functions
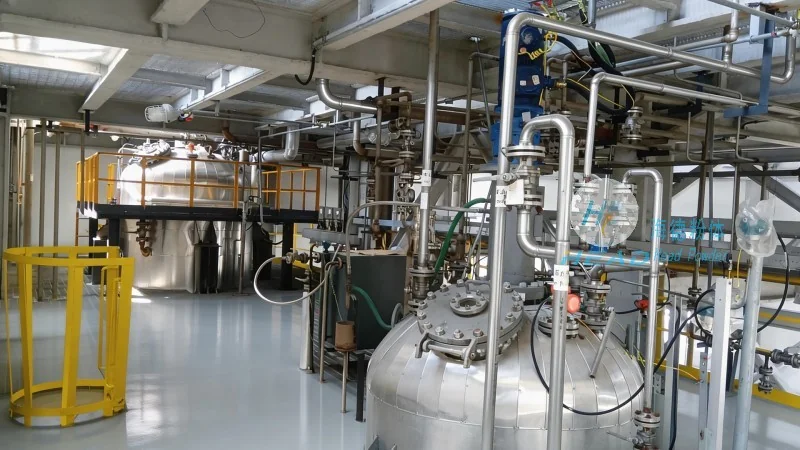
The sulfur powder pneumatic conveying equipment comprises several key components, each playing a vital role in the overall operation. The feeding device, such as a rotary valve or a screw feeder, is responsible for accurately metering and feeding the sulfur powder into the conveying line. The conveying pipeline, constructed from materials resistant to sulfur corrosion, ensures the safe and efficient transport of the powder. The separation unit, including cyclone separators or bag filters, effectively separates the powder from the air, preventing dust dispersion and enabling material recovery. The air compressor or vacuum pump provides the necessary pressure or suction to drive the material through the pipeline. The control system, equipped with sensors and automation, monitors and adjusts the process parameters to maintain stable operation and prevent system failures.
Advantages of the Equipment
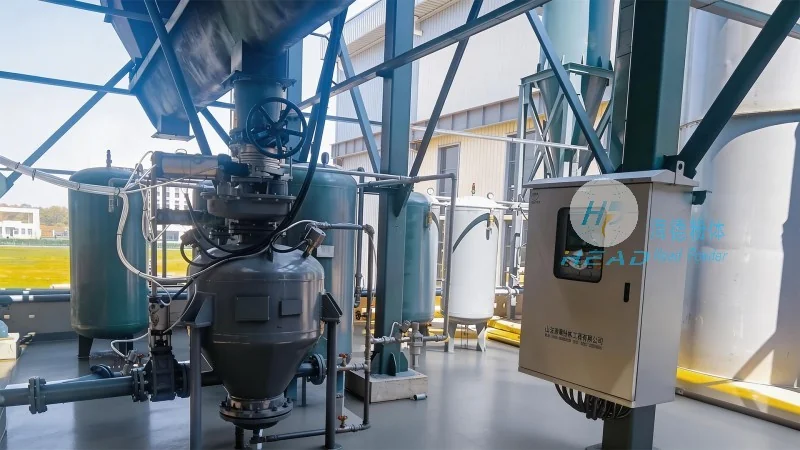
Implementing sulfur powder pneumatic conveying equipment offers numerous advantages for industrial applications. Firstly, it provides a dust-free and enclosed transport solution, significantly reducing the risk of dust explosions and improving workplace safety. Secondly, the system is highly efficient, capable of transporting large quantities of sulfur powder over long distances with minimal energy consumption. Thirdly, the equipment is adaptable to various process requirements, allowing for customization based on the specific characteristics of the sulfur powder and the operational environment. Additionally, the enclosed design helps maintain product quality by preventing contamination from external sources and minimizing material loss. The system also contributes to environmental sustainability by reducing waste and improving material recovery rates.
Application Scenarios
Sulfur powder pneumatic conveying equipment is widely used in various industrial sectors due to its versatility and efficiency. In the chemical industry, it is employed in the production of sulfuric acid, where sulfur powder is transported between reactors and storage tanks. In metallurgy, the equipment is utilized in processes involving sulfur-based reagents for metal refining. The fertilizer industry also benefits from this technology, as sulfur is a key component in many fertilizers, and the equipment ensures efficient handling and distribution of sulfur powders. Furthermore, in the petrochemical sector, sulfur powder is transported for processing and utilization in various chemical reactions. The equipment's ability to handle fine powders and maintain product integrity makes it suitable for applications where precision and reliability are critical.
Company Profile and Service
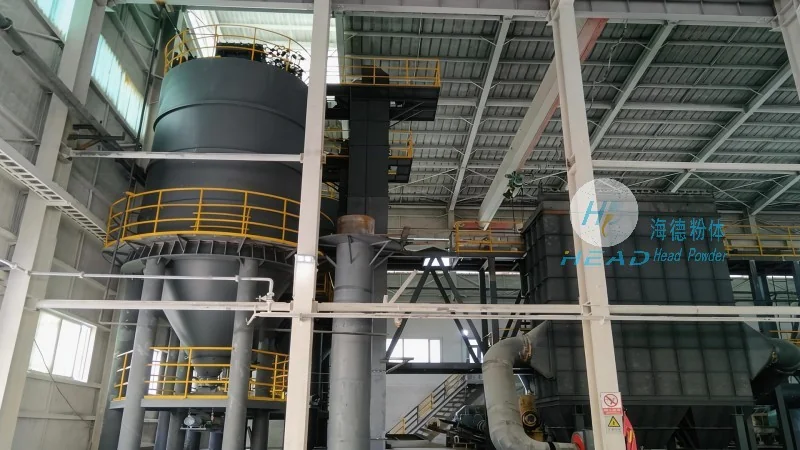
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a leading manufacturer and supplier of sulfur powder pneumatic conveying equipment. With a strong presence in China, particularly in Shandong, the company specializes in designing, manufacturing, and installing customized conveying systems tailored to the specific needs of its clients. HeadPowder's team of engineers and technicians leverages advanced technology and extensive industry experience to develop solutions that meet the highest standards of performance, safety, and reliability. The company provides comprehensive services, including system design, equipment installation, and after-sales support, ensuring that clients receive end-to-end solutions for their sulfur powder handling requirements. HeadPowder's commitment to quality and customer satisfaction has established it as a trusted partner in the industrial equipment sector, delivering reliable and efficient pneumatic conveying solutions to industries worldwide.