

Organic Fertilizer Pneumatic Conveying: How to Efficiently Transport Powder and Granular Materials w
Organic fertilizer is a vital component in modern agriculture, supplying essential nutrients to soil and supporting sustainable farming practices. However, the efficient handling and transportation of organic fertilizer materials—such as compost, manure, and granular organic products—can present significant challenges for agricultural and industrial operations. Traditional methods like manual labor or mechanical conveyors often suffer from low efficiency, high labor costs, and potential contamination risks. Pneumatic conveying, a technology that utilizes air flow to transport powder and granular materials, has emerged as a highly effective solution for these challenges. This article explores the principles and applications of organic fertilizer pneumatic conveying, highlighting how companies like Shandong HeadPowder Engineering Co., Ltd. (headpowder) leverage this technology to enhance material handling efficiency.
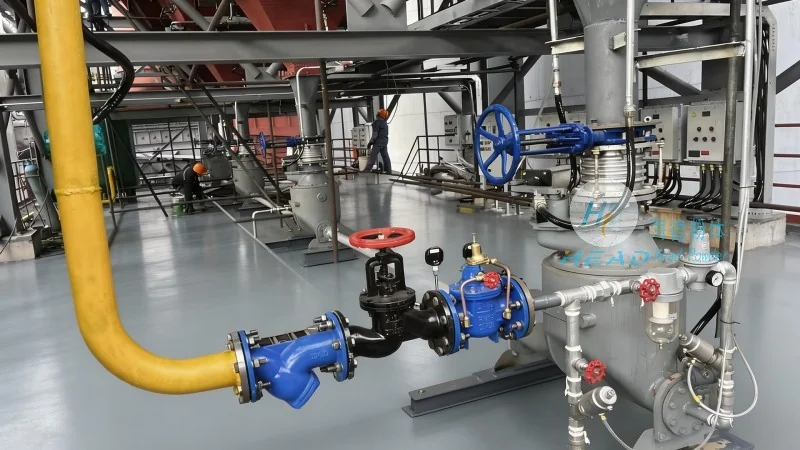
Understanding Pneumatic Conveying for Organic Fertilizer
Pneumatic conveying systems operate by using compressed air or suction to move bulk materials through a pipeline. The technology is particularly well-suited for organic fertilizer, which typically consists of fine powders and granules that are prone to dust and caking. Unlike mechanical conveyors, pneumatic systems can handle these materials without direct contact, reducing the risk of contamination and preserving product integrity. There are two primary types of pneumatic conveying: pressure and vacuum systems. Pressure systems employ positive pressure to push material through the pipeline, while vacuum systems use negative pressure to draw material from a source. The choice between these systems depends on factors such as material characteristics, distance, and system layout.
Key Benefits of Pneumatic Conveying for Organic Fertilizer
Implementing pneumatic conveying for organic fertilizer offers several advantages that make it an attractive option for businesses in the agricultural sector. First, it significantly improves operational efficiency by reducing the time and labor required for material transport. Unlike traditional methods that may involve multiple handling steps and equipment, pneumatic systems can transport materials over long distances with minimal human intervention. Second, pneumatic conveying enhances product quality by minimizing exposure to contaminants and preventing material degradation. The enclosed pipeline system ensures that organic fertilizer remains clean and free from external pollutants, which is critical for maintaining its nutritional value and effectiveness. Third, this technology contributes to environmental sustainability by reducing dust emissions and minimizing the need for additional packaging materials. By eliminating the need for manual handling, pneumatic systems also lower the risk of workplace accidents and improve overall safety in the workplace.
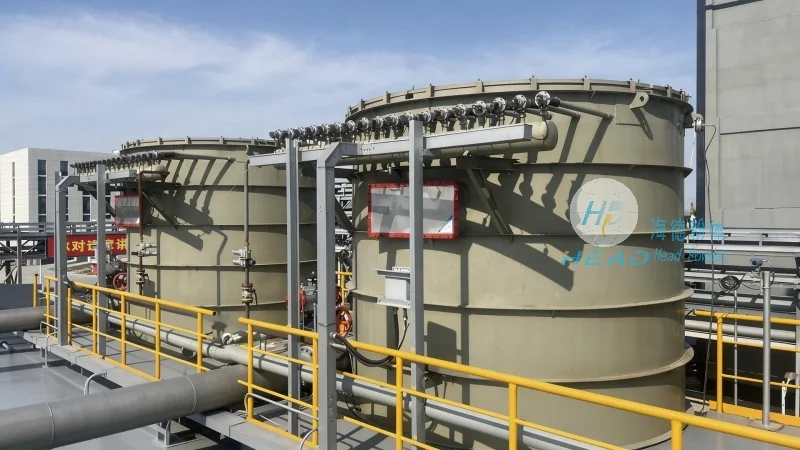
How Shandong HeadPowder Engineering Co., Ltd. Delivers Pneumatic Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading provider of pneumatic conveying solutions tailored to the organic fertilizer industry. With headquarters in Shandong, China, the company specializes in designing and manufacturing customized pneumatic systems that meet the unique needs of agricultural and industrial clients. headpowder's expertise lies in understanding the specific challenges of organic fertilizer, such as varying particle sizes, moisture content, and bulk density, and developing solutions that address these factors effectively. The company's team of engineers works closely with clients to assess their material handling requirements, site conditions, and operational goals to design a pneumatic conveying system that maximizes efficiency and cost-effectiveness.
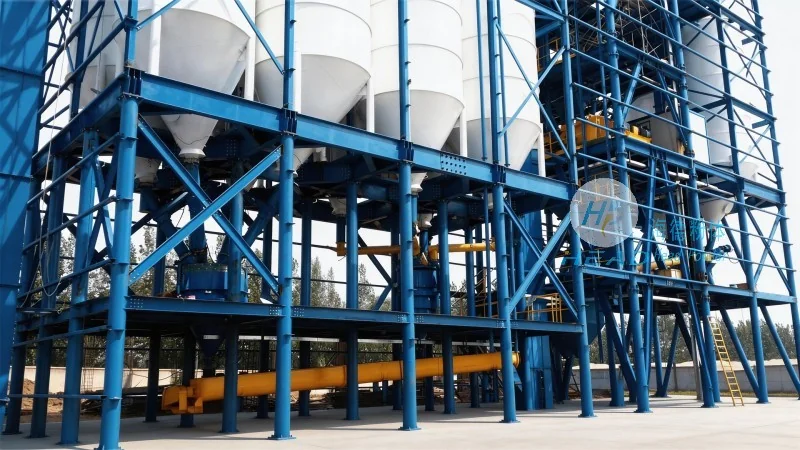
Technical Advancements in Organic Fertilizer Pneumatic Conveying
headpowder continuously invests in research and development to enhance the performance of pneumatic conveying systems for organic fertilizer. One of the key advancements is the use of advanced control systems that optimize air flow and pressure to ensure consistent material transport. These systems can adjust parameters in real-time based on material conditions, such as changes in particle size or moisture content, ensuring that the conveying process remains efficient and reliable. Another innovation is the integration of energy-efficient components, such as variable frequency drives (VFDs) and high-efficiency compressors, which reduce energy consumption and lower operational costs. Additionally, headpowder employs materials like stainless steel and food-grade plastics in the construction of its pneumatic systems to ensure durability and compliance with industry standards for organic fertilizer handling.
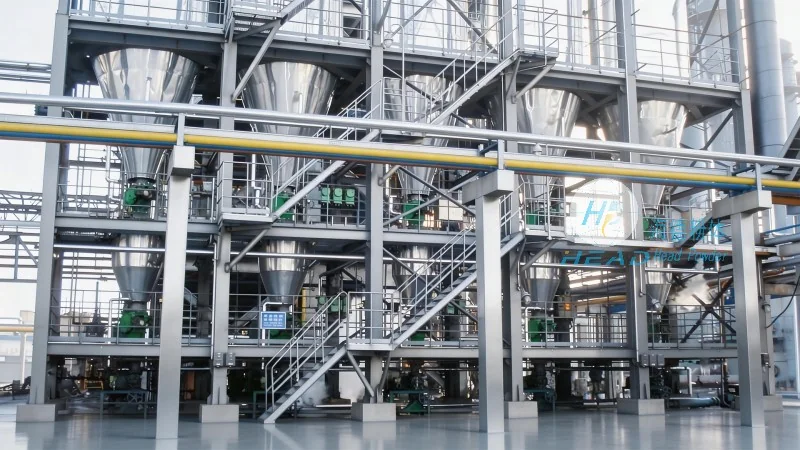
Application Examples and Case Studies
The effectiveness of pneumatic conveying for organic fertilizer is demonstrated through various applications across the industry. For instance, in compost production facilities, pneumatic systems are used to transport raw materials from storage silos to processing equipment and finished compost to packaging lines. This seamless integration of material flow improves production throughput and reduces downtime. In agricultural farms, pneumatic conveyors are employed to distribute organic fertilizer to fields, ensuring even application and maximizing nutrient uptake by crops. headpowder has successfully implemented such systems for clients ranging from small-scale farms to large-scale composting operations, with consistent positive results in terms of efficiency and product quality. These case studies highlight the versatility and reliability of pneumatic conveying as a solution for organic fertilizer handling.
Conclusion and Future Outlook
Pneumatic conveying represents a significant advancement in the efficient handling and transportation of organic fertilizer materials. By leveraging air flow to move powder and granular products, this technology offers substantial benefits in terms of efficiency, product quality, and environmental sustainability. Companies like Shandong HeadPowder Engineering Co., Ltd. play a crucial role in providing tailored solutions that address the specific needs of the organic fertilizer industry. As the demand for sustainable agricultural practices grows, the adoption of advanced pneumatic conveying systems will likely increase, further enhancing the capabilities of agricultural operations and supporting the global push towards more eco-friendly farming methods.