

What is a High-Pressure Pneumatic Conveyor? What are its Design Principles?
High-pressure pneumatic conveyors are industrial systems designed to transport bulk materials through a pipeline using compressed air as the driving force. These systems are widely used in various industries for efficient material handling, offering a flexible and reliable solution for moving powders, granules, and other particulate materials over long distances or within complex layouts.
Company Introduction
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a professional manufacturer specializing in the research, development, and production of high-pressure pneumatic conveying equipment. With a focus on innovation and quality, the company has established itself as a trusted supplier in the material handling industry, providing customized solutions tailored to meet the diverse needs of clients worldwide.
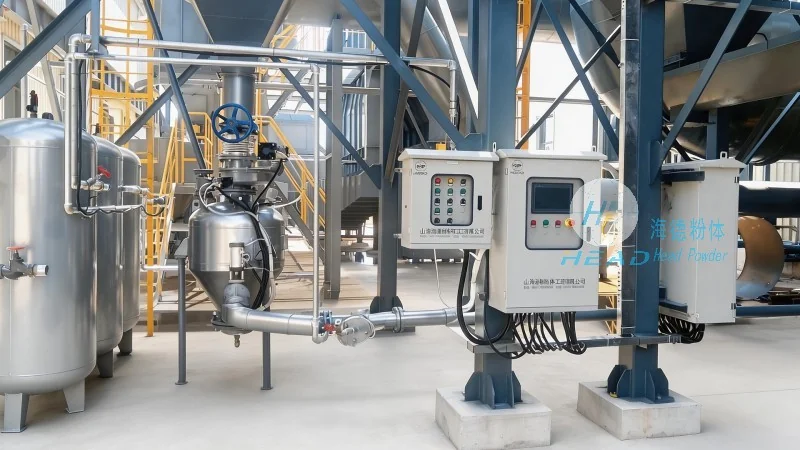
Product Overview: High-Pressure Pneumatic Conveyors
At the core of our product line is the high-pressure pneumatic conveyor, a sophisticated system engineered to handle a wide range of materials with precision and efficiency. These conveyors operate by injecting high-pressure air into a sealed pipeline, creating a pressure differential that propels the material forward. The system typically includes components such as a feeding hopper, a pressure vessel, a control valve, and a discharge unit, all working in harmony to ensure smooth and consistent material transport. Our high-pressure pneumatic conveyors are designed to handle materials with varying particle sizes, densities, and flow characteristics, making them suitable for applications in pharmaceuticals, food processing, chemical manufacturing, and more.
Design Principles of High-Pressure Pneumatic Conveyors
The design of a high-pressure pneumatic conveyor is based on several key principles that ensure optimal performance and reliability. First, the system relies on the principle of fluidization, where compressed air is introduced into the material bed, creating a fluid-like state that allows the material to be moved as a single stream. This fluidization process minimizes material degradation and ensures uniform transport. Second, the design incorporates pressure control mechanisms to maintain consistent air pressure, which is critical for controlling the velocity and flow rate of the material. Additionally, the system features a sealed pipeline to prevent dust emissions and maintain material integrity, adhering to environmental and safety standards. The control system, often integrated with sensors and automation, allows for real-time monitoring and adjustment of the conveying process, enhancing operational efficiency and reducing downtime.
Key Features and Advantages
Our high-pressure pneumatic conveyors offer several advantages that make them a preferred choice for industrial applications. One of the primary benefits is their ability to transport materials over long distances with minimal energy consumption compared to traditional methods like belt conveyors or bucket elevators. The system’s flexibility allows for easy integration into existing production lines or new facilities, with the ability to change the direction or layout of the pipeline as needed. Furthermore, the sealed design reduces dust contamination, which is particularly important in industries such as food and pharmaceuticals where product purity is paramount. The system also provides a hygienic and clean operation, as the materials are contained within the pipeline, preventing exposure to external contaminants. Another advantage is the reduced maintenance requirements, as the components are designed for durability and longevity, with minimal moving parts that can wear out over time.