

What is a Rare Earth Powder Material Handling System? And What Are Its Design Principles?
When it comes to handling rare earth powders, an efficient and reliable material handling system is crucial for industrial applications. The rare earth powder material handling system, as provided by Shandong HeadPowder Engineering Co., Ltd. from China, is designed to address the unique challenges associated with these specialized powders. This system is engineered to ensure safe, clean, and efficient transportation of rare earth powders, which are often characterized by their fine particle size, potential for static charge, and tendency to agglomerate or clog conventional equipment.
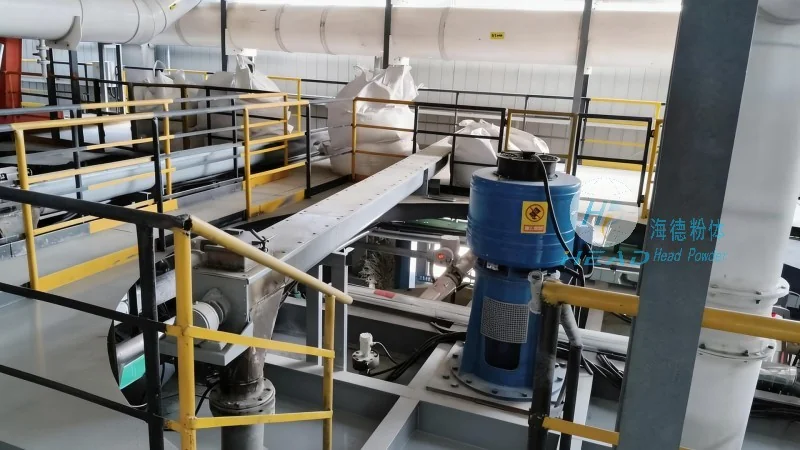
Understanding the Rare Earth Powder Material Handling System
The rare earth powder material handling system is a comprehensive solution tailored for the transportation of rare earth powders, which are critical components in various high-tech industries such as electronics, renewable energy, and advanced manufacturing. These powders, including elements like neodymium, praseodymium, and dysprosium, require specialized handling due to their chemical and physical properties. The system is designed to minimize dust generation, prevent material loss, and maintain product integrity throughout the handling process. By integrating advanced engineering principles and materials handling expertise, the system ensures that rare earth powders are transported safely and efficiently, meeting the stringent requirements of modern industrial processes.
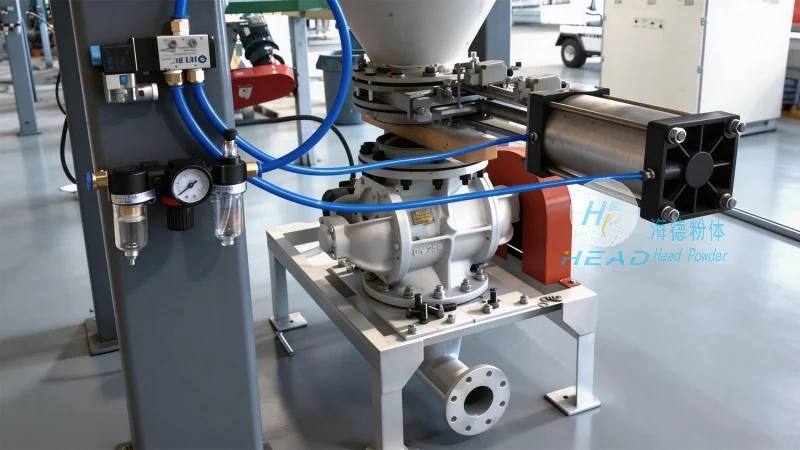
Key Design Principles for the Material Handling System
The design of the rare earth powder material handling system is based on several fundamental principles that address the unique challenges of handling these powders. First, the system employs a fully enclosed design to prevent dust contamination and environmental exposure. This is critical because rare earth powders can be hazardous if inhaled or if they come into contact with sensitive equipment. Second, the system incorporates anti-static measures to prevent electrostatic discharge, which can cause sparks and potentially ignite dust explosions. Third, the equipment is constructed from materials that are resistant to corrosion and wear, ensuring long-term durability and reliability. Additionally, the system is designed for easy maintenance and cleaning, which is essential for maintaining product purity and compliance with industry standards. The combination of these design principles results in a robust and efficient material handling solution that meets the demands of modern rare earth processing facilities.
Components and Functionality of the Material Handling System
The rare earth powder material handling system typically consists of several key components that work together to ensure seamless material transport. The primary components include feeders, conveyors, and control systems. The feeders are designed to handle the fine particles of rare earth powders, ensuring consistent and controlled feeding into the conveyor system. The conveyors, often using pneumatic or mechanical methods, transport the powders through the system while maintaining the enclosed environment. The control systems monitor and regulate the flow of material, ensuring that the system operates within safe and efficient parameters. Each component is carefully selected and integrated to maximize performance and minimize downtime. For example, the use of flexible hoses and sealed joints in the pneumatic system prevents leaks and maintains the integrity of the material being handled. The mechanical conveyors, such as screw conveyors, are equipped with special coatings to prevent material buildup and ensure smooth operation. Together, these components form a cohesive system that delivers reliable and efficient material handling for rare earth powders.
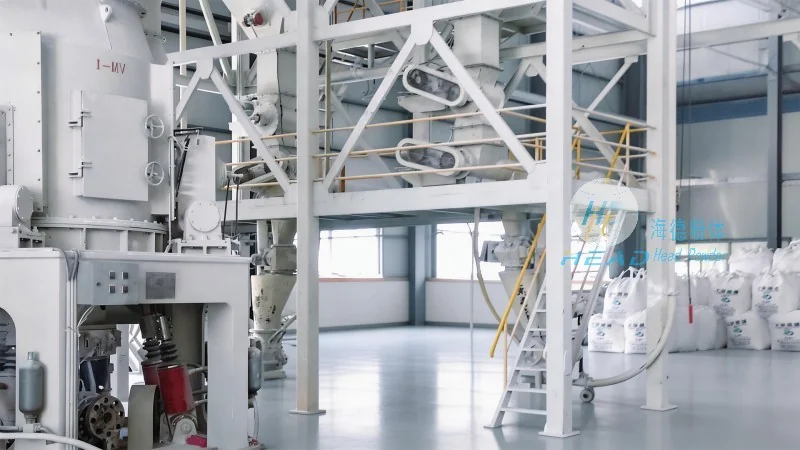
Applications and Benefits of the Material Handling System
The rare earth powder material handling system is widely used in various industrial applications where rare earth powders are processed and transported. These applications include the production of magnets, batteries, and catalysts, where the purity and consistency of the powders are critical. The system's ability to handle these powders without contamination or degradation makes it an essential part of the manufacturing process. The benefits of using this system include improved safety, reduced operational costs, and enhanced product quality. By minimizing dust exposure and preventing material loss, the system helps to create a safer working environment and reduces the need for costly cleanup and maintenance. Additionally, the efficient transport of materials leads to increased productivity and reduced downtime, which are vital for maintaining competitiveness in the rare earth industry. The system's adaptability also allows it to be integrated into existing production lines, providing a seamless transition to more advanced material handling solutions.