

What is a Negative Pressure Vacuum Powder Conveyor? And What Are Its Design Principles?
When it comes to efficiently transporting bulk powders and granules in industrial settings, the negative pressure vacuum powder conveyor stands out as a critical piece of equipment. This system is engineered to handle a wide range of materials, from fine powders to larger granules, while maintaining a controlled and safe environment. As a leading manufacturer in the field, Shandong HeadPowder Engineering Co., Ltd. specializes in providing high-quality solutions tailored to meet diverse industrial needs. With a focus on innovation and precision, their products are designed to enhance operational efficiency and ensure reliable performance in various applications.
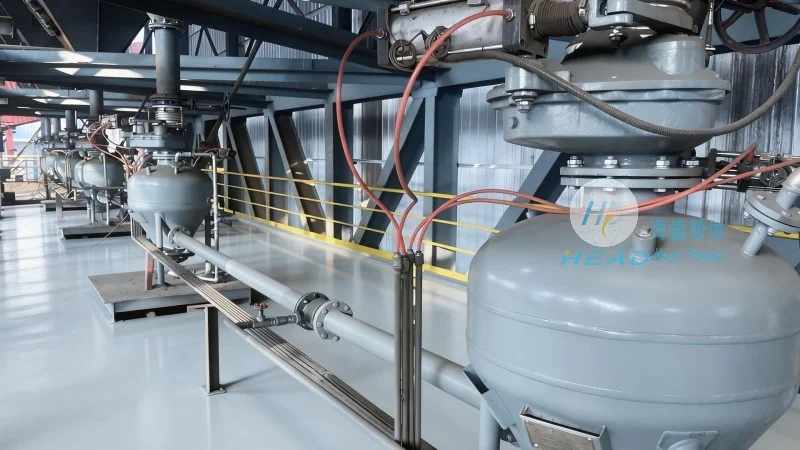
Understanding the Negative Pressure Vacuum Powder Conveyor
A negative pressure vacuum powder conveyor operates by creating a vacuum within the system to draw material from a source, such as a hopper or storage silo, and transport it to a destination, like a processing unit or packaging line. The core principle involves using a vacuum pump to generate a pressure differential that pulls the material through a sealed pipeline. This method is particularly advantageous for handling materials that are prone to dust, caking, or contamination, as it minimizes exposure to the environment and maintains a clean transfer process.
Key Design Principles of the Conveyor
The design of a negative pressure vacuum powder conveyor incorporates several critical elements that contribute to its effectiveness. First, the system relies on a robust vacuum pump, typically a rotary vane or Roots blower, which generates the necessary suction force. The pipeline network is constructed from materials resistant to corrosion and wear, such as stainless steel or specialized polymers, to ensure durability and prevent material degradation. Additionally, the conveyor features a series of inlets and outlets strategically placed to facilitate smooth material flow, with options for multiple pickup points and discharge locations. The control system, often integrated with sensors and automation, allows for precise regulation of the vacuum level and flow rate, ensuring optimal performance and minimizing energy consumption.
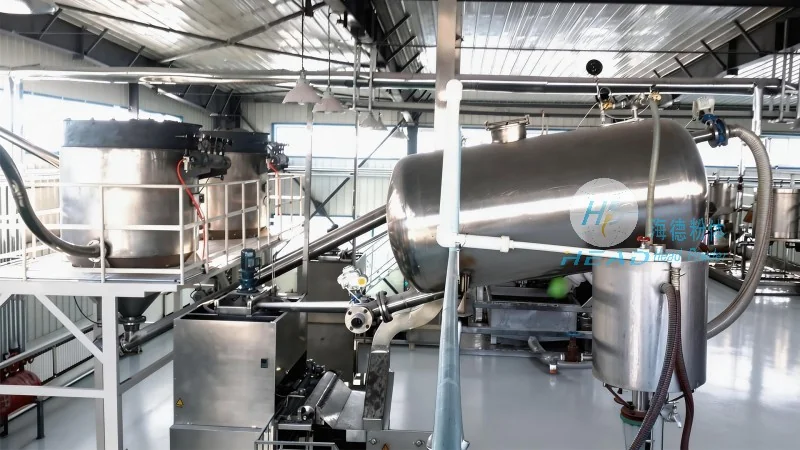
How the System Works: A Step-by-Step Overview
Operating the negative pressure vacuum powder conveyor involves a sequence of steps that ensure efficient material transfer. Initially, the vacuum pump is activated, creating a low-pressure environment within the pipeline. As the pump draws air and material from the source, the material is entrained in the airflow and carried through the sealed system. The material is then discharged at the destination, where the pressure is higher, allowing it to fall out of the stream. The system is equipped with filters and cyclones to separate the material from the air, ensuring that only the desired product is delivered to the processing line. This process is continuous and can be adjusted to handle varying material volumes and types, making it versatile for different industrial applications.
Advantages of Using a Negative Pressure Vacuum Conveyor
Implementing a negative pressure vacuum powder conveyor offers numerous benefits for industrial operations. One of the primary advantages is the ability to handle dusty or hazardous materials without exposing personnel to the material during transfer. The sealed system prevents dust emissions, reducing the risk of contamination and improving workplace safety. Additionally, the system minimizes material loss and degradation, as the material is kept in a controlled environment throughout the transfer process. The design also allows for flexible installation, with the ability to add or remove pickup points as needed, adapting to changing production requirements. Furthermore, the energy efficiency of modern vacuum pumps and the precise control of flow rates contribute to lower operational costs and reduced environmental impact.
Applications and Industries
The negative pressure vacuum powder conveyor is widely used across various industries that require the handling of bulk materials. In the pharmaceutical and food industries, it is essential for transferring powders and granules while maintaining strict hygiene standards. The chemical industry utilizes this system for handling abrasive or corrosive materials, ensuring safe and efficient transport. The agricultural sector also benefits from the conveyor's ability to handle grain and other agricultural products, reducing the risk of spoilage and contamination. Additionally, in the construction and mining industries, the system is used for transporting raw materials like cement, sand, and gravel, improving productivity and safety on job sites.
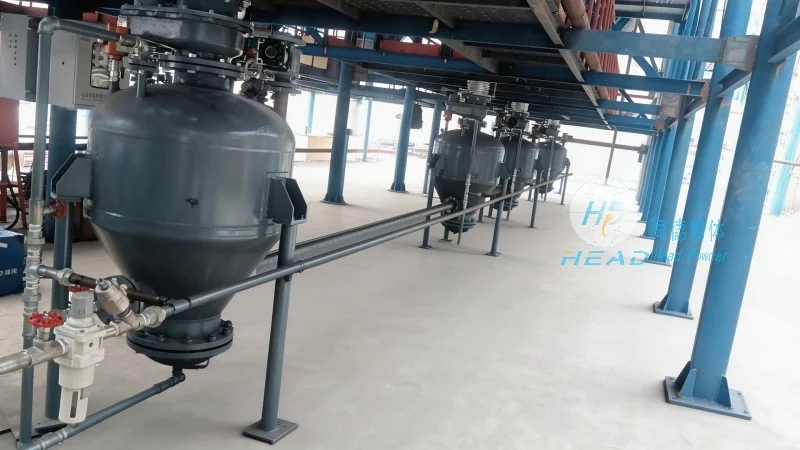
Customization and Solutions from Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd. understands that each industrial application has unique requirements. Therefore, they offer customized solutions tailored to specific needs. Their team of engineers works closely with clients to design and manufacture negative pressure vacuum powder conveyors that meet exact specifications, including material type, flow rate, and environmental conditions. The company provides a range of options, from standard models to specialized configurations, ensuring that clients can find a solution that fits their operational demands. With a focus on quality and reliability, HeadPowder's products are built to withstand heavy use and provide long-term performance, making them a trusted choice in the industry.
Conclusion: The Importance of Proper Design and Implementation
In conclusion, the negative pressure vacuum powder conveyor is a sophisticated and essential piece of equipment for efficient bulk material handling. Its design principles, which focus on creating a controlled vacuum environment and utilizing robust components, ensure reliable and safe operation. By understanding the system's functionality and advantages, industries can optimize their material transfer processes, improve productivity, and enhance workplace safety. As a leading manufacturer, Shandong HeadPowder Engineering Co., Ltd. plays a vital role in providing high-quality solutions that meet the evolving needs of modern industrial operations, contributing to the advancement of efficient and sustainable material handling practices.