

What is a Mineral Sand Powder Conveying System Equipment? Exploring Design Principles
Mineral sand powder conveying systems are critical in various industrial processes, particularly in the mining and processing sectors where efficient material handling is essential. These systems are designed to transport bulk materials like mineral sands, powders, and granules with precision and reliability. Understanding the equipment's functionality and design principles is crucial for optimizing operational efficiency and ensuring safety in industrial applications.
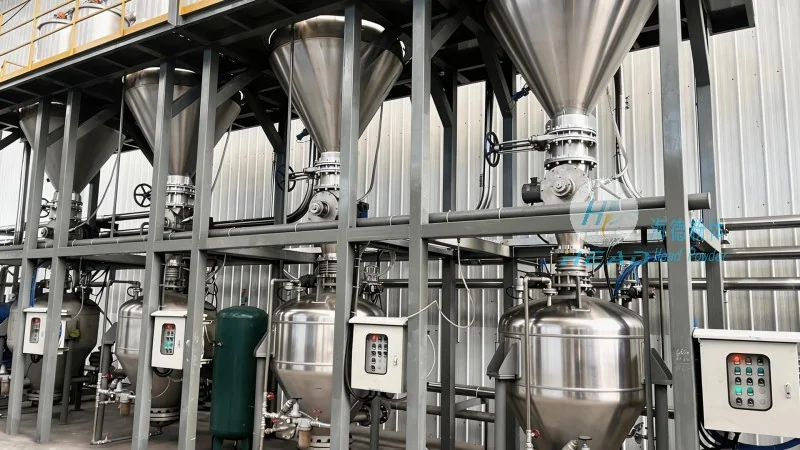
Key Components and Functions of the Equipment
The core components of a mineral sand powder conveying system typically include a feeding mechanism, a conveying pipeline, a drive system, and a control unit. The feeding mechanism ensures consistent material intake, while the pipeline (often made of durable materials like stainless steel or special polymers) transports the powder. The drive system, which may include motors and pulleys, provides the necessary force to move the material through the pipeline. The control unit allows operators to monitor and adjust the system's performance, ensuring optimal operation under varying conditions.
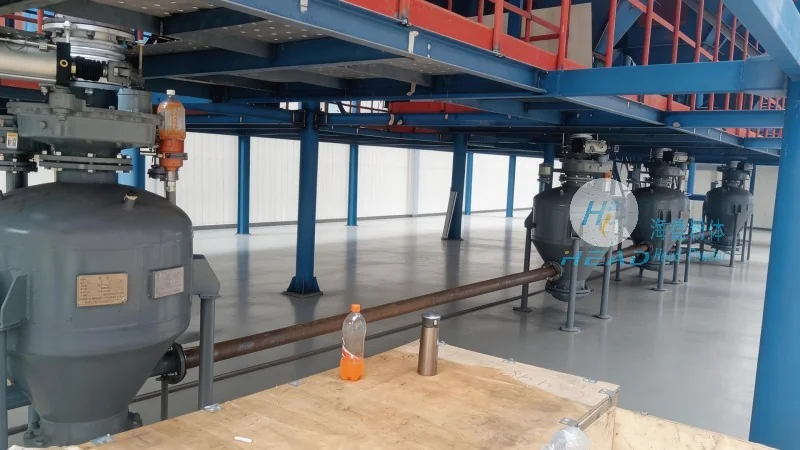
Design Principles and Technical Specifications
The design principles of these systems focus on efficiency, durability, and adaptability. Engineers consider factors such as material properties (e.g., particle size, moisture content, and flowability), system capacity, and environmental conditions when designing the equipment. For instance, the choice of pipeline material is critical to prevent material buildup or corrosion, which can affect system performance over time. Additionally, the system's layout is optimized to minimize energy consumption and maximize material throughput, aligning with modern industrial standards for sustainability and cost-effectiveness.
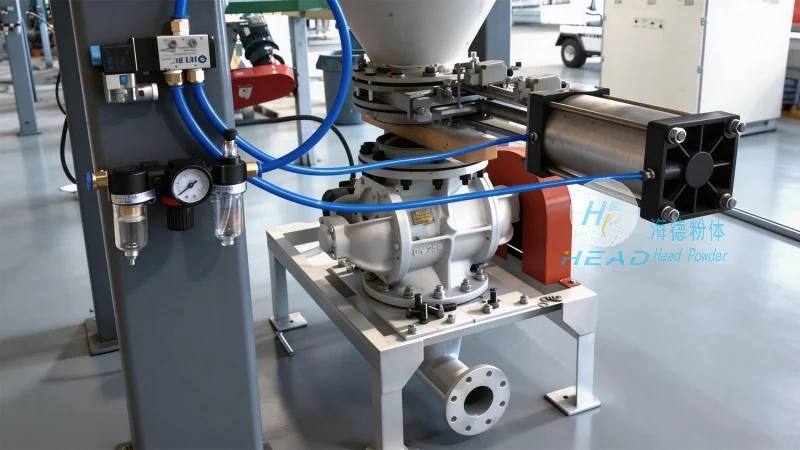
Application Scenarios and Operational Benefits
These conveying systems are widely used in industries such as mining, chemical processing, and food production. In mining operations, they facilitate the transport of mineral sands from processing plants to storage or shipping facilities. In chemical processing, they help move powders for mixing and manufacturing, ensuring consistent product quality. The operational benefits include reduced labor costs, minimized material loss, and enhanced safety by eliminating manual handling of bulk materials. Furthermore, the systems can be integrated with other industrial equipment, such as crushers and classifiers, to form a comprehensive material handling solution.
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer specializing in mineral sand powder conveying systems and related engineering solutions. With a strong focus on innovation and quality, the company has established itself as a trusted partner in the industry. HeadPowder's products are designed to meet the diverse needs of clients, offering customizable solutions that enhance operational efficiency and reliability. The company's headquarters is located in Shandong, China, where it leverages advanced technology and skilled workforce to develop cutting-edge equipment.

Conclusion
In summary, mineral sand powder conveying systems are essential for efficient material handling in industrial applications. The design principles and components of these systems are tailored to meet specific operational requirements, ensuring reliable and sustainable performance. With companies like Shandong HeadPowder Engineering Co., Ltd. providing advanced solutions, industries can optimize their material transport processes and achieve greater productivity. By understanding the technology and design behind these systems, businesses can make informed decisions to enhance their operational capabilities and stay competitive in the market.