

What is a Pharmaceutical Granule Material Handling System? What are its Design Principles?
Pharmaceutical granule material handling systems are specialized equipment used in the pharmaceutical industry to transport, convey, and manage granular materials such as active pharmaceutical ingredients (APIs), excipients, and other raw materials. These systems are critical for ensuring the efficient and safe processing of materials throughout the manufacturing process. The design of these systems must adhere to stringent regulatory standards, including those from the FDA and other international health authorities, to maintain product quality and safety.
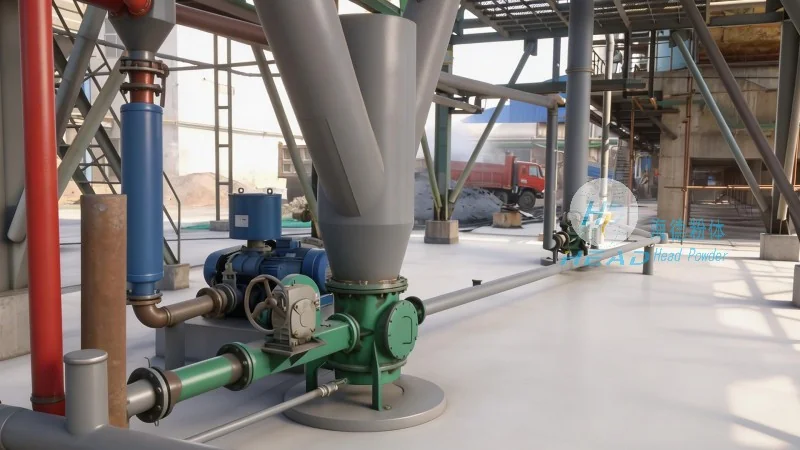
Key Components and Functions of Granule Material Handling Systems
The core components of a pharmaceutical granule material handling system typically include feeders, conveyors, storage bins, and control systems. Feeders are used to regulate the flow of granules from storage bins to processing equipment, ensuring consistent and controlled material delivery. Conveyors, such as belt conveyors or screw conveyors, transport the granules between different stages of the manufacturing line. Storage bins provide temporary storage for raw materials, allowing for batch processing and inventory management. Control systems, often integrated with PLCs (Programmable Logic Controllers), monitor and control the operation of all components to ensure smooth and safe material handling.
Design Principles for Efficient and Safe Material Handling
The design principles of pharmaceutical granule material handling systems focus on several key aspects: first, ensuring minimal product contamination through the use of stainless steel or other inert materials for construction; second, maintaining consistent material flow to prevent clogging or uneven distribution; third, incorporating safety features such as emergency stop buttons and overload protection to protect operators and equipment; and fourth, designing for easy cleaning and maintenance to comply with GMP (Good Manufacturing Practice) regulations. These principles are crucial for maintaining product integrity and meeting regulatory requirements.
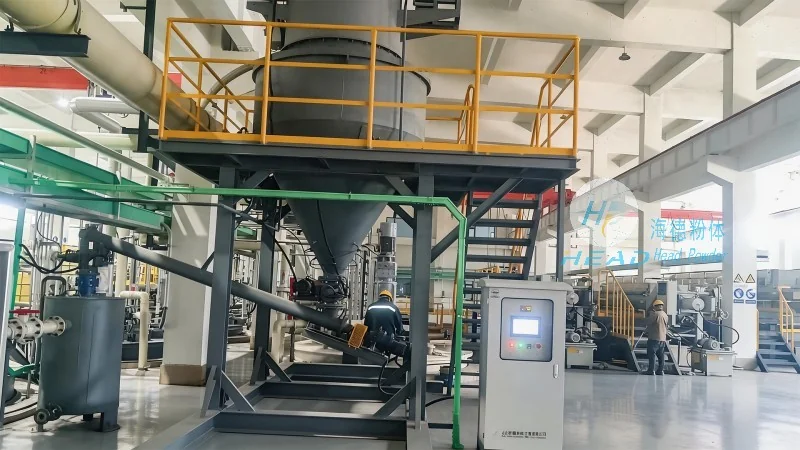
HeadPowder Engineering: Experts in Pharmaceutical Material Handling Solutions
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of pharmaceutical material handling systems. With a strong commitment to quality and innovation, HeadPowder specializes in designing and manufacturing customized solutions tailored to the unique needs of the pharmaceutical industry. The company's expertise lies in understanding the complex requirements of granule processing, from raw material handling to final product packaging, and delivering systems that enhance efficiency, safety, and compliance.
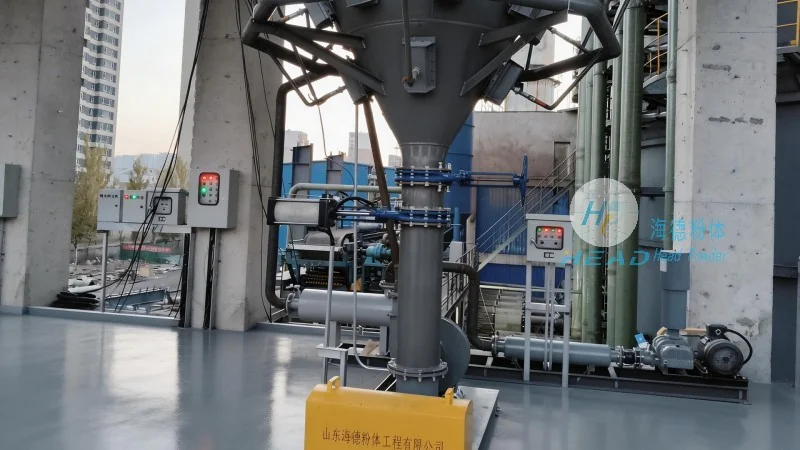
Customization and Integration Capabilities
HeadPowder's pharmaceutical granule material handling systems are highly customizable to meet specific production requirements. The company works closely with clients to understand their operational needs, process flow, and regulatory constraints, then designs systems that integrate seamlessly with existing manufacturing lines. This approach ensures that the final solution is not only efficient but also scalable and adaptable to future production changes. The integration of advanced control systems and monitoring technologies further enhances the performance and reliability of the material handling processes.
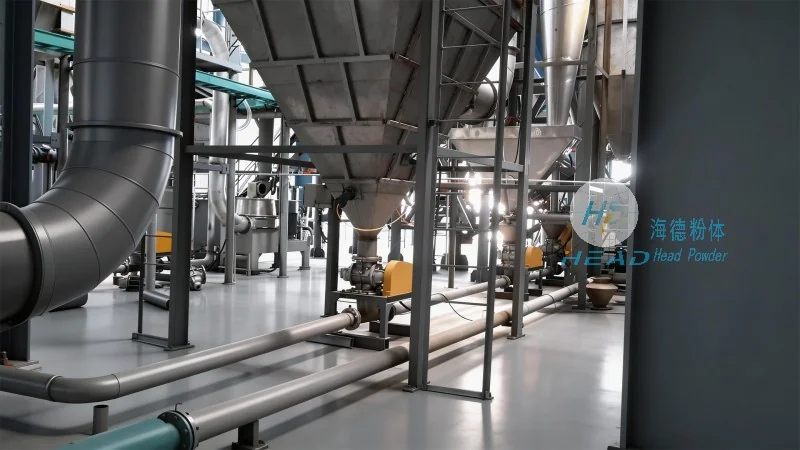
Quality Assurance and Compliance
At HeadPowder, quality is at the heart of everything we do. The company adheres to international quality management standards, including ISO 9001, and ensures that all products meet or exceed industry regulations. Each system is rigorously tested and validated to confirm that it operates within specified parameters and complies with GMP requirements. This commitment to quality assurance provides clients with confidence that their material handling systems are reliable, safe, and effective in supporting their pharmaceutical manufacturing operations.
Conclusion: The Importance of Reliable Granule Material Handling Systems
In conclusion, pharmaceutical granule material handling systems are essential for the efficient and safe processing of raw materials in the pharmaceutical industry. The design principles that guide these systems—such as contamination control, consistent flow, safety features, and easy maintenance—are critical for maintaining product quality and regulatory compliance. With its expertise and commitment to quality, Shandong HeadPowder Engineering Co., Ltd. (HeadPowder) offers advanced and customized solutions that meet the evolving needs of the pharmaceutical sector, helping manufacturers optimize their operations and deliver high-quality medications to patients worldwide.