Recycled sand powder conveyors are essential equipment in modern foundries and casting industries, designed to efficiently handle and transport reclaimed sand materials. As a key component in sand recycling systems, these conveyors play a crucial role in optimizing the production process and reducing material waste. The following article will explore the working principle and key features of such equipment, providing insights into how they enhance operational efficiency and sustainability.
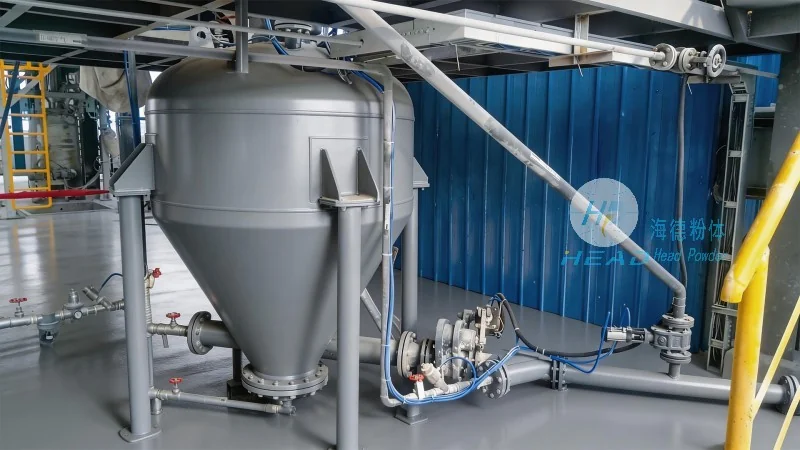
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design, development, and production of advanced powder handling solutions. With a strong commitment to innovation and quality, the company has established itself as a trusted partner for industries seeking reliable and efficient conveyor systems for recycled sand applications.
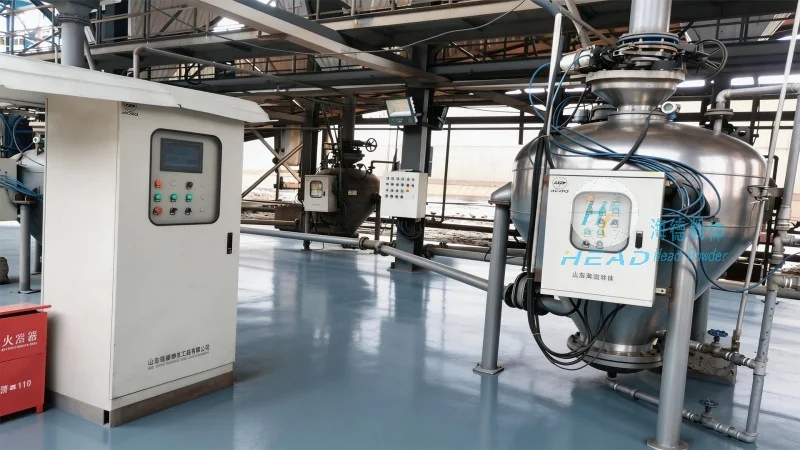
The operation of a recycled sand powder conveyor typically involves several key components and processes. The system starts with the collection of reclaimed sand from various sources, such as sand traps or recycling bins. This material is then fed into the conveyor's inlet, where it is transported through a series of mechanisms. Many models utilize a screw or auger design, which rotates to move the sand along the conveyor path. The screw or auger is enclosed in a robust housing, often made of stainless steel or other corrosion-resistant materials, to ensure durability and prevent material leakage. As the sand moves, it is propelled forward by the rotating screw, maintaining a consistent flow rate. Some advanced systems may incorporate additional features, such as air-assisted or vacuum suction, to enhance material handling capabilities, especially for fine powders or materials with low bulk density. The conveyor's speed and capacity can be adjusted based on the specific requirements of the application, allowing for flexible operation. The discharge end of the conveyor then delivers the processed sand to the next stage of the recycling process, such as screening or reclamation.
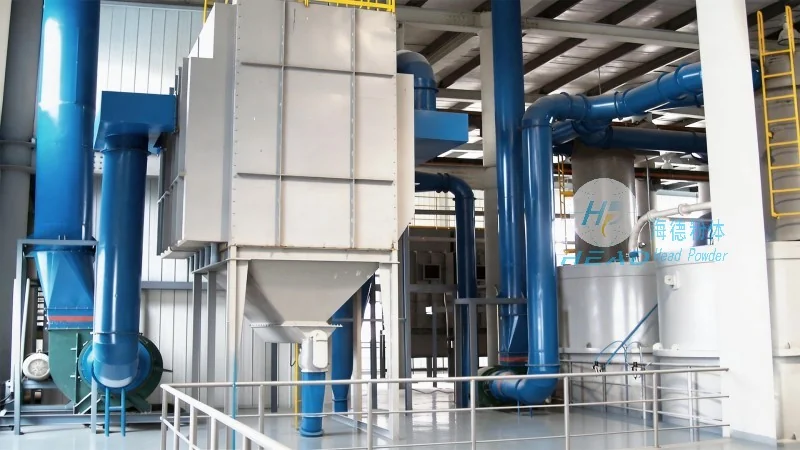
Recycled sand powder conveyors from HeadPowder are characterized by several notable features that set them apart in the market. First, the equipment is designed for high efficiency and reliability, ensuring consistent performance even under heavy load conditions. The robust construction, using high-quality materials, minimizes maintenance requirements and extends the service life of the conveyor. Another key feature is the adjustable speed control, which allows operators to optimize the conveyor's output based on production needs. This flexibility is particularly valuable in dynamic manufacturing environments where demand for reclaimed sand fluctuates. Additionally, the conveyors are equipped with safety features, such as overload protection and emergency stop buttons, to ensure safe operation and prevent accidents. The design also prioritizes ease of maintenance, with accessible components that can be easily cleaned or replaced. This reduces downtime and maintenance costs, contributing to overall operational efficiency. Furthermore, the conveyors are engineered to handle a wide range of sand types, including fine, coarse, and mixed reclaimed sand, making them versatile for various casting applications. The use of corrosion-resistant materials ensures that the equipment can withstand the abrasive nature of sand particles, prolonging its lifespan. The compact design of the conveyors also allows for easy integration into existing production lines, minimizing installation time and costs.
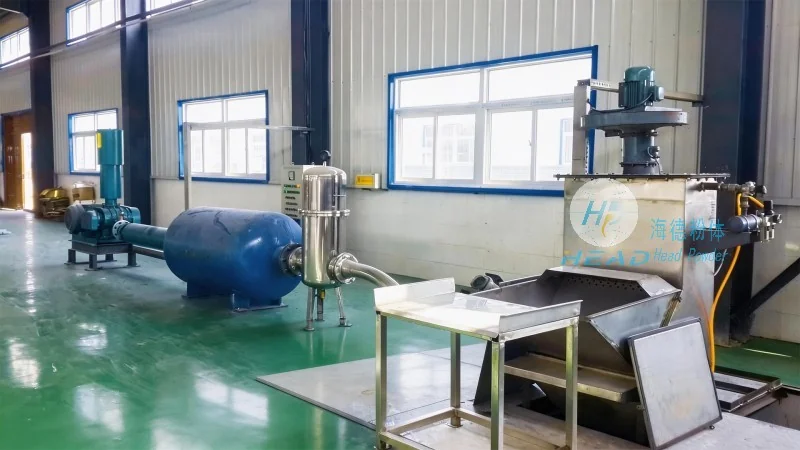
The performance of recycled sand powder conveyors is optimized through several design elements that enhance functionality and durability. The screw or auger mechanism is engineered to provide consistent material flow, reducing the risk of clogging or uneven distribution. This ensures that the reclaimed sand is delivered uniformly to subsequent processing stages, improving the efficiency of the overall recycling system. The use of high-quality bearings and seals in the conveyor's components minimizes friction and wear, leading to lower energy consumption and longer operational life. Additionally, the conveyors are designed to operate in harsh environments, with features such as dust-proof enclosures and protective covers that prevent contamination and damage from external factors. This makes them suitable for use in foundries where dust and debris are common. The adjustable speed and capacity settings allow operators to match the conveyor's output to the production rate of the casting process, ensuring that sand is available when needed without overloading the system. This balance between supply and demand enhances overall production efficiency and reduces waste. Furthermore, the conveyors are equipped with monitoring systems that provide real-time data on performance, such as flow rate and temperature, enabling operators to identify and address issues promptly. This proactive approach to maintenance helps to prevent breakdowns and extends the lifespan of the equipment.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan City, Shandong Province, China

telephone
WeChatconsult
top