

Working Principle and Features of Pharmaceutical Granule Material Handling System Equipment
Pharmaceutical granule material handling systems are integral to modern pharmaceutical manufacturing, facilitating the efficient transport and management of granular materials throughout the production process. These systems are designed to handle a variety of granules, including active pharmaceutical ingredients (APIs), excipients, and other raw materials, ensuring that they are moved safely, accurately, and in compliance with regulatory standards. The primary goal of such systems is to optimize production line efficiency, minimize material loss, and maintain consistent product quality. Understanding the working principle and key features of these systems is crucial for pharmaceutical manufacturers seeking to enhance their operational capabilities and meet the demands of a competitive market.
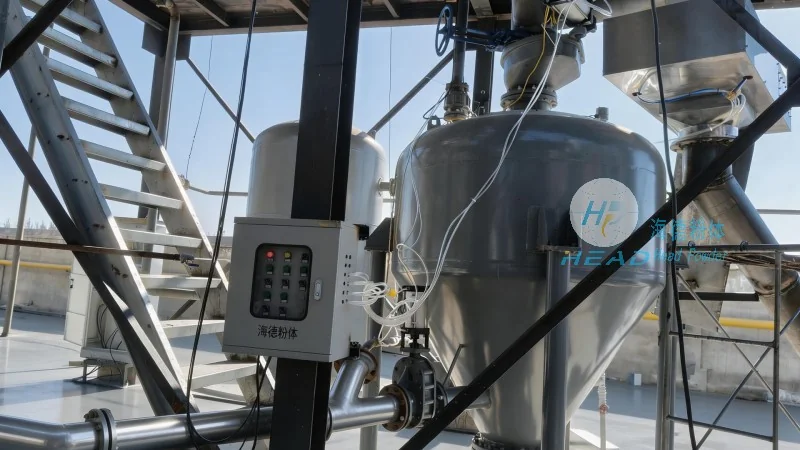
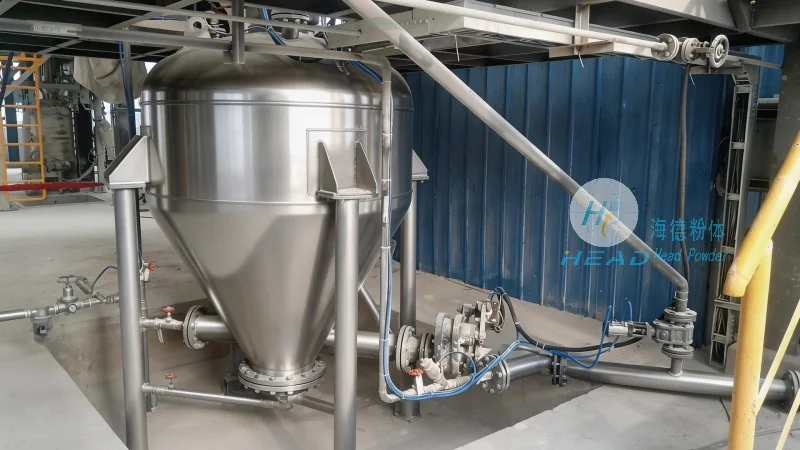
Working Principle of the Pharmaceutical Granule Material Handling System
The working principle of a pharmaceutical granule material handling system involves a series of coordinated actions that ensure the smooth flow of material from input to output. The system typically begins with a hopper or feeder, which stores and feeds the granules into the transport mechanism. The feeder is designed to provide a controlled and uniform flow of material, preventing overloading or underfeeding that could disrupt the process. Next, the granules are conveyed through a conveyor system, which may include belt conveyors, screw conveyors, or pneumatic conveyors, depending on the material's characteristics and the required transport distance. Belt conveyors are commonly used for horizontal or slight incline transport, while screw conveyors are ideal for vertical or inclined movement, especially for materials with higher moisture content. Pneumatic conveyors, or air slides, are used for fine powders and require a controlled air pressure system to move the material. Throughout the transport process, the system is equipped with sensors and control panels that monitor parameters such as flow rate, pressure, and temperature. These sensors provide real-time data to the control system, allowing for immediate adjustments to maintain optimal performance. For example, if the flow rate exceeds the set limit, the system can automatically reduce the feed rate or adjust the conveyor speed to prevent material buildup or spillage. The final stage of the system involves directing the granules to the next processing step, such as blending, coating, or packaging, ensuring that the material is handled with precision and minimal degradation.

Key Features of the Pharmaceutical Granule Material Handling System
HeadPowder's pharmaceutical granule material handling systems are distinguished by several key features that enhance their performance, reliability, and adaptability in pharmaceutical manufacturing. One of the most significant features is the use of high-quality stainless steel construction, which is essential for meeting the stringent hygiene and sanitation requirements of the pharmaceutical industry. The equipment is designed with smooth, non-porous surfaces that are easy to clean and sanitize, reducing the risk of cross-contamination and ensuring compliance with regulatory standards such as GMP (Good Manufacturing Practice). Another critical feature is the integration of advanced control systems, which provide precise and automated control over the material flow. These systems use programmable logic controllers (PLCs) and human-machine interfaces (HMIs) to allow operators to monitor and adjust parameters such as feed rate, conveyor speed, and pressure. The control systems also include safety features, such as emergency stop buttons and overload protection, to safeguard both operators and equipment from potential hazards. Additionally, the system is designed for flexibility, allowing for easy integration with other production equipment and customization to meet specific client requirements. For instance, the conveyor length and inclination can be adjusted to accommodate different production line layouts, and the system can be equipped with additional components like classifiers or separators to enhance material sorting and quality control. The energy efficiency of the system is another notable feature, with optimized motor and conveyor designs that reduce energy consumption while maintaining high performance. This not only lowers operational costs but also aligns with the industry's growing emphasis on sustainability and environmental responsibility.
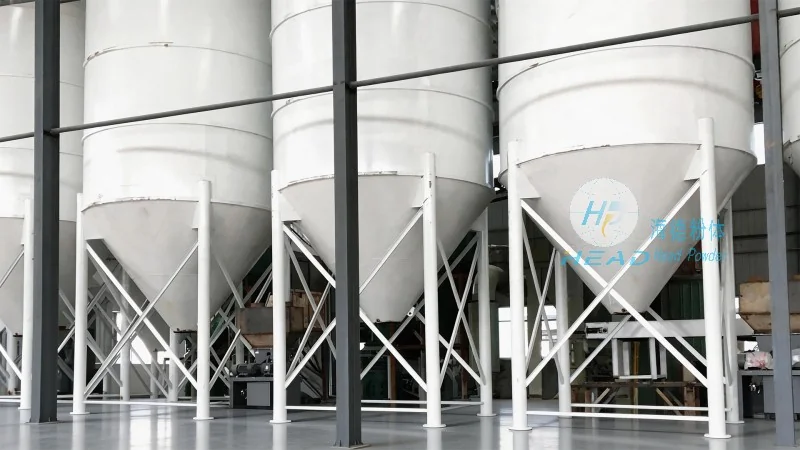
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a prominent manufacturer of pharmaceutical engineering solutions, is dedicated to providing innovative and reliable equipment for the pharmaceutical industry. With its base in Shandong, China, the company has built a strong reputation for excellence in product design, manufacturing, and customer service. HeadPowder specializes in developing customized solutions tailored to the unique needs of pharmaceutical manufacturers, focusing on enhancing production efficiency, improving product quality, and ensuring regulatory compliance. The company's team of experienced engineers and technicians work closely with clients to understand their specific challenges and develop tailored systems that address their requirements. HeadPowder's commitment to quality is evident in its adherence to international standards, including ISO 9001 for quality management and GMP guidelines for pharmaceutical equipment. The company continuously invests in research and development to stay ahead of technological advancements, incorporating the latest innovations in material handling, automation, and control systems into its products. By leveraging its expertise and state-of-the-art facilities, HeadPowder delivers systems that meet the highest standards of performance, reliability, and safety, helping pharmaceutical manufacturers achieve their operational goals and maintain a competitive edge in the global market.