

Working Principle and Features of a Stabilizer Powder Material Pneumatic Conveying System
For industries dealing with fine powders, especially those used as stabilizers in various applications, efficient and reliable material handling is crucial. The pneumatic conveying system, particularly designed for stabilizer powders, offers a solution that ensures minimal product degradation, consistent flow, and safe operation. This article explores the working principle and key features of such a system, highlighting its benefits and operational efficiency.
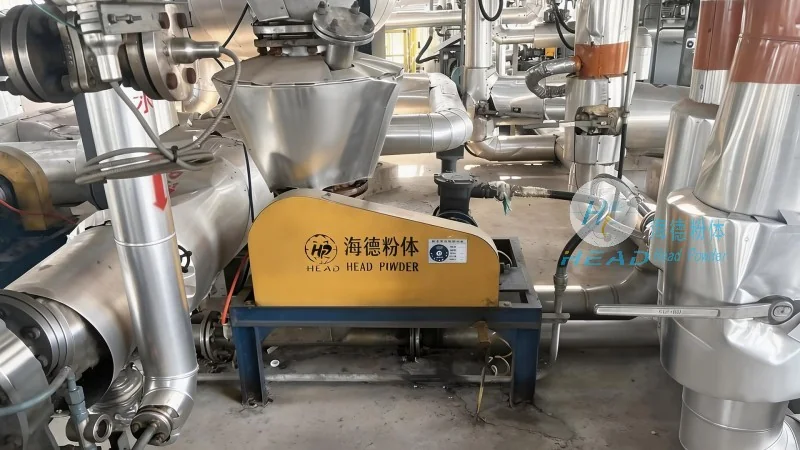
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer in the field of powder handling equipment, specializes in designing and supplying advanced pneumatic conveying systems tailored to the unique needs of industrial applications. With a strong presence in China, particularly in Shandong province, the company has built a reputation for delivering high-quality, durable, and efficient solutions for material transport. The expertise and innovation of HeadPowder have enabled them to cater to diverse industries, ensuring that their systems meet the stringent requirements of modern manufacturing processes.
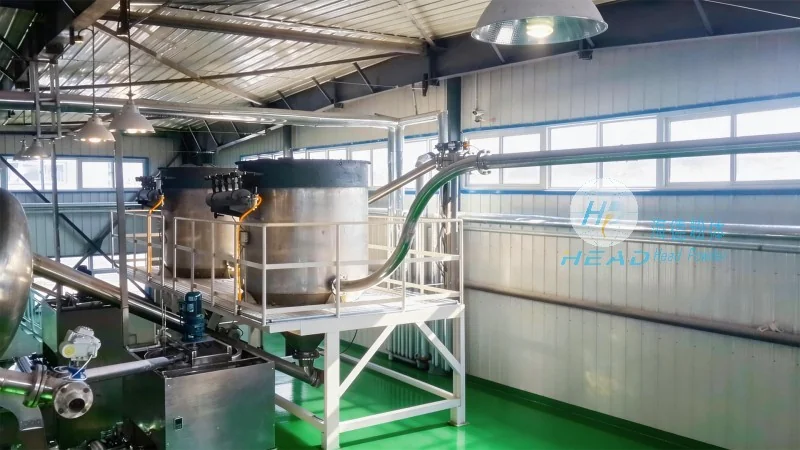
Working Principle of the Stabilizer Powder Pneumatic Conveying System
The core of a pneumatic conveying system for stabilizer powders lies in its ability to transport dry materials through a pipeline using air or other gases. The system typically operates on the principle of creating a pressure differential or using suction to move the material. In a pressure system, a blower or compressor generates positive pressure, pushing the material through the pipeline. Conversely, a suction system uses a vacuum to draw the powder from the source to the destination. For stabilizer powders, which are often sensitive to moisture and temperature changes, the system is designed to maintain optimal conditions throughout the transport process. The process begins with the material being fed into the hopper, where it is then drawn into the pipeline by the air flow. The air-powder mixture travels through the pipeline, with the air velocity maintained at a level sufficient to keep the powder suspended and prevent blockages. At the receiving end, the air is separated from the powder, often through a cyclone or filter, and the powder is collected in a storage bin or processing unit. This continuous flow ensures that the stabilizer powder is transported efficiently and without degradation, preserving its quality and performance.

Key Features and Advantages of the System
The pneumatic conveying system for stabilizer powders offers several distinct features that make it an ideal choice for industrial applications. Firstly, it provides a dust-free and enclosed transport process, which is critical for maintaining product purity and safety in the workplace. Unlike traditional belt or bucket elevators, the system eliminates the risk of dust exposure, reducing health hazards and environmental contamination. Secondly, the system is highly flexible in terms of layout and installation. It can be configured to fit various plant layouts, with the pipeline running horizontally, vertically, or at an angle, depending on the space constraints and operational requirements. This flexibility allows for seamless integration into existing production lines without major modifications. Thirdly, the system offers excellent control over the material flow rate and pressure, ensuring consistent and reliable transport. The adjustable air velocity and pressure settings allow operators to optimize the system for different powder types and quantities, minimizing energy consumption and maximizing efficiency. Additionally, the system is equipped with safety features such as pressure relief valves and overcurrent protection, ensuring safe operation and preventing accidents. The durability of the components, including the pipeline and fittings, is another key feature, as they are designed to withstand the abrasive nature of fine powders and the continuous operation required in industrial settings. The system also supports easy maintenance, with accessible components and simple cleaning procedures, reducing downtime and maintenance costs.
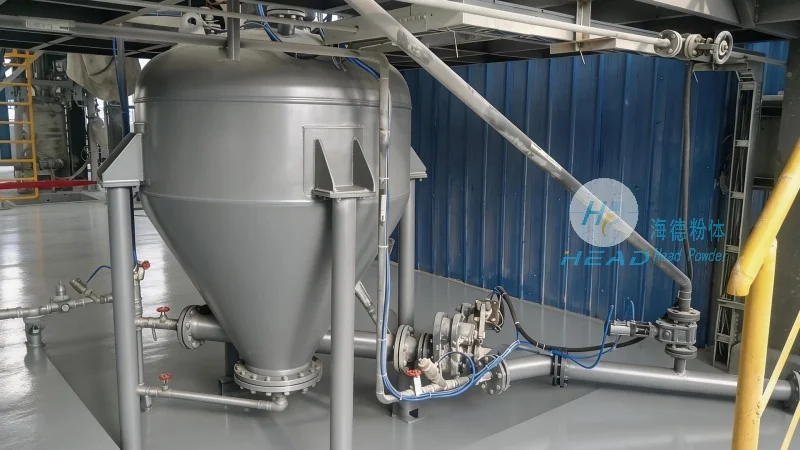
Applications and Industries Served
The pneumatic conveying system for stabilizer powders is widely used in various industries that rely on fine powders for their production processes. These include the chemical industry, where stabilizer powders are used as additives in polymer production; the food and beverage industry, where they are used as stabilizers in dairy products and beverages; the pharmaceutical industry, where they are used as excipients in drug formulations; and the construction industry, where they are used as additives in concrete and mortar. The system's ability to handle these diverse applications while maintaining product quality makes it a preferred choice for manufacturers in these sectors. By ensuring efficient and safe transport of stabilizer powders, the system contributes to improved productivity and reduced operational costs, making it a valuable asset for any industrial operation.