

Principle and Working Scene Characteristics of Tonne Bag Unloading Powder Conveying System Equipment
HeadPowder, a leading enterprise in the field of powder handling technology, specializes in the design, manufacturing, and supply of advanced tonne bag unloading powder conveying systems. Based in Shandong, China, the company has established itself as a reliable partner for industries requiring efficient and reliable bulk powder handling solutions.
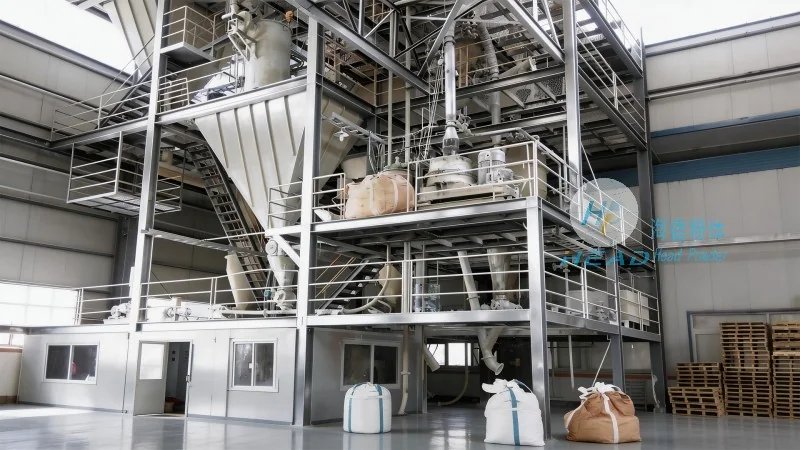
Introduction to Tonne Bag Unloading Powder Conveying Systems
At the core of many industrial processes, the efficient transfer of bulk powders from storage containers to processing equipment is crucial for maintaining productivity and product quality. Tonne bag unloading powder conveying systems address this need by providing a seamless, automated solution for handling large volumes of powders. These systems are engineered to handle the challenges associated with unloading heavy-duty bags, such as those used in the chemical, food, and pharmaceutical industries, ensuring minimal dust generation and optimal material flow.
Principle of Operation
The tonne bag unloading powder conveying system operates on a principle of mechanical and pneumatic integration. The process typically begins with the placement of a tonne bag onto a loading platform. A mechanical lifting mechanism then lifts the bag, while a pneumatic valve or airlock system opens to allow the powder to flow into a hopper or silo. The system may incorporate a combination of vacuum or pressure-assisted conveying to ensure consistent material movement. Key components include the bag opening mechanism, the hopper with integrated filters, and the conveying pipeline, all designed to work in harmony to achieve a continuous and controlled flow of powder. The design emphasizes energy efficiency and low maintenance, making it suitable for long-term industrial use.
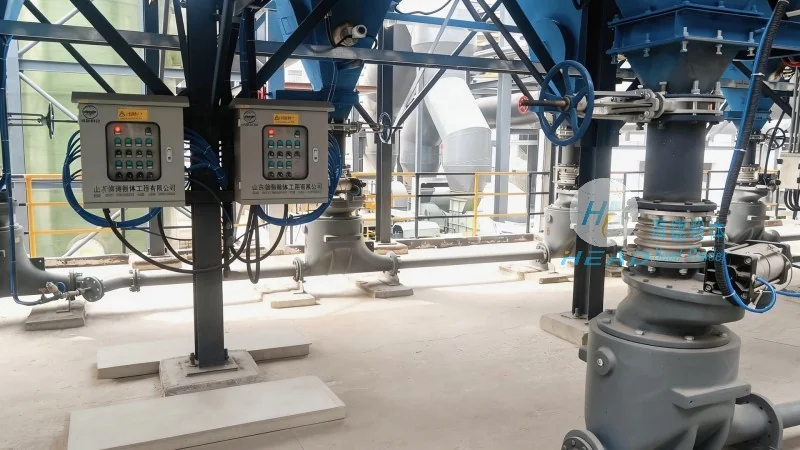
Working Scene Characteristics
The working scene characteristics of these systems are tailored to meet the diverse demands of industrial applications. In chemical plants, for instance, the system must handle a wide range of powders, from fine chemicals to bulk raw materials, while maintaining strict safety and contamination control. The food industry requires systems that are hygienic, easy to clean, and compliant with food safety regulations. Pharmaceutical applications demand high-purity handling, with features like HEPA filters and sterile processing to prevent cross-contamination. The versatility of the tonne bag unloading system allows it to adapt to various working environments, whether in a large-scale manufacturing facility or a smaller processing plant. The system's ability to handle different bag sizes and materials further enhances its adaptability, making it a flexible solution for various operational needs.
Key Features and Advantages
HeadPowder's tonne bag unloading powder conveying systems are equipped with several features that enhance their performance and reliability. These include automatic bag opening and closing mechanisms, which reduce manual labor and improve safety. The integrated dust collection and filtration systems ensure that the working environment remains clean and compliant with environmental regulations. The system's modular design allows for easy installation and maintenance, with components that can be replaced or upgraded as needed. Additionally, the use of high-quality materials and robust construction ensures durability and long service life. The energy-efficient design minimizes operational costs, making it a cost-effective solution for industries looking to optimize their powder handling processes.
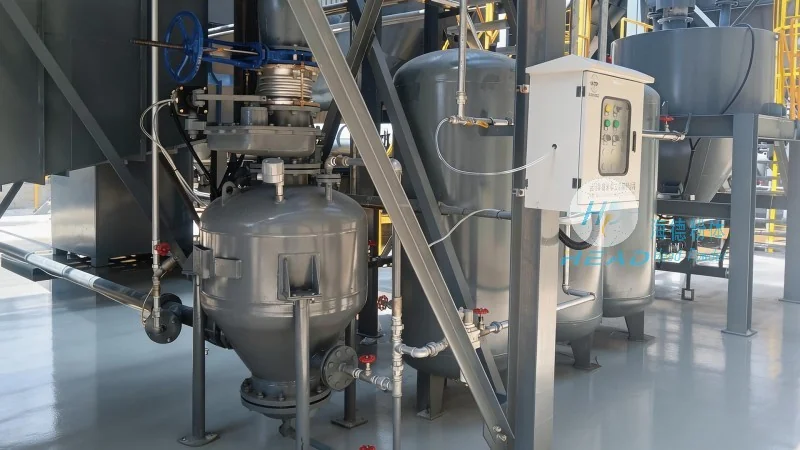
Application Scenarios
The applications of tonne bag unloading powder conveying systems span across multiple industries. In the chemical industry, these systems are used to handle raw materials such as limestone, gypsum, and various chemical powders, facilitating their transfer to reactors and processing units. In the food and beverage sector, they are employed to handle ingredients like flour, sugar, and spices, ensuring a consistent supply for production lines. The pharmaceutical industry utilizes these systems for the handling of active pharmaceutical ingredients (APIs) and excipients, maintaining the purity and integrity of the materials. Additionally, in the agricultural sector, the systems are used to handle fertilizers and other bulk agricultural products, supporting efficient farming operations. Each application leverages the system's ability to handle large volumes and maintain material quality, contributing to overall operational efficiency.
Conclusion
HeadPowder's tonne bag unloading powder conveying systems represent a sophisticated solution for the efficient handling of bulk powders. By integrating mechanical and pneumatic technologies, these systems provide a reliable, safe, and cost-effective method for unloading and conveying powders in various industrial settings. With a focus on durability, adaptability, and compliance with industry standards, HeadPowder continues to be a trusted provider of powder handling equipment. The company's commitment to innovation and customer satisfaction ensures that its systems meet the evolving needs of modern industries, supporting productivity and quality in bulk material processing.