

Principles and Application Scenarios of Dust-Free Material Feeding and Conveying Systems
HeadPowder, a leading provider of industrial material handling solutions, specializes in dust-free material feeding and conveying systems. These systems are designed to ensure the safe and efficient transfer of powders and bulk materials while maintaining a clean environment, which is critical in industries such as pharmaceuticals, food processing, and electronics manufacturing. The core principle behind these systems lies in the integration of advanced sealing technologies and controlled airflow to prevent particle contamination and cross-contamination.
The Fundamental Principles of Dust-Free Material Feeding
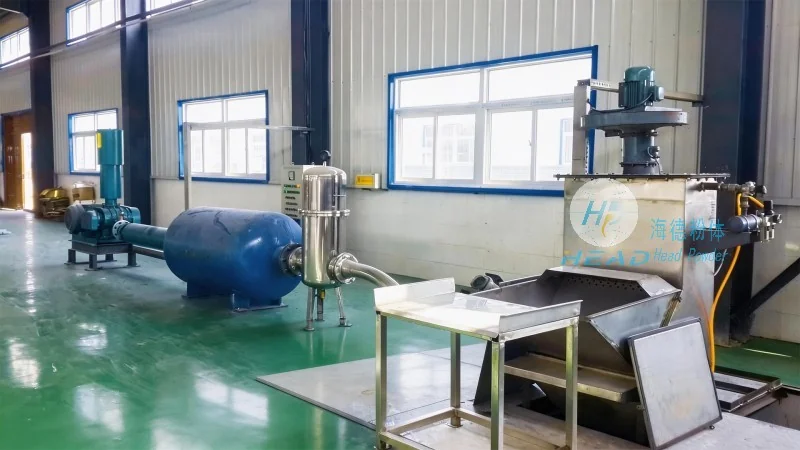
The operation of dust-free material feeding systems is based on several key principles that ensure minimal particle release and optimal material handling. First, the system employs airtight enclosures and sealed transfer points to contain dust and prevent it from entering the surrounding environment. This is achieved through the use of high-quality seals, such as O-rings and gaskets, which create a barrier between the material and the external air. Second, the system utilizes controlled airflow, often in a negative pressure or positive pressure mode, to maintain a stable air pressure within the system. In negative pressure systems, the enclosure is kept at a lower pressure than the surrounding environment, drawing air and particles out through designated exhaust points. Conversely, positive pressure systems maintain a higher pressure inside the enclosure, preventing external air from entering and carrying contaminants into the system.
Key Working Characteristics of Dust-Free Material Feeding Systems
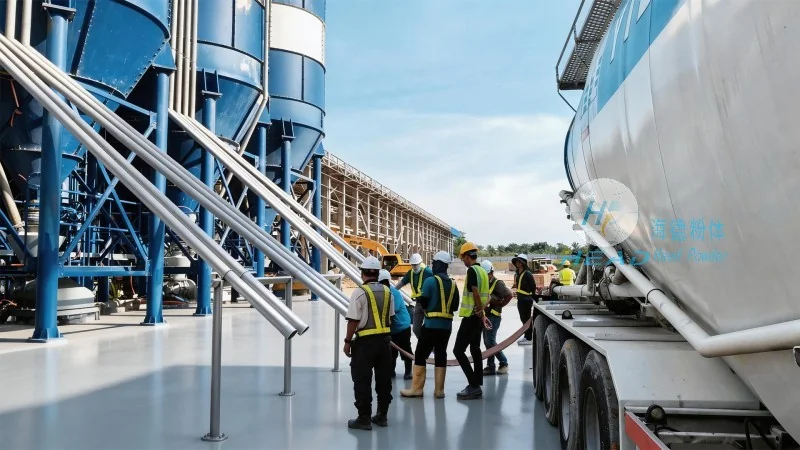
Several working characteristics define the effectiveness and reliability of dust-free material feeding systems. One of the most important is the ability to handle a wide range of materials, from fine powders to bulk solids, without compromising the integrity of the material or the cleanliness of the environment. This is achieved through adjustable feeding mechanisms, such as screw conveyors, vibratory feeders, and rotary valves, which can be customized to match the specific properties of the material being handled. Another critical characteristic is the system's ability to maintain consistent material flow rates, which is essential for maintaining production efficiency and preventing material buildup or clogging. Additionally, the systems are designed to be easy to clean and maintain, with removable components and easy access to internal parts, which helps to minimize downtime and ensure long-term performance.
Common Application Scenarios in Industrial Settings
Dust-free material feeding systems are widely used in various industrial settings where maintaining a clean and controlled environment is paramount. In the pharmaceutical industry, these systems are used to handle active pharmaceutical ingredients (APIs) and excipients, ensuring that the final product remains free from contaminants and meets stringent regulatory standards. In the food processing industry, they are used to handle ingredients such as flour, sugar, and spices, maintaining the quality and safety of the food products. In the electronics manufacturing industry, they are used to handle sensitive components and materials, preventing dust and particles from damaging delicate equipment and affecting product performance. Other applications include the chemical industry, where they are used to handle hazardous powders, and the cosmetics industry, where they are used to handle raw materials for beauty products.
About HeadPowder Engineering
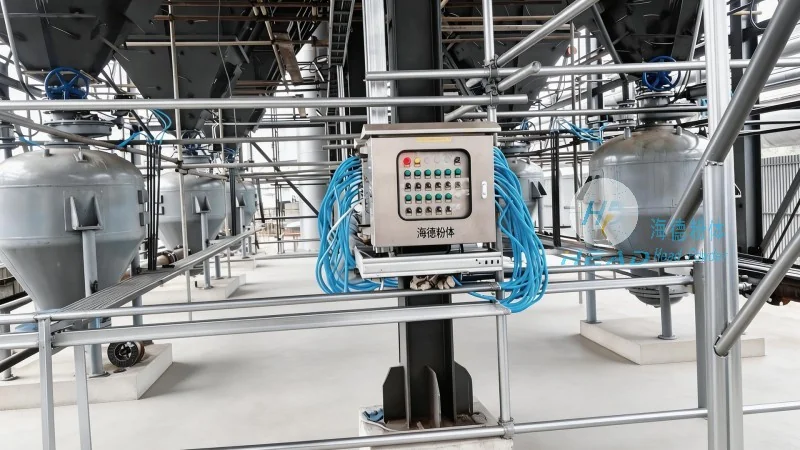
HeadPowder Engineering Co., Ltd., headquartered in Shandong, China, is a professional manufacturer and supplier of industrial material handling equipment. With years of experience in the field, HeadPowder has developed a comprehensive range of dust-free material feeding and conveying systems that meet the diverse needs of various industries. The company's products are designed to be reliable, efficient, and easy to maintain, ensuring that customers can achieve optimal performance and minimize operational costs. HeadPowder is committed to providing high-quality solutions that help its clients maintain a clean and safe working environment while improving production efficiency.