

Principle and Working Scene Characteristics of Calcium Carbonate Stone Powder Material Conveying Lin
Calcium carbonate stone powder is a widely used material in various industrial applications, and the efficient transportation of this fine powder is crucial for maintaining production efficiency and product quality. The material conveying line for calcium carbonate stone powder involves specialized equipment and systems designed to handle the unique properties of this material, such as its fine particle size, low bulk density, and potential for dust generation. Understanding the principle and working scene characteristics of these conveying lines is essential for industries that rely on calcium carbonate in their manufacturing processes.
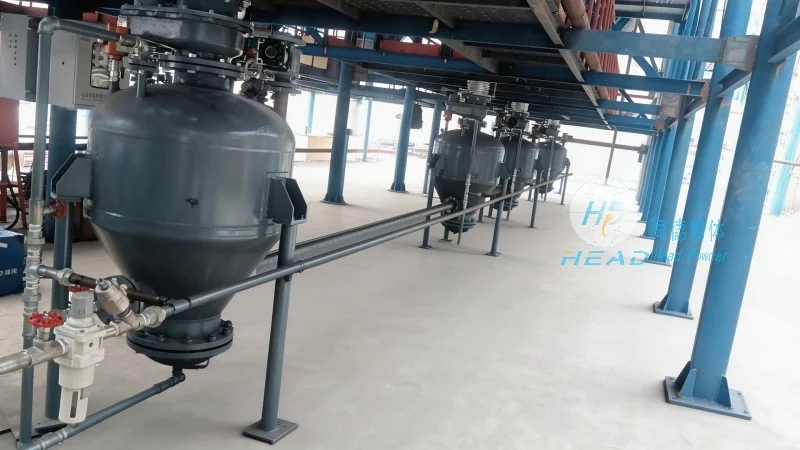
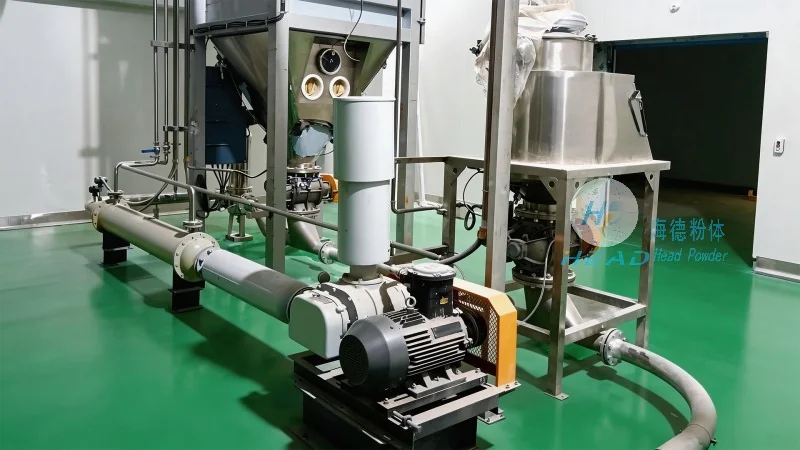
Principle of Material Conveying Systems for Calcium Carbonate Stone Powder
The core principle of calcium carbonate stone powder material conveying lines is to transport the fine powder from a source, such as a storage silo or a processing unit, to a destination, like a processing machine or a packaging area. The conveying systems typically utilize mechanical or pneumatic methods to move the material. Mechanical conveying, often through belt conveyors or screw conveyors, is commonly used for bulk material handling due to its reliability and cost-effectiveness. Pneumatic conveying, on the other hand, uses air pressure to transport the powder through a pipeline, which is ideal for applications requiring dust-free and controlled delivery. The choice of conveying method depends on factors like the material's characteristics, the distance to be covered, and the required flow rate. For calcium carbonate stone powder, which is often sensitive to moisture and can cause blockages if not handled properly, the design of the conveying system must ensure minimal friction, proper air flow, and effective dust control measures.
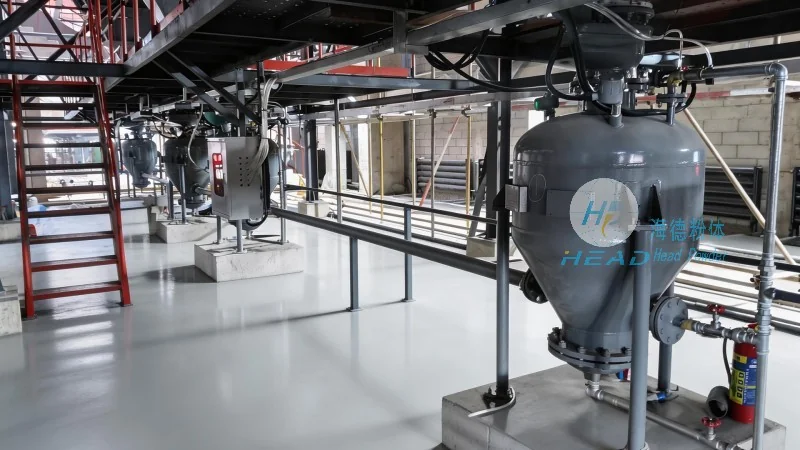
Working Scene Characteristics and Applications
The working scene characteristics of calcium carbonate stone powder material conveying lines vary significantly based on the specific industrial application. In the paper and plastic industries, for example, calcium carbonate is used as a filler to enhance the strength and whiteness of products. The conveying lines in these settings must be capable of handling large volumes of fine powder and integrating with existing production lines without disrupting operations. In the construction industry, calcium carbonate is used as a raw material for cement and concrete, and the conveying systems must be robust enough to handle the material's abrasive properties and ensure consistent flow rates. Additionally, the working environment may involve high temperatures or exposure to chemicals, requiring the conveying equipment to be made of corrosion-resistant materials. The characteristics of the working scene also include the need for dust suppression and environmental compliance, as calcium carbonate dust can be a health hazard if not properly contained. Therefore, the design of the conveying line must incorporate features like dust collection systems and sealed enclosures to maintain a safe and clean working environment.
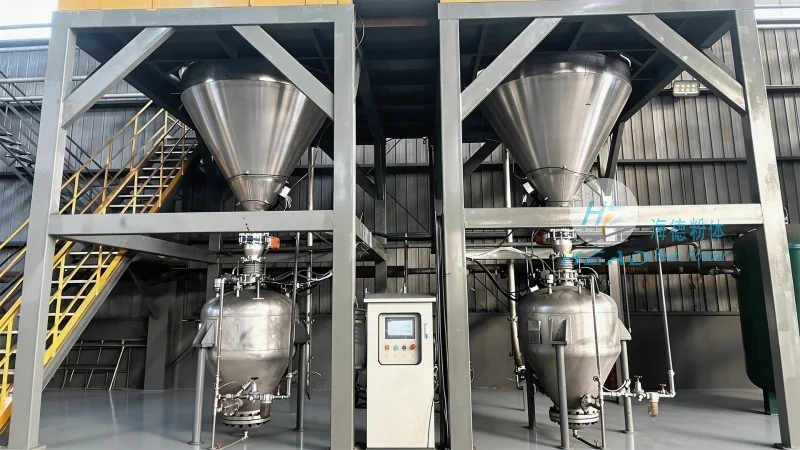
Company Profile and Technical Expertise
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading provider of specialized material handling solutions for industries that use calcium carbonate stone powder. With a strong focus on engineering innovation and customer-centric design, headpowder has developed advanced conveying systems tailored to the unique challenges of handling fine powders. The company's expertise lies in understanding the material's properties and designing conveying lines that optimize efficiency, reduce downtime, and ensure product integrity. Headpowder's team of engineers and technicians work closely with clients to assess their specific needs and provide customized solutions, from initial design and installation to ongoing maintenance and support. Based in Shandong, China, headpowder leverages its local manufacturing capabilities and extensive industry experience to deliver high-quality, reliable material conveying systems that meet international standards. The company's commitment to quality and customer satisfaction has established it as a trusted partner for businesses seeking to enhance their material handling processes and improve overall operational performance.