

Principle and Working Scene Characteristics of Pneumatic Conveying Systems for Coal Particle Materia
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and implementation of advanced pneumatic conveying systems tailored for coal particle materials. These systems represent a sophisticated approach to material handling, offering efficient and reliable solutions for transporting coal in various industrial applications. The following discussion explores the fundamental principles behind these systems and highlights the key characteristics of their operational environments.
The Principle of Pneumatic Conveying Systems
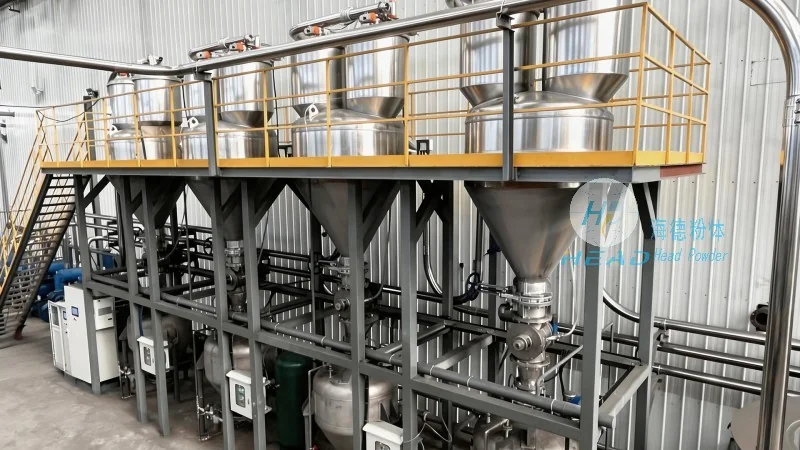
Pneumatic conveying systems operate on the principle of using compressed air or gas to transport bulk materials, such as coal particles, through a pipeline. The system typically consists of a hopper for material storage, a feeder to control the flow rate, a conveying line, and a receiver for the discharged material. The core mechanism involves creating a pressure differential within the pipeline, where air is introduced to generate a flow that carries the coal particles along. This method eliminates the need for mechanical components like belts or buckets, reducing maintenance and increasing operational efficiency. The system can be categorized into two main types: dilute-phase and dense-phase, each offering distinct advantages depending on the material characteristics and transport distance.
Working Scene Characteristics
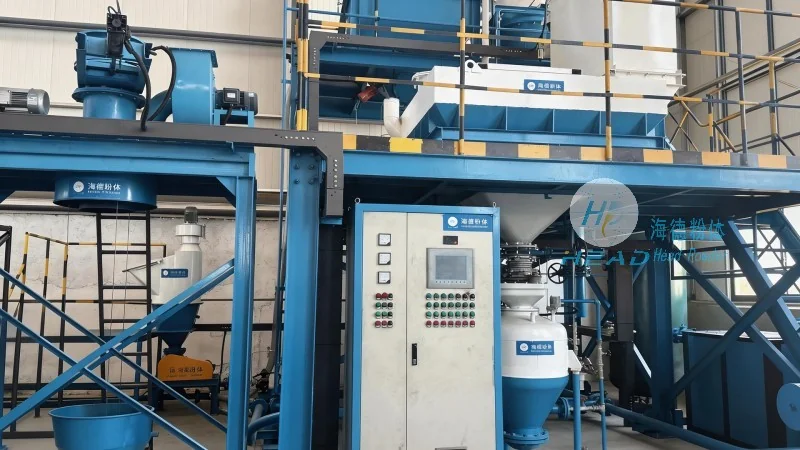
The operational environment of pneumatic conveying systems for coal particles is characterized by several key factors that influence system design and performance. Firstly, the particle size and density of coal play a crucial role in determining the appropriate conveying velocity and pressure. Larger or denser particles may require higher air velocities to ensure proper suspension and transport. Secondly, the distance and layout of the conveying line affect the system's pressure requirements and energy consumption. Longer or more complex layouts may necessitate additional boosters or larger compressor capacity to maintain effective transport. Additionally, the system's integration with existing industrial processes, such as coal storage and processing facilities, requires careful consideration of space constraints and compatibility with other equipment. The working environment also includes considerations for dust control and safety measures, as coal dust can pose health and safety risks in industrial settings. Proper sealing and filtration systems are essential to maintain air quality and prevent dust emissions.

System Advantages and Applications
Pneumatic conveying systems for coal particle materials offer several advantages over traditional mechanical handling methods. These include reduced labor costs due to automated operation, lower maintenance requirements as there are fewer moving parts, and increased safety by minimizing direct human contact with the material. The systems are also highly flexible, allowing for changes in material flow rates and line configurations without significant modifications. In industrial settings, these systems are commonly used in coal mines, power plants, and processing facilities where coal needs to be transported from storage to processing units or between different stages of production. The efficiency and reliability of pneumatic conveying make it an ideal solution for continuous and high-volume material handling, ensuring consistent performance even under varying operational conditions.
Conclusion and Company Expertise
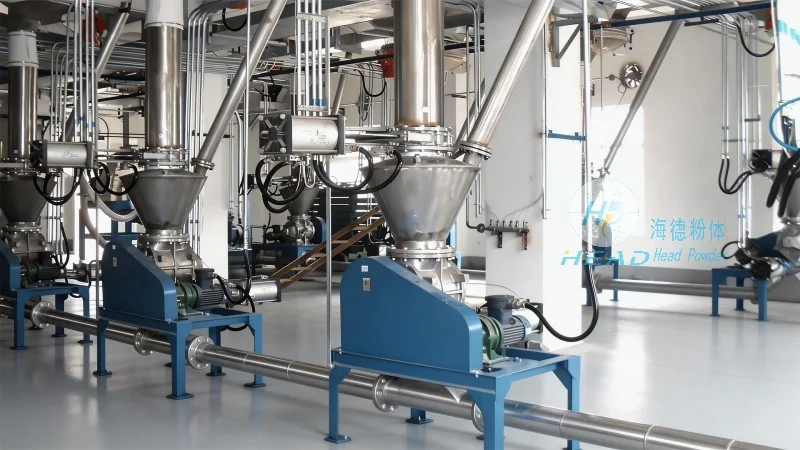
HeadPowder Engineering Co., Ltd., with its headquarters in Shandong, China, leverages decades of experience in engineering and material handling to provide customized pneumatic conveying solutions for coal particle applications. By understanding the unique characteristics of coal and the specific requirements of each industrial site, the company designs systems that optimize performance, reduce operational costs, and enhance safety. The company's commitment to innovation and quality ensures that its clients receive reliable and efficient solutions tailored to their needs. Whether for new installations or system upgrades, HeadPowder remains a trusted partner in the implementation of advanced material handling technologies for coal particle materials.