

Principle and Working Scene Characteristics of Pneumatic Conveying Machine for Organic Fertilizer Gr
HeadPowder, a leading enterprise in pneumatic conveying technology, specializes in designing and manufacturing advanced equipment for transporting organic fertilizer granular materials. Headquartered in Shandong, China, the company has positioned itself as a trusted partner for clients seeking efficient and reliable material handling solutions. This article explores the core principles and working scene characteristics of the organic fertilizer granular materials pneumatic conveying machine, highlighting its technical advantages and practical applications.
Organic Fertilizer Granular Materials Pneumatic Conveying Machine: An Overview
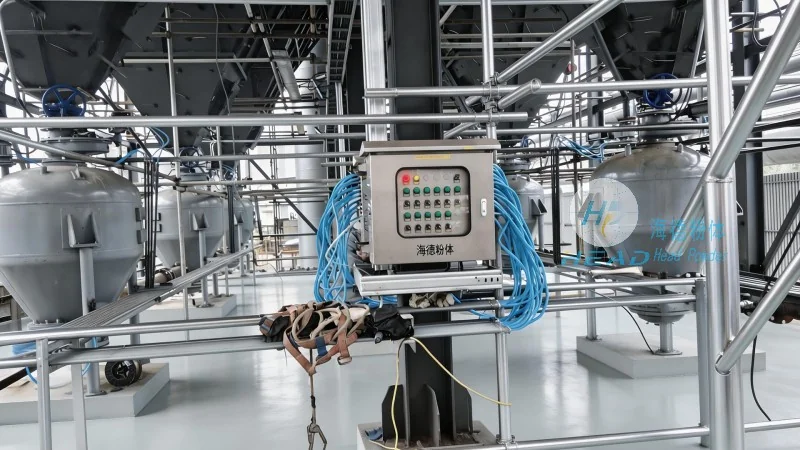
The organic fertilizer granular materials pneumatic conveying machine is a specialized device engineered to transport organic fertilizer granules through an air-driven system. This equipment is designed to handle the unique properties of organic fertilizer, such as bulk density, moisture content, and potential dust generation, ensuring safe and efficient material movement. The machine operates by utilizing a combination of air pressure and vacuum to move the granular material from the source to the destination, eliminating the need for traditional mechanical conveyors that may cause material degradation or contamination.
Principle of Pneumatic Conveying Technology
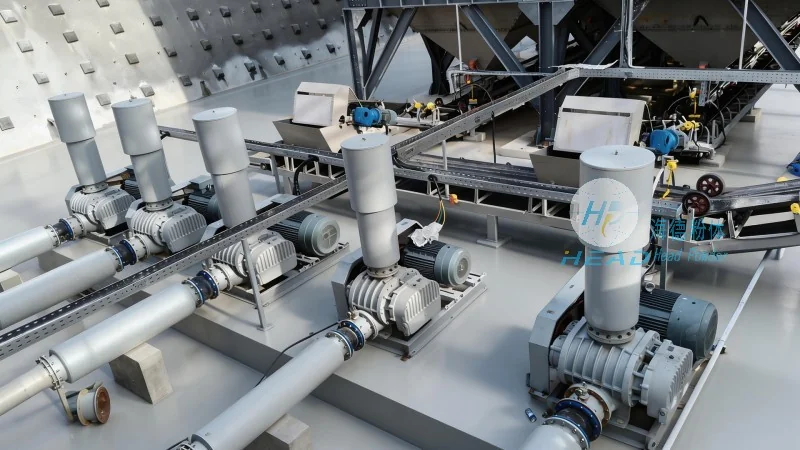
The fundamental principle behind the pneumatic conveying machine is the use of air as the conveying medium. The system typically consists of a blower or compressor that generates airflow, a hopper for material storage, a conveying line, and a discharge point. When the machine is activated, air is introduced into the hopper, creating a pressure differential that lifts the organic fertilizer granules into the conveying line. The material is then carried through the pipeline by the moving air stream, reaching the discharge point where it is released. This process is highly efficient, as it minimizes material handling time and reduces the risk of product loss or degradation.
Working Scene Characteristics and Applications
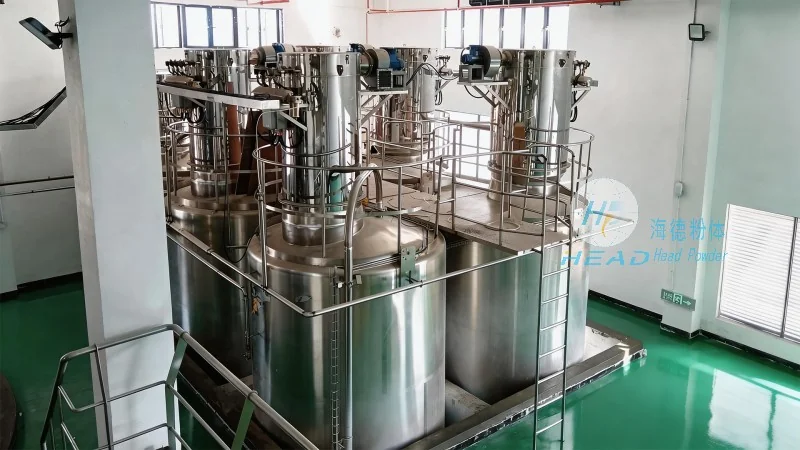
The organic fertilizer granular materials pneumatic conveying machine is particularly suited for various working scenes, including fertilizer production plants, storage facilities, and distribution centers. In fertilizer production, the machine is used to transport raw organic materials from storage silos to processing units, ensuring a continuous and clean flow of material. In storage facilities, it facilitates the transfer of finished organic fertilizer products from storage silos to loading areas, enhancing operational efficiency. The machine's ability to handle large volumes of granular material with minimal maintenance makes it an ideal choice for industrial applications where reliability and productivity are paramount.
Technical Advantages and Performance Metrics
HeadPowder's organic fertilizer granular materials pneumatic conveying machine offers several technical advantages that set it apart from conventional conveying methods. The machine is designed to handle a wide range of organic fertilizer types, including compost, manure, and other organic byproducts, with minimal impact on material quality. The air-driven system reduces mechanical wear and tear, leading to lower maintenance costs and longer equipment lifespan. Additionally, the machine's ability to operate in both positive and negative pressure modes allows for flexible application in different working environments, ensuring adaptability to various production and storage scenarios.
Customization and Integration with Existing Systems
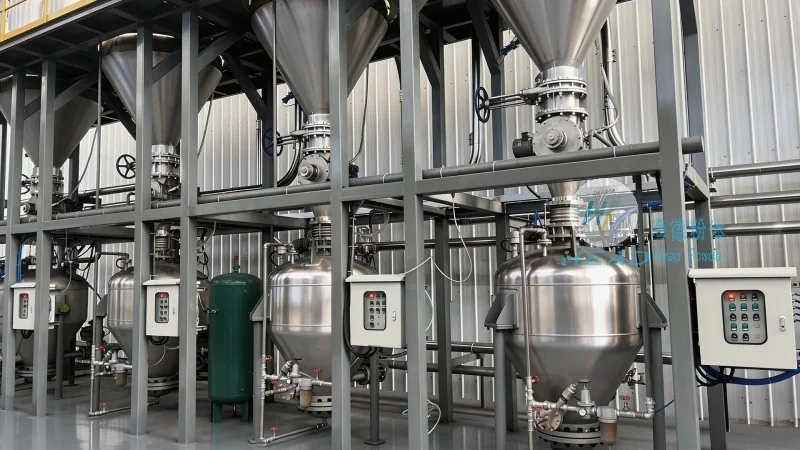
HeadPowder provides customized solutions tailored to the specific needs of clients, ensuring that the organic fertilizer granular materials pneumatic conveying machine integrates seamlessly with existing production and storage systems. The company's engineering team works closely with clients to assess their operational requirements, material characteristics, and space constraints, developing a tailored solution that maximizes efficiency and minimizes downtime. Customization options may include adjustments to the conveying line diameter, air pressure settings, and material hopper capacity, ensuring that the equipment meets the unique demands of each application.
Conclusion: Enhancing Efficiency in Organic Fertilizer Handling
In conclusion, the organic fertilizer granular materials pneumatic conveying machine from HeadPowder represents a significant advancement in material handling technology for the organic fertilizer industry. By leveraging pneumatic conveying principles, the machine offers efficient, reliable, and cost-effective solutions for transporting organic fertilizer granules. With its headquarters in Shandong, China, HeadPowder continues to innovate and provide high-quality equipment that meets the evolving needs of the fertilizer sector, contributing to improved operational efficiency and sustainability in material handling processes.