

Classification and Composition of Coal Ash Particle Pneumatic Conveying Systems
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a professional manufacturer specializing in the design, production, and supply of pneumatic conveying systems for various industrial applications. The company is located in Shandong, China, and has established itself as a reliable partner in the field of material handling solutions.
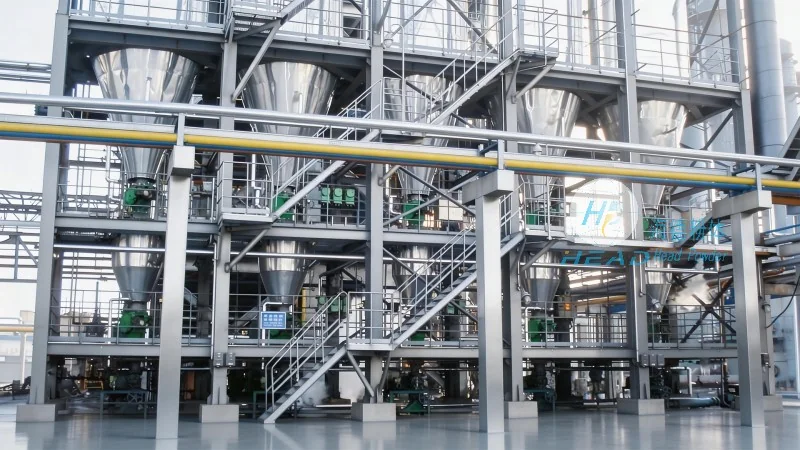
Classification of Coal Ash Particle Pneumatic Conveying Systems
Pneumatic conveying systems for coal ash particles are typically classified based on the pressure and flow characteristics of the conveying medium. The primary categories include low-pressure, medium-pressure, and high-pressure systems. Low-pressure systems operate at pressures below 0.1 MPa and are suitable for short-distance conveying with low particle loadings. Medium-pressure systems operate between 0.1 MPa and 0.5 MPa, offering a balance between energy efficiency and conveying capacity. High-pressure systems operate above 0.5 MPa, providing high conveying speeds and the ability to handle larger particle sizes and higher loadings. The choice of system type depends on factors such as the distance to be covered, the volume of material to be conveyed, and the specific characteristics of the coal ash particles.
Composition of Coal Ash Particle Pneumatic Conveying Systems
A typical coal ash particle pneumatic conveying system consists of several key components that work together to ensure efficient and reliable material transport. The main components include a material feeder, a conveying pipeline, a blower or compressor, a dust separator, and a discharge device. The material feeder is responsible for feeding the coal ash particles into the system at a controlled rate, ensuring a consistent flow. The conveying pipeline is designed to withstand the pressure and temperature conditions of the system and is typically made of materials such as stainless steel or plastic. The blower or compressor provides the necessary air or gas pressure to move the particles through the pipeline. The dust separator is used to remove any fine particles or dust from the conveying air, improving air quality and preventing contamination. The discharge device is responsible for releasing the coal ash particles from the system at the destination point, such as a storage silo or processing unit.
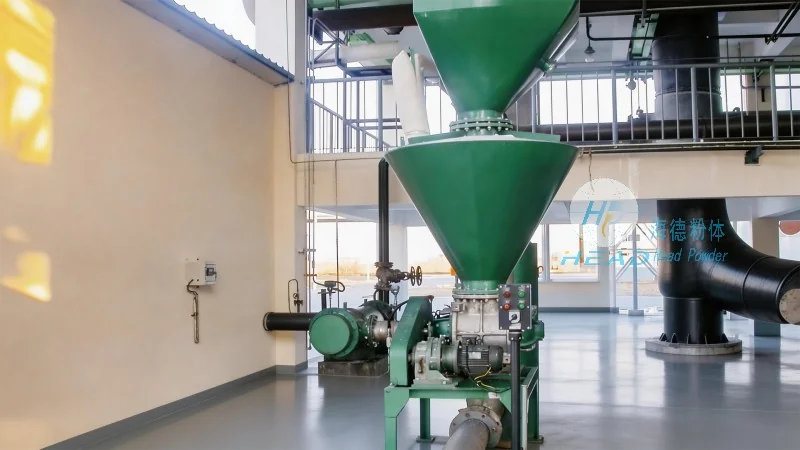
Key Features and Benefits
Coal ash particle pneumatic conveying systems from headpowder are engineered to deliver superior performance and durability. These systems are designed to handle the abrasive and corrosive nature of coal ash particles, ensuring long-term reliability. The use of high-quality materials and advanced manufacturing processes minimizes maintenance requirements and reduces downtime. Additionally, the systems are equipped with advanced control systems that allow for precise regulation of the conveying process, optimizing energy consumption and material flow. The result is a cost-effective solution that enhances operational efficiency and reduces environmental impact by minimizing dust emissions.
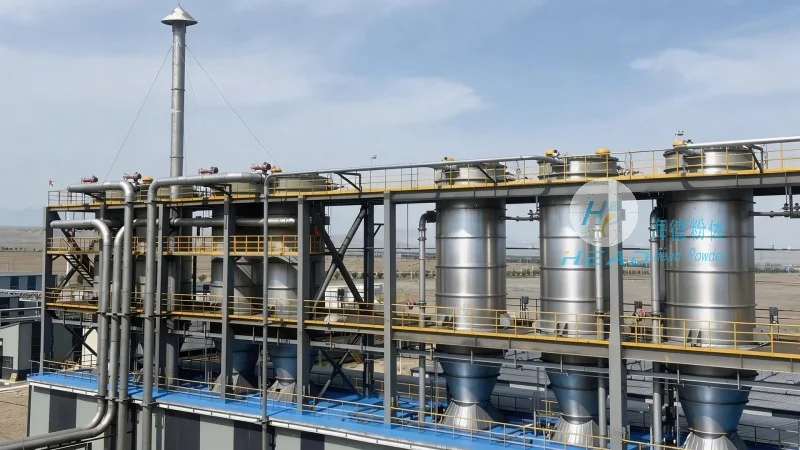
Applications and Industry Use
The coal ash particle pneumatic conveying systems are widely used in various industrial sectors, including power plants, cement production, and waste management facilities. In power plants, these systems are used to transport coal ash from the boiler to storage silos or for further processing. In cement plants, they facilitate the handling of raw materials and finished products, improving overall production efficiency. The systems are also utilized in waste management to transport ash from incineration plants to disposal sites or for recycling purposes. The versatility and adaptability of the systems make them suitable for a wide range of applications, providing customized solutions to meet specific industry needs.
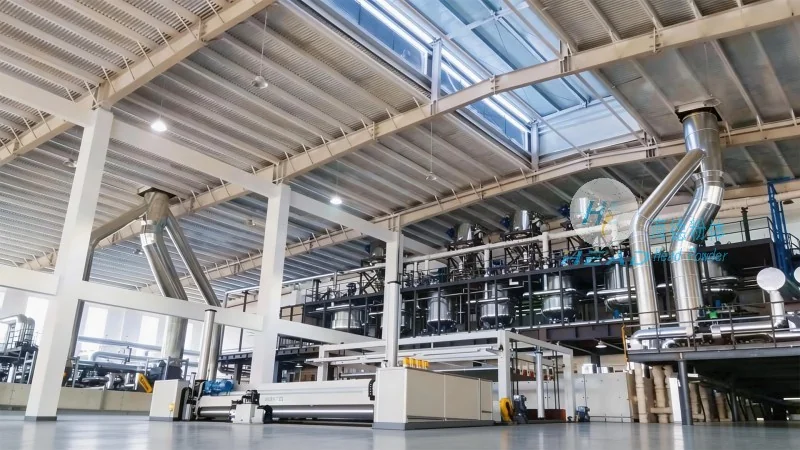
Technical Specifications and Customization
headpowder offers a range of technical specifications and customization options to suit diverse operational requirements. The systems can be tailored to handle different particle sizes, moisture contents, and flow rates. The conveying capacity can be adjusted from small volumes for laboratory or pilot-scale operations to large-scale industrial applications. The pressure and flow rates are configurable to match the specific distance and elevation changes of the conveying route. Additionally, the systems can be integrated with existing infrastructure or designed as standalone units, providing flexibility in installation and operation. The company's engineering team works closely with clients to develop customized solutions that meet their unique operational challenges and performance goals.
Quality Assurance and Service
Shandong HeadPowder Engineering Co., Ltd. adheres to strict quality control standards throughout the design, manufacturing, and installation process. All components are manufactured using high-quality materials and undergo rigorous testing to ensure compliance with industry standards. The company provides comprehensive after-sales service, including installation, commissioning, and maintenance support. Technical support is available to assist with system operation and troubleshooting, ensuring optimal performance and minimal downtime. By prioritizing quality and customer service, headpowder aims to build long-term partnerships with clients and deliver reliable, efficient material handling solutions.