

Long-Distance Pneumatic Conveying System for Rice Husk Powder
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and implementation of advanced pneumatic conveying systems tailored for the efficient transport of rice husk powder over long distances. This article provides an in-depth look at the technical aspects, operational benefits, and practical applications of such systems, highlighting how they address the unique challenges associated with handling fine, lightweight powders like rice husk powder.
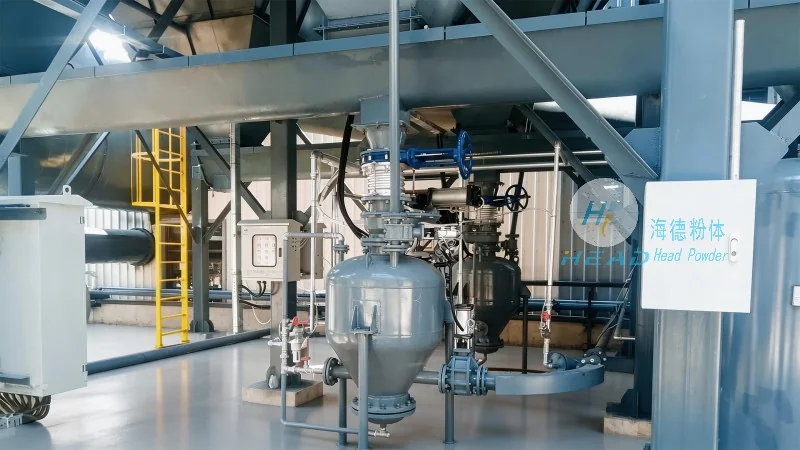
Introduction to Pneumatic Conveying Systems for Rice Husk Powder
Pneumatic conveying systems offer a reliable and efficient method for transporting bulk materials, including rice husk powder, from one location to another without the need for mechanical components like belts or buckets. These systems utilize compressed air to move the material through a pipeline network, making them ideal for applications where traditional conveying methods may be impractical or inefficient. The long-distance pneumatic conveying system for rice husk powder, developed by HeadPowder, is engineered to handle the specific properties of rice husk powder, such as its fine particle size, low bulk density, and tendency to create dust, ensuring optimal performance and minimal material loss.
Key Features and Technical Specifications
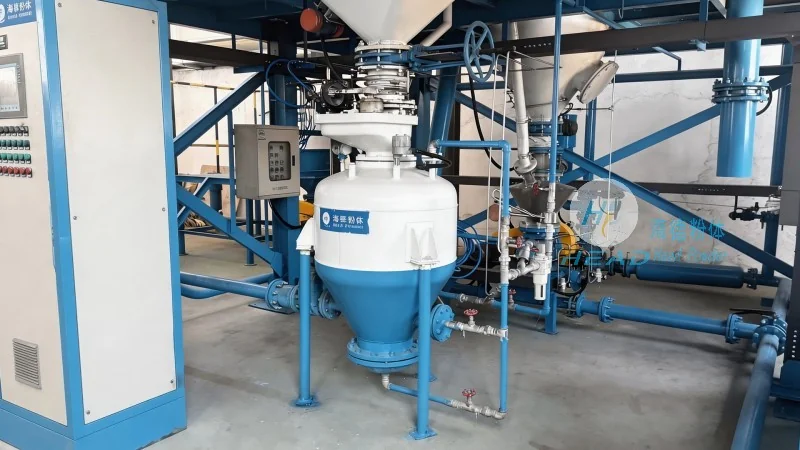
The long-distance pneumatic conveying system for rice husk powder from HeadPowder incorporates several key features that enhance its performance and reliability. One of the primary components is the air compressor, which generates the necessary pressure to move the material through the pipeline. The system is equipped with high-efficiency filters to maintain air quality and prevent dust accumulation, which is crucial for maintaining the purity of the rice husk powder. Additionally, the pipeline design includes appropriate bends and fittings to minimize pressure drop and ensure smooth material flow. The system also features a control panel that allows for real-time monitoring and adjustment of operational parameters, such as air pressure and flow rate, to optimize performance and prevent system overload.
Operational Benefits and Efficiency
Implementing a long-distance pneumatic conveying system for rice husk powder provides numerous operational benefits for industrial applications. One of the most significant advantages is the reduction in material handling costs, as the system eliminates the need for manual labor and reduces the risk of material loss during transport. The system also minimizes the risk of contamination, as the enclosed pipeline design prevents exposure to external elements and dust. Furthermore, the system's ability to handle fine particles without clogging or blockages ensures consistent and reliable material flow, which is essential for maintaining production efficiency. The long-distance capability of the system allows for seamless integration with existing production lines, enabling companies to expand their operations without the need for additional infrastructure.
Application Examples and Case Studies
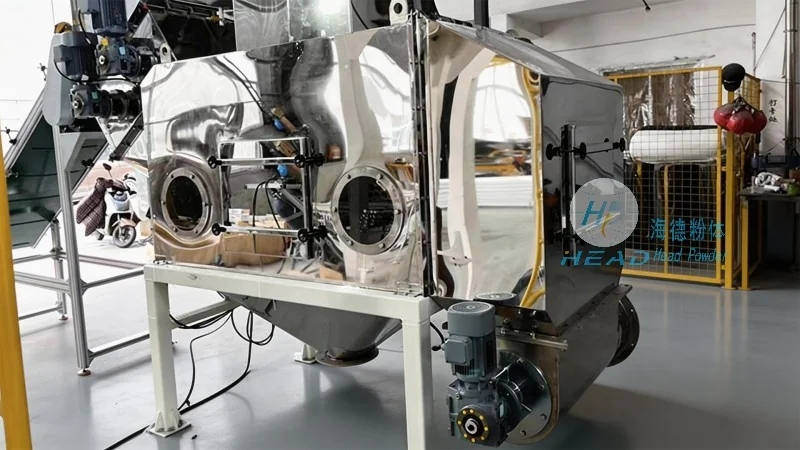
The long-distance pneumatic conveying system for rice husk powder has been successfully implemented in various industrial applications, including power generation, biofuel production, and agricultural processing. For example, in a power plant, the system was used to transport rice husk powder from a storage silo to a boiler, where it is used as a fuel source. The system's ability to handle the fine particle size of the rice husk powder and maintain consistent flow ensured that the boiler operated efficiently, reducing fuel costs and improving overall plant performance. In another application, the system was used in a biofuel plant to transport rice husk powder to a pelletizing machine, where it is converted into biomass pellets for use as a renewable energy source. The system's reliability and efficiency in these applications have demonstrated its effectiveness in meeting the demands of modern industrial processes.
Maintenance and Longevity
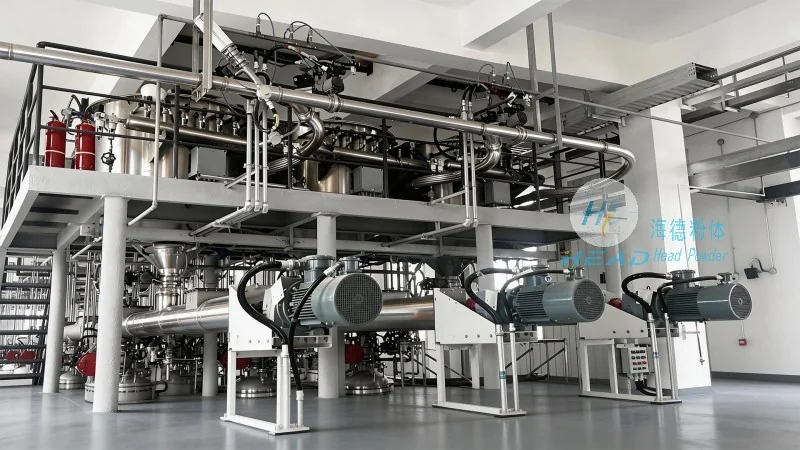
Maintaining the long-distance pneumatic conveying system for rice husk powder is essential to ensure its longevity and continued performance. Regular maintenance procedures include cleaning the air filters, checking the pipeline for blockages or leaks, and inspecting the compressor and control panel for any signs of wear or damage. HeadPowder provides comprehensive maintenance services to ensure that the system operates at peak efficiency and minimizes downtime. The use of high-quality materials and components in the system's construction also contributes to its longevity, as it is designed to withstand the harsh conditions associated with handling fine powders. By following proper maintenance procedures and using high-quality components, the system can provide reliable service for many years, making it a cost-effective solution for long-distance material transport.
Conclusion
The long-distance pneumatic conveying system for rice husk powder from HeadPowder is a highly efficient and reliable solution for transporting fine, lightweight powders over long distances. With its advanced features, operational benefits, and proven performance in various industrial applications, the system offers a cost-effective alternative to traditional material handling methods. By addressing the unique challenges associated with rice husk powder, the system ensures optimal performance and minimal material loss, making it an ideal choice for companies looking to improve their production efficiency and reduce operational costs. HeadPowder's expertise in engineering and design ensures that the system is tailored to meet the specific needs of each application, providing a customized solution that delivers maximum value.