

Long - Distance Pneumatic Conveying System for Manganese Carbonate
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and implementation of advanced material handling solutions. The long - distance pneumatic conveying system for manganese carbonate is a sophisticated piece of equipment engineered to efficiently transport manganese carbonate over extended distances. This system is particularly valuable in industrial settings where traditional bulk material handling methods may be less effective or more costly.
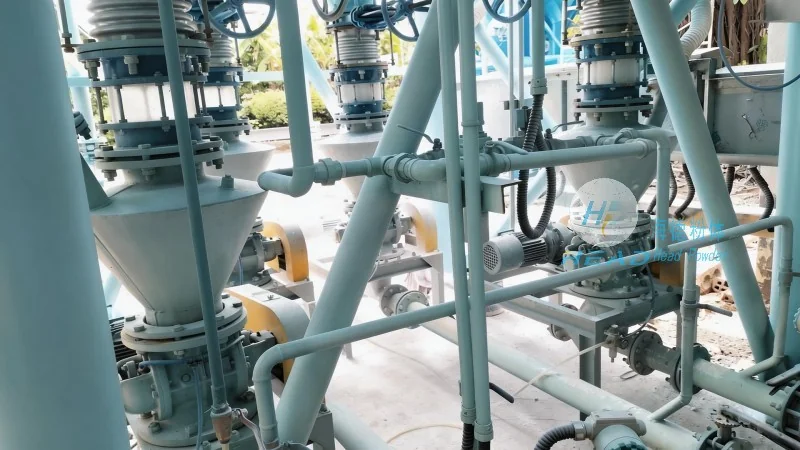
Key Features and Technical Specifications
The system is built with high - quality components to ensure durability and reliable operation. It incorporates advanced control systems that allow for precise regulation of air flow and material transport. The conveying pipeline is constructed from materials resistant to corrosion, which is essential when handling manganese carbonate, a chemical compound that can be abrasive and reactive under certain conditions. The system's design minimizes material degradation during transport, preserving the quality of the manganese carbonate product. HeadPowder's engineers have optimized the system's performance parameters, including air velocity and pressure, to achieve maximum efficiency while maintaining low energy consumption. The system is also equipped with safety features such as pressure relief valves and automatic shut - off mechanisms to prevent accidents and ensure safe operation.
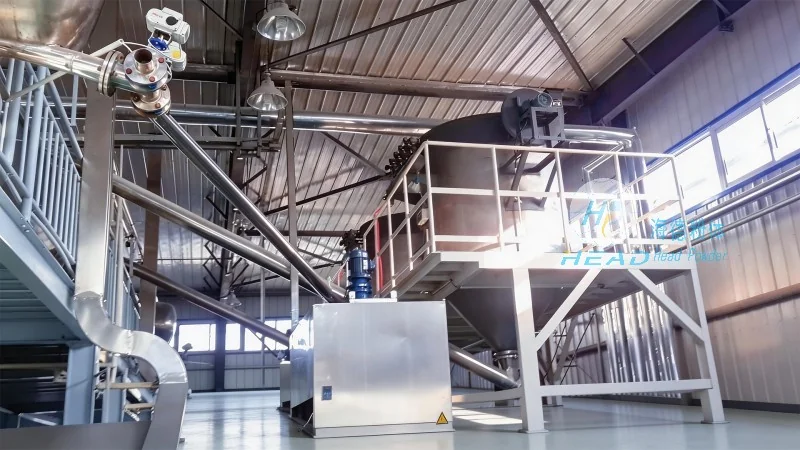
Application Scenarios and Benefits
This pneumatic conveying system is widely used in the mining and chemical industries. In mining operations, it facilitates the transport of manganese carbonate from processing plants to storage facilities or for further processing. In chemical manufacturing, it enables the efficient movement of the material between different stages of production, such as from crushing and grinding to packaging. The primary benefits of this system include increased operational efficiency, reduced labor costs, and enhanced safety compared to manual or mechanical handling methods. By automating the material transport process, the system minimizes the risk of human error and workplace accidents. Additionally, the system's ability to handle large volumes of material in a continuous manner improves overall production throughput.
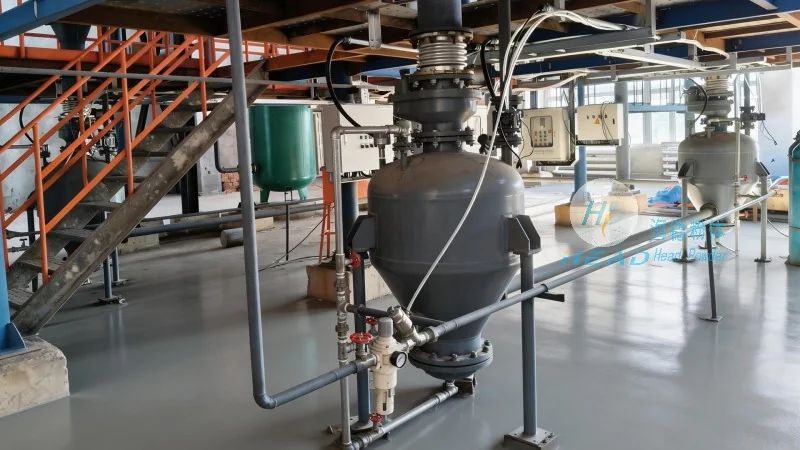
Customization and Integration Services
HeadPowder understands that each industrial application has unique requirements. Therefore, the company offers customization services to tailor the long - distance pneumatic conveying system to specific client needs. This includes adjusting the system's capacity, modifying the conveying distance, and integrating it with existing production lines. The engineering team at HeadPowder works closely with clients to understand their operational challenges and provide solutions that meet their exact specifications. The company also provides comprehensive installation and commissioning services to ensure that the system is set up correctly and operates at peak performance from the start. Post - installation support and maintenance services are available to keep the system running smoothly over its service life.
Quality Assurance and Compliance
HeadPowder adheres to strict quality standards in the design, manufacturing, and testing of its pneumatic conveying systems. All components are manufactured using high - grade materials that meet international industry standards. The system undergoes rigorous testing to ensure it meets performance criteria and safety regulations. Compliance with relevant environmental and safety regulations is a priority, ensuring that the system operates in an environmentally responsible manner and protects the health and safety of workers. HeadPowder's commitment to quality is reflected in its certifications and client feedback, which highlight the reliability and effectiveness of its products.
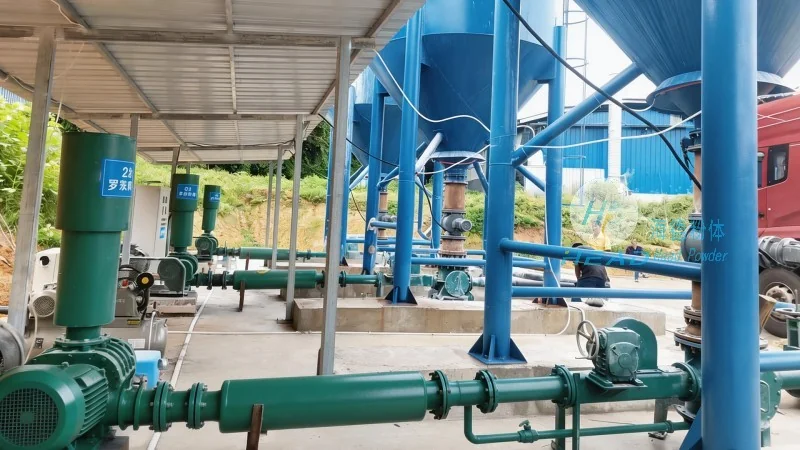
Conclusion
The long - distance pneumatic conveying system for manganese carbonate from HeadPowder is a reliable and efficient solution for industrial material handling. By leveraging advanced engineering and quality materials, the system provides significant benefits in terms of operational efficiency, cost reduction, and safety. With customization options and comprehensive support services, HeadPowder is well - positioned to meet the diverse needs of its clients in the mining and chemical sectors. The company's focus on quality and client satisfaction ensures that the system not only meets but exceeds industry expectations, making it a preferred choice for businesses seeking to optimize their material transport processes.