

Long - distance Pneumatic Conveying System for Ammonium Bicarbonate
Ammonium bicarbonate, a widely used chemical in various industrial applications, requires efficient and reliable transportation methods to ensure consistent supply and operational efficiency. The long - distance pneumatic conveying system designed by Shandong HeadPowder Engineering Co., Ltd. addresses these needs by providing a robust solution for the safe and effective movement of this material over extended distances. This system is engineered to meet the specific demands of industries that rely on ammonium bicarbonate, offering a combination of performance, durability, and adaptability.
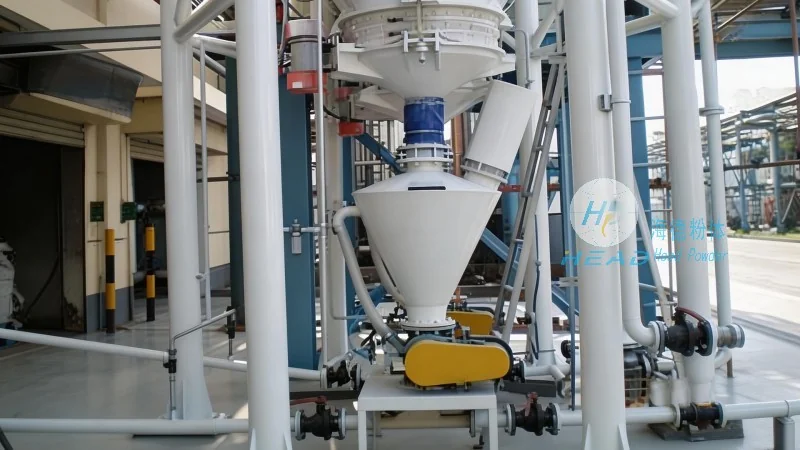
Key Features of the Pneumatic Conveying System
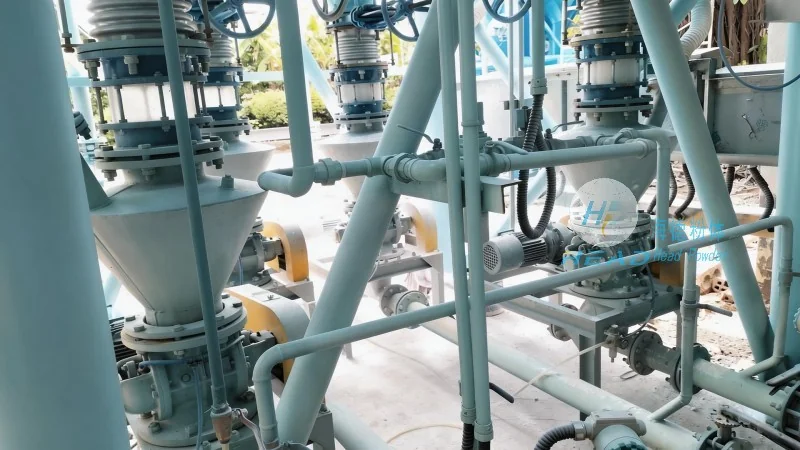
The system incorporates several advanced features that enhance its functionality and reliability. Firstly, it utilizes a high - efficiency air - flow mechanism that ensures consistent material transport without the need for excessive pressure or energy consumption. The design includes a series of specialized components such as airlocks, rotary valves, and flexible hoses, which work in tandem to maintain the integrity of the ammonium bicarbonate during transit. Additionally, the system is equipped with advanced control systems that allow for real - time monitoring and adjustment of the conveying process, ensuring optimal performance under varying operational conditions. The robust construction of the equipment, made from corrosion - resistant materials, ensures long - term durability and minimal maintenance requirements, making it suitable for continuous industrial use.
Company Background and Expertise
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer in the field of chemical processing equipment. With a strong focus on innovation and customer - centric solutions, the company has established itself as a trusted partner for industries requiring specialized conveying systems. HeadPowder has a team of experienced engineers and technicians who bring extensive knowledge and expertise to the design and development of their products. The company's commitment to quality and safety is evident in the rigorous testing and certification processes that their systems undergo before deployment. This expertise allows them to tailor solutions to meet the unique requirements of each client, ensuring that the long - distance pneumatic conveying system for ammonium bicarbonate is optimized for specific operational needs.
Application and Operational Benefits
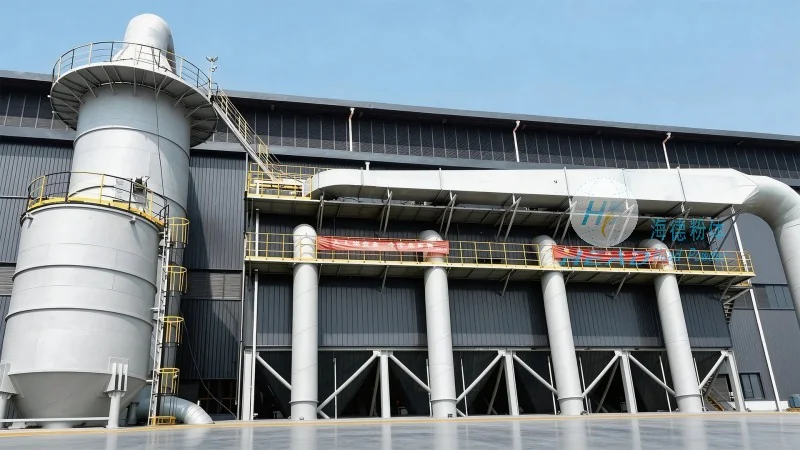
The long - distance pneumatic conveying system for ammonium bicarbonate is particularly suitable for applications where material handling over significant distances is required, such as in fertilizer production, chemical manufacturing, and food processing industries. By eliminating the need for traditional bulk handling methods like trucks or conveyor belts, the system reduces operational costs and improves overall efficiency. The system's ability to handle ammonium bicarbonate in a dust - free and controlled manner minimizes environmental impact and ensures compliance with safety regulations. Furthermore, the system's modular design allows for easy integration into existing production lines, reducing downtime during installation and maintenance. The consistent and reliable transport of ammonium bicarbonate ensures that downstream processes operate smoothly, leading to improved productivity and reduced waste.
Customization and Support Services
HeadPowder understands that each industrial application has unique requirements, and therefore offers customized solutions for the long - distance pneumatic conveying system. The company works closely with clients to assess their specific needs, including the volume of material to be conveyed, the distance of transport, and the environmental conditions. Based on this assessment, they design and manufacture a system that meets all operational criteria. Additionally, HeadPowder provides comprehensive after - sales support, including installation, training, and maintenance services. Their technical support team is available to assist with any issues that may arise, ensuring that the system operates at peak performance throughout its service life. The company's commitment to customer satisfaction is reflected in their comprehensive warranty and service agreements, providing clients with peace of mind regarding the reliability and longevity of their equipment.

Conclusion and Contact Information
The long - distance pneumatic conveying system for ammonium bicarbonate developed by Shandong HeadPowder Engineering Co., Ltd. represents a significant advancement in material handling technology. By combining advanced engineering, robust construction, and customer - focused solutions, the system offers a reliable and efficient means of transporting ammonium bicarbonate over extended distances. With the support of headpowder's expertise and commitment to quality, industries can enhance their operational efficiency and ensure consistent supply of this essential chemical. For more information or to discuss specific requirements, please contact Shandong HeadPowder Engineering Co., Ltd., located in Shandong, China.