

Cereal Pneumatic Conveying Systems: The Intelligent and Efficient New Era of Cereal Transport
Discover the advanced technology of cereal pneumatic conveying systems, a revolutionary solution for efficient and intelligent cereal transport. This system represents a significant advancement in material handling, offering a modern approach to moving cereal products with precision and reliability. HeadPowder, a leading manufacturer based in Shandong, China, specializes in providing cutting-edge solutions for the food processing industry. Our cereal pneumatic conveying systems are designed to meet the highest standards of efficiency, safety, and performance.
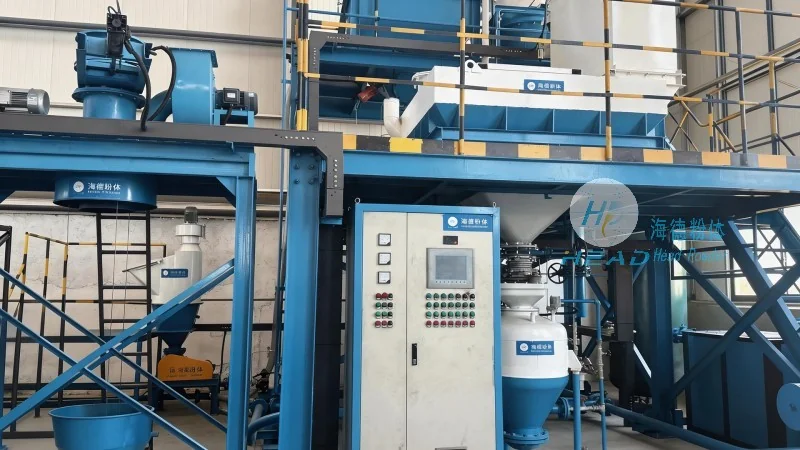
Introduction to Cereal Pneumatic Conveying Systems
At Shandong HeadPowder Engineering Co., Ltd., we specialize in providing cutting-edge solutions for the food processing industry. Our cereal pneumatic conveying systems are designed to meet the highest standards of efficiency, safety, and performance. As a leading manufacturer in this field, HeadPowder combines years of expertise with innovative engineering to deliver systems that enhance productivity and reduce operational costs for our clients.
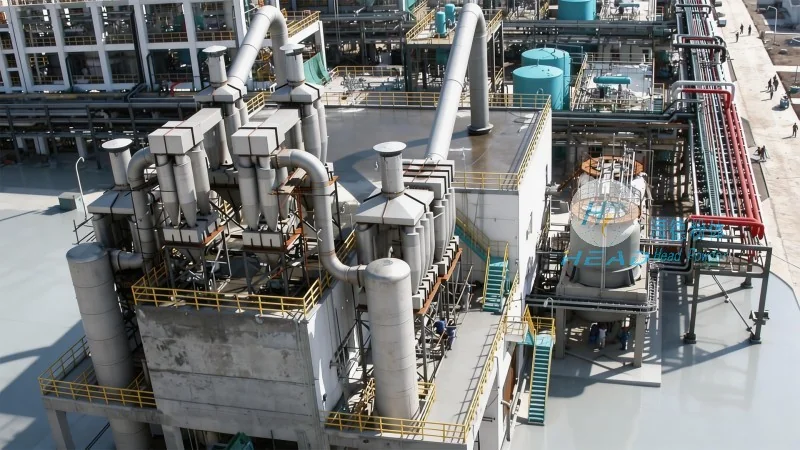
Key Features and Benefits of Our Cereal Pneumatic Conveying Systems
Our systems are engineered with several key features that set them apart in the market. The primary advantage is the ability to transport cereal products in a dust-free environment, which is crucial for maintaining product quality and ensuring compliance with food safety regulations. The pneumatic conveying method eliminates the need for mechanical components like belts or chains, reducing maintenance requirements and extending the system's lifespan. Additionally, these systems offer flexibility in layout, allowing for customized configurations to fit various production facilities. The intelligent control systems integrated into our solutions enable real-time monitoring and adjustment, optimizing the conveying process for maximum efficiency. This results in consistent product flow, reduced downtime, and improved overall operational reliability.
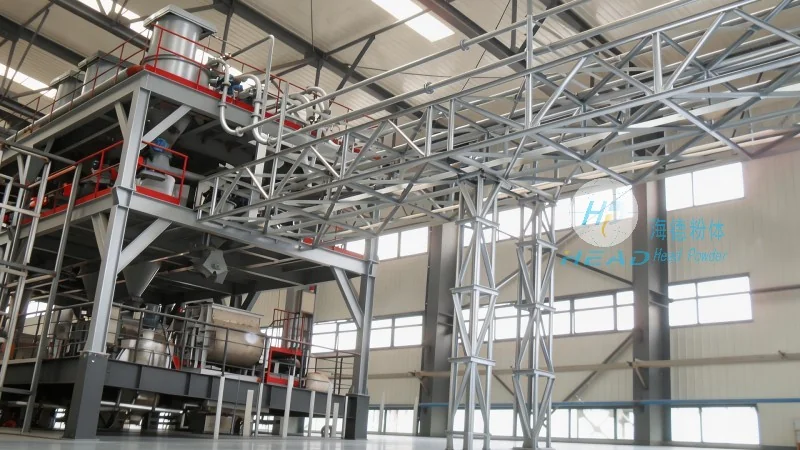
How the Cereal Pneumatic Conveying System Works
The core of our system is the pneumatic conveying principle, which uses air pressure to move cereal materials through a pipeline network. The process begins with the material being fed into a hopper, where it is then conveyed by a stream of air under controlled pressure. The system includes components such as feeders, air locks, and cyclones to ensure smooth and continuous material transport. The use of positive pressure or negative pressure systems depends on the specific application and material characteristics. Our engineers design each system to match the unique needs of the client, ensuring optimal performance for different cereal types and production volumes.
Applications in the Food Processing Industry
Our cereal pneumatic conveying systems are widely used in various applications within the food processing sector. They are ideal for transporting raw cereals such as wheat, corn, and oats from storage to processing lines, as well as for moving finished products like breakfast cereals and flour. The systems are also suitable for handling other dry, free-flowing materials, making them versatile for different production stages. By integrating our systems into existing facilities, companies can streamline their operations, improve workflow, and enhance product quality. The consistent and controlled transport of materials reduces the risk of contamination and ensures that the final product meets the highest standards of purity and safety.
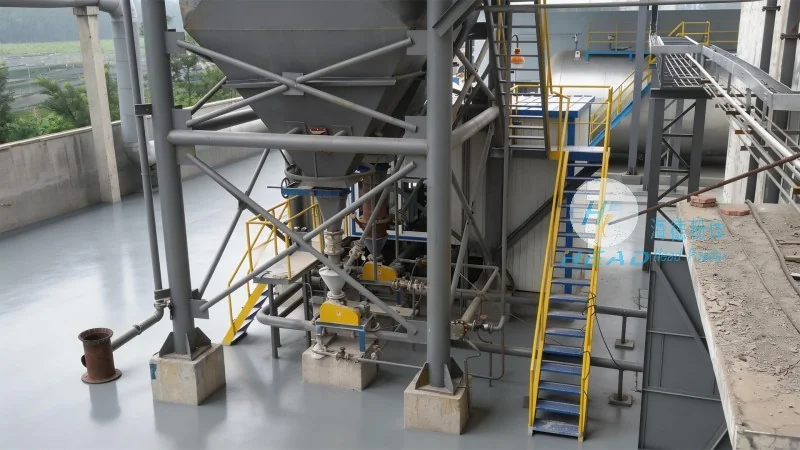
Customization and After-Sales Support
At HeadPowder, we understand that each client has unique requirements. Therefore, we offer comprehensive customization options to tailor our systems to specific needs. Our team of experienced engineers works closely with clients to design systems that fit their production capacity, space constraints, and operational goals. We also provide thorough after-sales support, including installation, training, and maintenance services. Our commitment to customer satisfaction ensures that clients receive not only high-quality equipment but also reliable support throughout the system's lifecycle. This approach helps to minimize downtime and maximize the return on investment for our clients.