

Pharmaceutical Pneumatic Conveying Systems: The Intelligent and Efficient New Era of Pharmaceutical
Pharmaceutical pneumatic conveying systems are advanced technologies designed to transport powders and granules within pharmaceutical manufacturing environments. These systems employ air or gas as the conveying medium, enabling materials to be moved through a network of pipes with minimal contact with external contaminants. By maintaining a closed system, they significantly reduce the risk of cross-contamination, a critical factor in pharmaceutical production where product purity and safety are paramount. Additionally, these systems offer precise control over material flow rates, pressure, and temperature, which are essential for maintaining consistent product quality and adhering to regulatory guidelines such as those from the FDA and GMP (Good Manufacturing Practice).
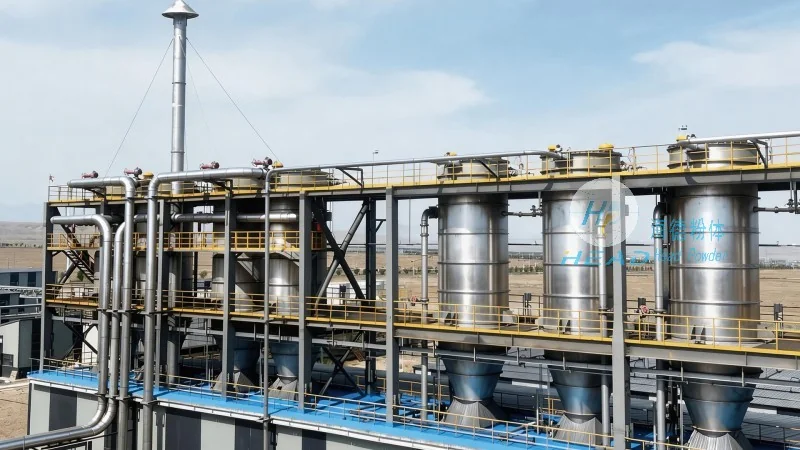
Core Advantages of Our Pneumatic Conveying Solutions
As a leading provider in the field, Shandong HeadPowder Engineering Co., Ltd. (headpowder) offers pharmaceutical pneumatic conveying systems that deliver superior performance and reliability. The primary benefits of our solutions include: enhanced safety through enclosed operation, reduced labor costs due to automated material handling, and improved process efficiency by minimizing downtime and material loss. Our systems are also designed for easy integration into existing production lines, allowing for seamless upgrades without major disruptions to operations.
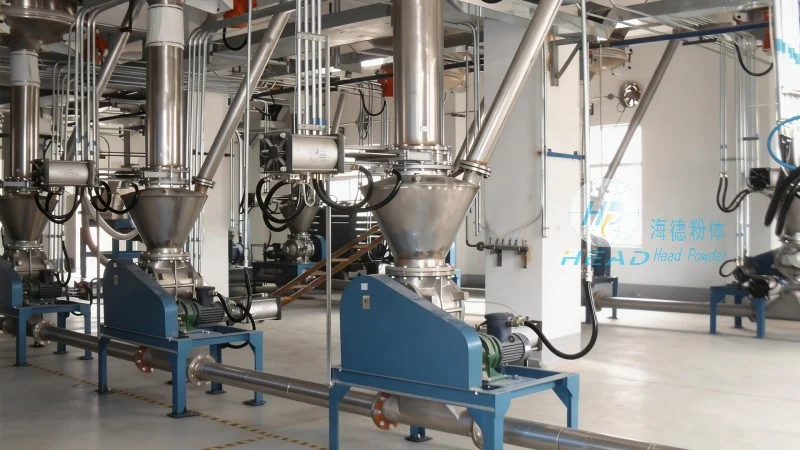
Technical Specifications and Customization Options
Our pharmaceutical pneumatic conveying systems are available in various configurations to suit diverse application requirements. Key technical specifications include: a range of conveying capacities from low to high volume operations, adjustable air pressure settings to accommodate different material properties, and modular components that facilitate maintenance and replacement. We also offer customized solutions tailored to specific production needs, such as specialized materials handling for sensitive or hazardous powders, ensuring that our systems meet the unique challenges of each client's pharmaceutical process.
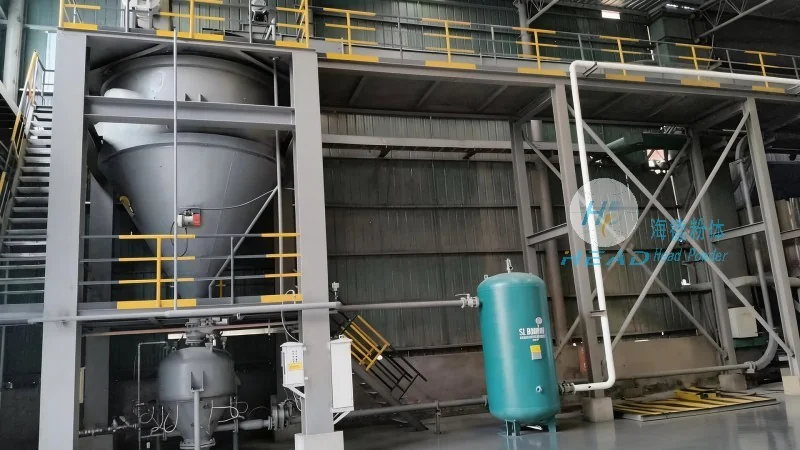
Application Examples in Pharmaceutical Manufacturing
Pharmaceutical pneumatic conveying systems are widely used in various stages of drug production. For instance, in the raw material processing stage, these systems efficiently transport raw powders from storage to mixing and blending units. During formulation, they ensure precise dosing of active pharmaceutical ingredients (APIs) and excipients into production batches. In the packaging phase, they can handle finished product powders, such as capsules or powders for inhalation, with minimal risk of contamination. Our systems have been successfully implemented in applications ranging from small-scale laboratory production to large-scale industrial manufacturing, demonstrating their versatility and effectiveness across different production scales.
Quality Assurance and Compliance
At headpowder, we prioritize quality and compliance in all our manufacturing processes. Our pharmaceutical pneumatic conveying systems are constructed using materials that meet or exceed industry standards for chemical resistance and durability, such as stainless steel and food-grade plastics. These materials are chosen to prevent corrosion and ensure long-term performance. Furthermore, our systems are designed to be easily cleaned and sanitized, which is crucial for maintaining compliance with GMP regulations. We conduct rigorous testing and validation procedures to ensure that each system meets the required performance criteria before delivery, providing clients with confidence in the reliability and safety of our equipment.
Conclusion and Contact Information
Pharmaceutical pneumatic conveying systems from Shandong HeadPowder Engineering Co., Ltd. represent a reliable and efficient solution for modern pharmaceutical material handling. By leveraging advanced technology and adhering to strict quality standards, our systems help pharmaceutical manufacturers enhance productivity, reduce operational risks, and maintain compliance with industry regulations. With our headquarters located in Shandong, China, headpowder continues to serve clients globally with innovative and tailored solutions for their pharmaceutical processing needs.