

Design of a Vacuum Pneumatic Conveying Device for Pearl Salt Powder
At Shandong HeadPowder Engineering Co., Ltd., we specialize in the design and manufacturing of advanced material handling equipment tailored for the food and chemical industries. Our latest innovation, the vacuum pneumatic conveying device for pearl salt powder, represents a significant advancement in efficient and hygienic powder transport solutions.
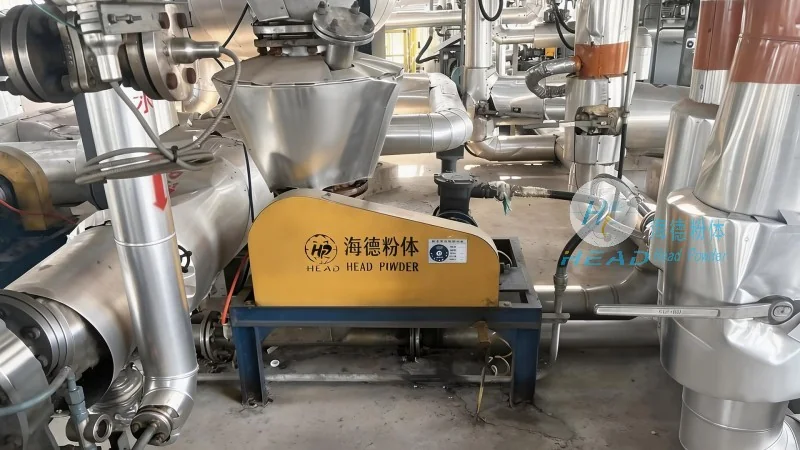
Overview of the Vacuum Pneumatic Conveying System
The vacuum pneumatic conveying device for pearl salt powder is engineered to handle fine powders like pearl salt with precision and reliability. This system utilizes a vacuum-based approach to draw material from a storage silo or hopper into a processing unit, eliminating the need for mechanical components that can cause contamination or wear. The design ensures a clean, dust-free environment, which is critical for maintaining product quality and adhering to stringent industry standards.
Key Features and Technical Specifications
Our vacuum pneumatic conveying device incorporates several key features that enhance performance and durability. The system includes a high-efficiency vacuum pump, a stainless steel material transport pipeline, and a control panel with real-time monitoring capabilities. The pipeline is constructed from food-grade stainless steel, ensuring compliance with hygiene regulations and preventing material degradation. The vacuum pump is designed for low noise operation and energy efficiency, reducing operational costs while maintaining consistent conveying rates. The control system allows for adjustable conveying speeds and pressure settings, enabling seamless integration with existing production lines.
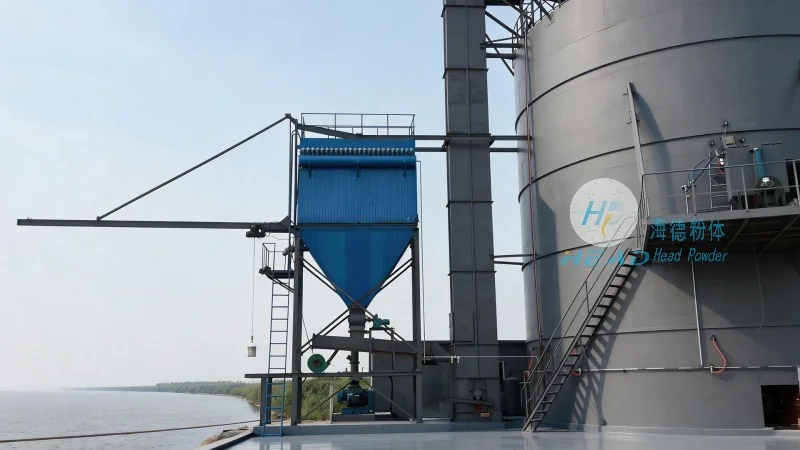
Benefits for Pearl Salt Powder Handling
Implementing a vacuum pneumatic conveying system for pearl salt powder offers numerous advantages for manufacturers. Firstly, it minimizes product loss and contamination by eliminating manual handling and open-air transport. The enclosed system prevents dust dispersion, protecting both the product and the working environment. Secondly, the system enhances operational efficiency by automating the material transfer process, reducing downtime and labor costs. Additionally, the hygienic design of the equipment ensures that the product remains free from microbial contamination, which is essential for food-grade applications. The system's compact footprint also allows for easy installation in existing facilities without major structural modifications.
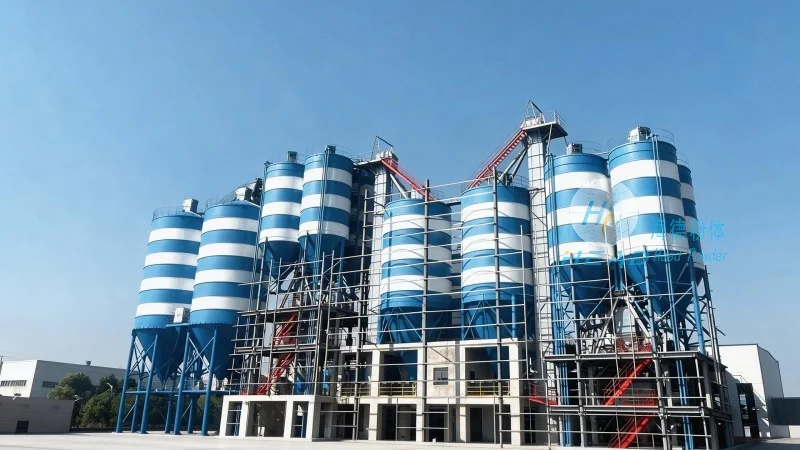
Application Scenarios and Industry Compliance
The vacuum pneumatic conveying device is particularly suitable for applications in the food processing, pharmaceutical, and chemical industries where handling fine powders requires strict adherence to safety and quality standards. It is ideal for transferring pearl salt from storage silos to mixing, packaging, or processing units. The system's design complies with international standards such as FDA and GMP regulations, ensuring that it meets the highest hygiene and safety requirements. This makes it a reliable choice for manufacturers seeking to enhance their production processes while maintaining product integrity.
Customization and After-Sales Support
At Shandong HeadPowder Engineering Co., Ltd., we understand that each production facility has unique requirements. Therefore, our vacuum pneumatic conveying devices are customizable to meet specific operational needs. We offer tailored solutions, including different pipeline lengths, pump capacities, and control configurations, to ensure optimal performance. Our team of engineers provides comprehensive after-sales support, including installation guidance, maintenance training, and technical assistance. We also offer spare parts and regular maintenance services to minimize downtime and extend the lifespan of the equipment.