

Types and Practical Applications of Pneumatic Conveying Systems for Calcined Ash Transport
For industrial facilities dealing with calcined ash, the efficient and reliable transport of this material is crucial to maintaining operational efficiency and safety. Pneumatic conveying systems have emerged as a preferred solution due to their ability to handle bulk materials like calcined ash with minimal maintenance and environmental impact. This article explores the different types of pneumatic conveying systems used in calcined ash transport and their practical applications, highlighting the expertise of Shandong HeadPowder Engineering Co., Ltd. in providing tailored solutions for such industrial needs.
Overview of Pneumatic Conveying Systems for Calcined Ash
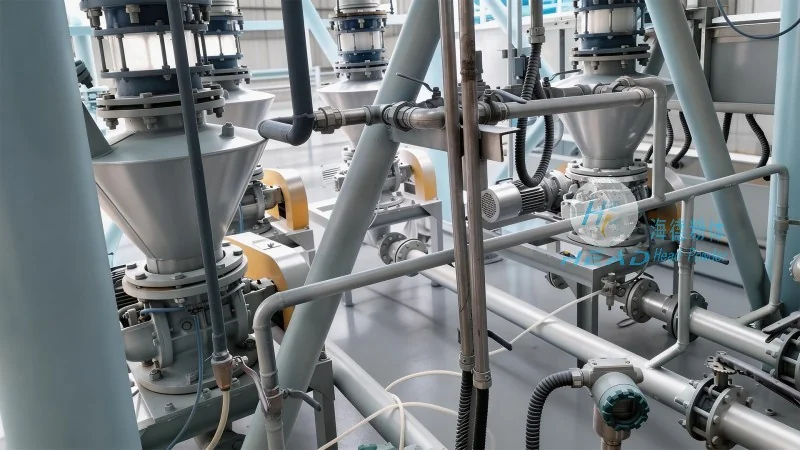
Pneumatic conveying systems utilize air or other gases to transport bulk materials through a pipeline. In the context of calcined ash, these systems are designed to handle the specific properties of the material, such as its density, moisture content, and particle size. The choice of system type depends on factors like the distance of transport, the volume of material, and the required speed of delivery. Shandong HeadPowder Engineering Co., Ltd. specializes in designing and implementing pneumatic conveying solutions that meet the unique demands of calcined ash handling in various industrial settings.
Types of Pneumatic Conveying Systems
There are primarily two types of pneumatic conveying systems: pressure and vacuum systems. Each type has distinct characteristics and is suitable for different applications in calcined ash transport.
Pressure Pneumatic Conveying Systems
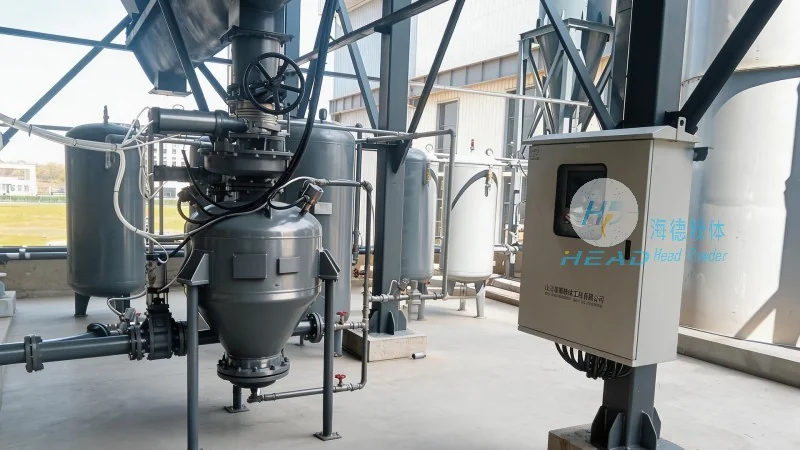
Pressure systems operate by pushing material through a pipeline using positive pressure, typically generated by a blower or compressor. These systems are ideal for long-distance transport and can handle larger volumes of material. In calcined ash applications, pressure systems are often used when the ash needs to be transported over several hundred meters or more. The high-pressure air forces the ash particles through the pipeline, ensuring consistent flow and minimal blockages. Shandong HeadPowder Engineering Co., Ltd. designs pressure systems with robust components that can withstand the abrasive nature of calcined ash, ensuring long-term reliability and low maintenance costs.
Vacuum Pneumatic Conveying Systems
Vacuum systems, on the other hand, use negative pressure to draw material into the pipeline. These systems are commonly used for shorter distances and when the material needs to be collected from multiple points. In calcined ash transport, vacuum systems are suitable for handling ash from storage silos or collection points and transporting it to processing units. The low-pressure environment reduces the risk of dust emissions and is more energy-efficient for shorter transport distances. Shandong HeadPowder Engineering Co., Ltd. offers vacuum systems that are compact and easy to install, making them a practical choice for facilities with limited space or where the transport distance is relatively short.
Practical Applications of Pneumatic Conveying Systems
The practical applications of pneumatic conveying systems in calcined ash transport vary based on the system type and the specific requirements of the industrial process. Here are some common scenarios where these systems are effectively utilized:
Transport from Calcination Furnaces to Storage Silos
After calcination, ash is often collected from the furnace and transported to storage silos for further processing or disposal. Pneumatic conveying systems provide a direct and efficient method for this transfer. Pressure systems are commonly used for this application, as they can handle the high volume of ash produced by large-scale calcination processes. The system design by Shandong HeadPowder Engineering Co., Ltd. ensures that the ash is conveyed without clogging or degradation, maintaining the quality of the material for subsequent use or disposal.
Transfer Between Processing Units
In industrial plants, calcined ash may need to be transferred between different processing units, such as from a drying unit to a grinding unit or from a storage area to a mixing station. Pneumatic conveying systems offer a flexible solution for these inter-unit transfers. Vacuum systems are often preferred for shorter distances between units, as they can be easily integrated into existing plant layouts. Shandong HeadPowder Engineering Co., Ltd. designs custom vacuum systems that can handle the specific flow rates and particle sizes required for each processing step, ensuring smooth operation and minimal downtime.
Environmental Control and Dust Management
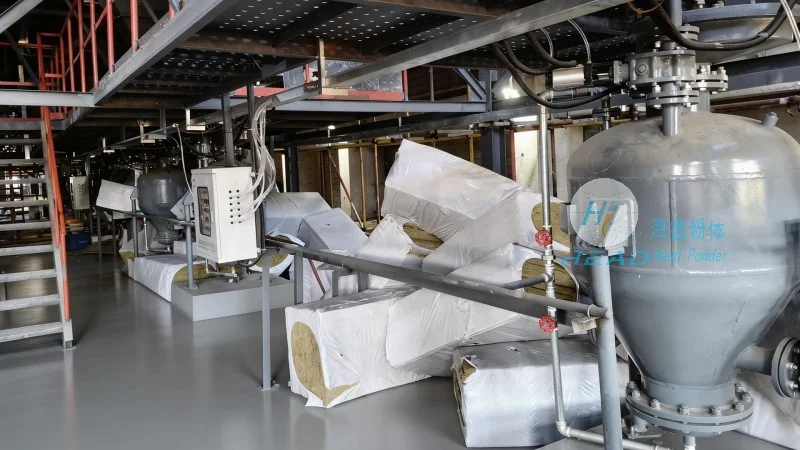
Calcined ash can be a source of dust, which poses health and safety risks if not properly managed. Pneumatic conveying systems, especially vacuum systems, help in controlling dust emissions by enclosing the material in a sealed pipeline. This not only protects workers from inhalation hazards but also prevents environmental contamination. Shandong HeadPowder Engineering Co., Ltd. incorporates advanced dust control features in their pneumatic conveying systems, such as sealed connections and efficient filtration, to ensure compliance with environmental regulations and maintain a safe working environment.
Key Considerations for Implementing Pneumatic Conveying Systems
When implementing a pneumatic conveying system for calcined ash transport, several factors must be considered to ensure optimal performance and longevity. These include the material properties of the ash, the distance and layout of the transport route, and the required flow rate. Shandong HeadPowder Engineering Co., Ltd. conducts thorough assessments of these factors to design a system that meets the specific needs of each client. The company’s expertise in material handling and process engineering ensures that the chosen system is both efficient and cost-effective.
Conclusion
Pneumatic conveying systems are a vital component in the efficient transport of calcined ash, offering advantages in terms of safety, reliability, and environmental control. The choice between pressure and vacuum systems depends on the specific requirements of the application, with each type providing unique benefits. Shandong HeadPowder Engineering Co., Ltd. provides comprehensive solutions for calcined ash transport, leveraging their expertise in pneumatic conveying technology to deliver systems that meet the highest standards of performance and durability. For industrial facilities seeking reliable and efficient calcined ash transport solutions, Shandong HeadPowder Engineering Co., Ltd. is a trusted partner in providing tailored pneumatic conveying systems.