

Classification and Application Analysis of Bentonite Pneumatic Conveying Systems
Bentonite, a natural clay mineral with excellent swelling and thixotropic properties, is widely used in various industrial applications such as drilling fluids, foundry sand, and environmental remediation. The efficient transportation of bentonite powder from storage to processing units is crucial for maintaining production efficiency and product quality. Pneumatic conveying systems offer a reliable and flexible solution for handling this fine powder, ensuring minimal dust generation and high material recovery rates.
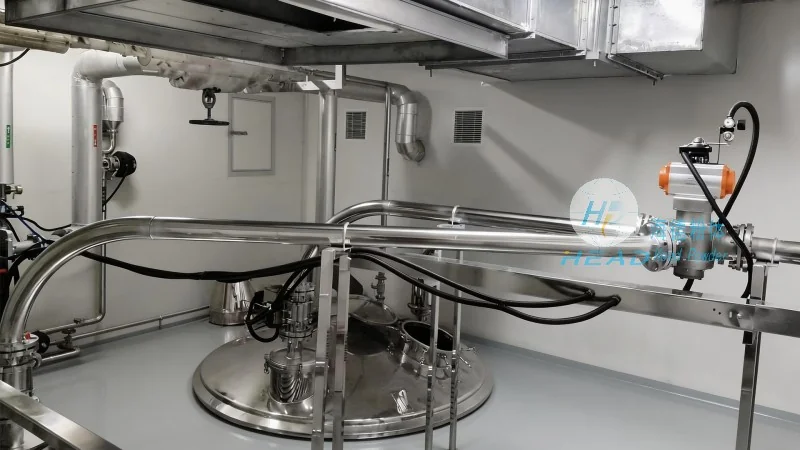
Classification of Bentonite Pneumatic Conveying Systems
Bentonite pneumatic conveying systems can be classified based on several key parameters, including the conveying principle, pressure, and system configuration. The primary classifications include:
- Positive Pressure (Pressure) Systems: These systems use a blower or compressor to generate positive pressure in the pipeline, pushing the material forward. They are suitable for long-distance and high-capacity conveying of fine powders like bentonite.
- Negative Pressure (Vacuum) Systems: In this configuration, a vacuum pump creates a negative pressure in the pipeline, drawing the material from the source. This type is often used for short-distance conveying or when the material needs to be transported from multiple sources.
- Combined Systems: A hybrid approach that combines both positive and negative pressure elements, offering flexibility for complex conveying routes and varying material flow requirements.
Each classification has its advantages and limitations, and the choice depends on factors such as the distance to be covered, the volume of material, and the specific characteristics of the bentonite being handled.
Key Applications of Bentonite Pneumatic Conveying Systems
Bentonite pneumatic conveying systems are employed in a range of industrial processes where the consistent and clean transport of bentonite is essential. Some of the key applications include:

- Drilling Fluid Preparation: In oil and gas exploration, bentonite is mixed with water to form drilling mud, which is used to lubricate and stabilize the wellbore. Pneumatic conveying ensures that the bentonite powder is accurately dosed and mixed, improving the quality of the drilling fluid.
- Foundry Sand Processing: Bentonite is used as a binder in foundry sand to improve mold strength and surface finish. The pneumatic system efficiently transports the bentonite powder to the mixing and molding equipment, ensuring uniform distribution and reducing material waste.
- Environmental Remediation: Bentonite is utilized in soil stabilization and groundwater barrier applications. The conveying system facilitates the transport of bentonite to construction sites, enabling rapid deployment in environmental projects.
- Food and Pharmaceutical Industries: In some specialized applications, bentonite is used as a filter aid or clarifying agent. The pneumatic conveying system ensures that the material is handled hygienically and without contamination, meeting strict industry standards.
Across these applications, the ability of pneumatic systems to handle fine powders with minimal dust and high efficiency makes them the preferred choice for bentonite transportation.
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer and supplier of advanced pneumatic conveying systems tailored for bentonite and other fine powders. With a strong focus on innovation and customer satisfaction, the company has established itself as a trusted partner in the industry.
HeadPowder specializes in designing and manufacturing customized pneumatic conveying solutions that meet the unique requirements of each client. The company’s engineers work closely with customers to understand their operational needs, material characteristics, and production goals, ensuring that the final system is optimized for performance, reliability, and cost-effectiveness.
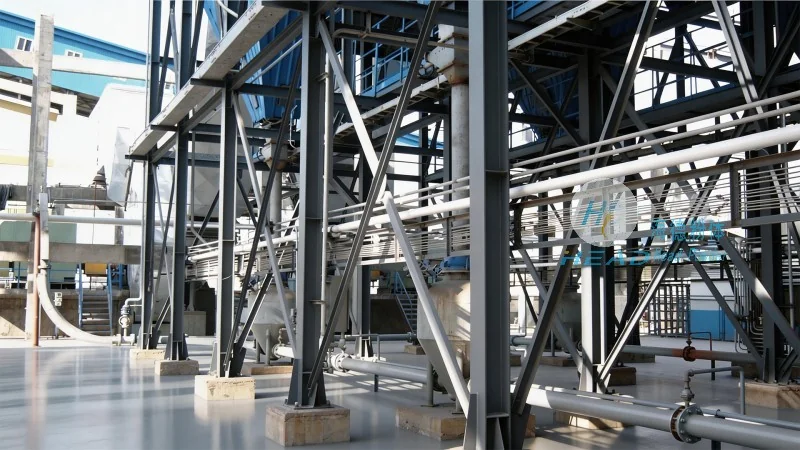
HeadPowder’s product portfolio includes a wide range of components such as rotary valves, airlocks, cyclone separators, and dust collectors, all engineered to handle the specific challenges of bentonite transportation. The company adheres to international quality standards and employs rigorous testing protocols to ensure that every system meets the highest performance benchmarks.
HeadPowder’s commitment to sustainability and environmental responsibility is reflected in its product design. The systems are engineered to minimize energy consumption and reduce emissions, aligning with global efforts to promote eco-friendly industrial practices. Additionally, the company provides comprehensive after-sales support, including installation, maintenance, and technical assistance, to ensure long-term system reliability.
With its headquarters in Shandong, China, HeadPowder leverages its local presence to serve clients across the region and beyond. The company’s team of experienced professionals brings a wealth of knowledge and expertise to every project, enabling the delivery of solutions that enhance operational efficiency and contribute to the success of industrial processes.