

Classification and Application Analysis of Organic Fertilizer Granule Pneumatic Conveying Systems
Organic fertilizer granule pneumatic conveying systems are critical in modern agricultural and industrial operations, designed to efficiently transport granular organic fertilizers with precision and reliability. These systems utilize air as the conveying medium, enabling material movement without direct contact, which minimizes contamination and equipment wear. The classification of such systems is based on key factors like conveying method, material characteristics, and operational requirements. Understanding these classifications helps select the most suitable system for specific applications, ensuring optimal performance and cost-effectiveness.
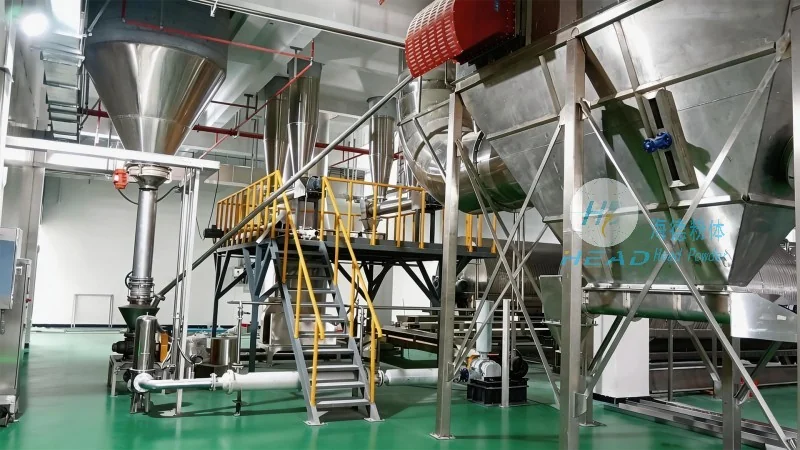
Types of Organic Fertilizer Granule Pneumatic Conveying Systems
There are primarily two main categories of pneumatic conveying systems for organic fertilizer granules: dilute-phase and dense-phase systems. Dilute-phase systems operate by suspending material particles in a high-velocity air stream (typically above 20 m/s), suitable for short to medium distances and light to medium-density granules. Dense-phase systems use lower air velocities and higher material concentrations, often with positive pressure or vacuum, ideal for longer distances and materials prone to degradation under high-velocity air.
Sub-types further differentiate systems based on air flow direction and pressure. Pressure systems use compressed air to push material, while vacuum systems use suction. The choice depends on the conveying line layout, distance, and multi-point material handling needs. Features like rotary valves, airlocks, and cyclones control flow and separation, preventing blockages.
Key Components and Their Functions
The feed hopper or silo is the initial storage and preparation point, with feeder mechanisms (e.g., rotary valves, screw conveyors) regulating material flow. These must handle organic fertilizer characteristics (moisture, particle size) to prevent bridging or segregation.
The air supply system (blower/compressor) generates required pressure/vacuum. Dilute-phase systems use high-capacity blowers for velocity, dense-phase systems use high-pressure compressors for concentration. Air treatment components (filters, moisture separators) ensure clean, contaminant-free air, protecting fertilizer quality and system performance.
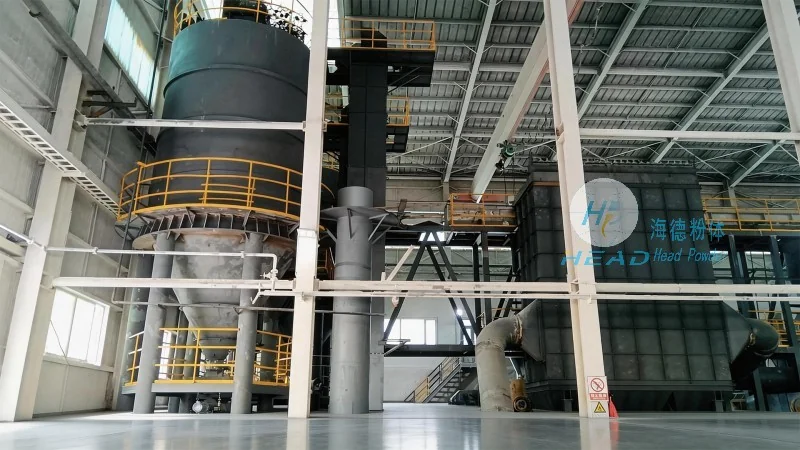
The conveying pipeline, constructed from corrosion-resistant materials (stainless steel, polyethylene, or coated surfaces), must withstand wear and chemical reactions. Design includes bends, elbows, and straight sections to minimize pressure losses. Expansion joints and supports accommodate thermal changes and structural loads for durability.
Applications of Organic Fertilizer Granule Pneumatic Conveying Systems
In fertilizer manufacturing, these systems transport raw materials from storage to processing units (granulators, mixers), ensuring continuous production. They also move finished granules to storage or loading areas for distribution. In agriculture, they enable uniform fertilizer application across fields, improving crop yields and soil health. Integration with irrigation or spraying equipment enhances nutrient delivery efficiency.
In industrial settings (composting, biogas plants), systems transport organic waste to processing facilities, facilitating conversion to fertilizers or energy. This supports sustainable waste management and resource recovery.
Advantages and Considerations
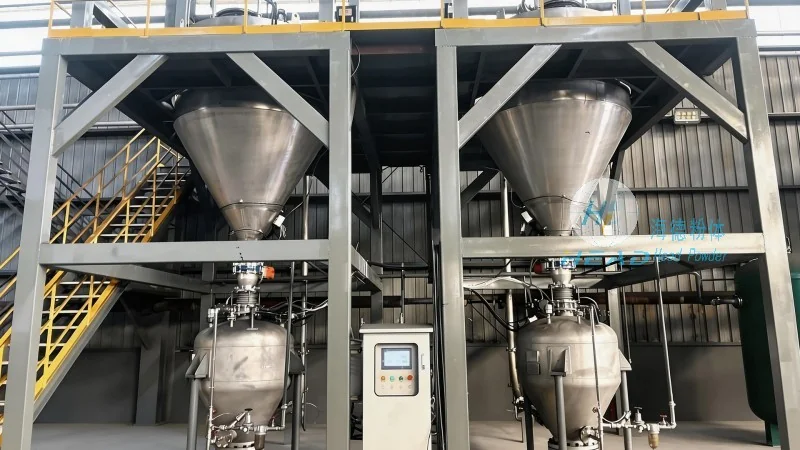
Advantages include reduced labor costs and downtime, minimized human error and workplace risks, and enhanced hygiene (preventing material contamination). However, initial investment costs can be higher than traditional methods. Regular maintenance (air filters, part lubrication, pipeline inspection) is needed to ensure performance. Energy consumption from blowers/compressors impacts operational costs. System design must account for fertilizer properties (moisture, particle size) to avoid caking or blockages.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer and supplier of advanced pneumatic conveying systems for organic fertilizers. The company focuses on innovation and quality, providing customized solutions tailored to client needs. HeadPowder’s expertise combines cutting-edge technology with practical engineering, ensuring systems are efficient, reliable, and cost-effective.
Products meet high performance and durability standards, with minimal maintenance requirements. The team collaborates closely with clients to understand unique requirements—from fertilizer type to system layout—ensuring optimized solutions that deliver long-term benefits and value.
HeadPowder offers comprehensive support, from initial consultation and design to installation, commissioning, and after-sales service. The company’s commitment to customer satisfaction and technical excellence has established it as a trusted partner in agriculture and industry. With a focus on continuous improvement, HeadPowder remains at the forefront of the pneumatic conveying industry, delivering solutions that help clients achieve operational goals and enhance productivity.