

What is Ammonium Nitrate Pneumatic Conveying? What Are the Design Principles?
Ammonium nitrate (AN) is a critical chemical compound utilized across multiple industries, including agriculture, explosives manufacturing, and chemical processing. Pneumatic conveying represents a sophisticated method for transporting bulk materials like AN through a pipeline by utilizing air or other gases as the conveying medium. This technology offers significant advantages over traditional handling methods, such as reduced dust exposure, lower labor costs, enhanced safety, and improved material flow control. By understanding the fundamental principles behind ammonium nitrate pneumatic conveying, industries can optimize their material handling processes and ensure operational efficiency.

Key Design Principles for Ammonium Nitrate Pneumatic Conveying Systems
The successful design of an ammonium nitrate pneumatic conveying system relies on several core principles that address the unique properties of the material and operational requirements. First, the conveying velocity must be carefully selected to ensure that particles are fully suspended and transported without causing excessive wear on equipment or pipeline blockages. This velocity is typically determined based on the particle size distribution, density, and flowability of ammonium nitrate, which can vary depending on the specific application and processing conditions. Second, the air pressure and flow rate are critical parameters that must be optimized to maintain consistent material transport and prevent system inefficiencies. Higher air pressures may be required for longer conveying distances or larger particle sizes, while lower pressures are suitable for shorter distances and finer materials. Third, the system design must incorporate appropriate equipment components, including hoppers for material storage, feeders to regulate flow rates, blowers or compressors to generate the conveying air, and pipelines with suitable diameters and materials to withstand the corrosive or abrasive nature of ammonium nitrate. Additionally, safety features such as explosion-proof components, dust collectors, and moisture control systems are essential to mitigate risks associated with handling this material.
Components and Equipment in Ammonium Nitrate Pneumatic Conveying Systems
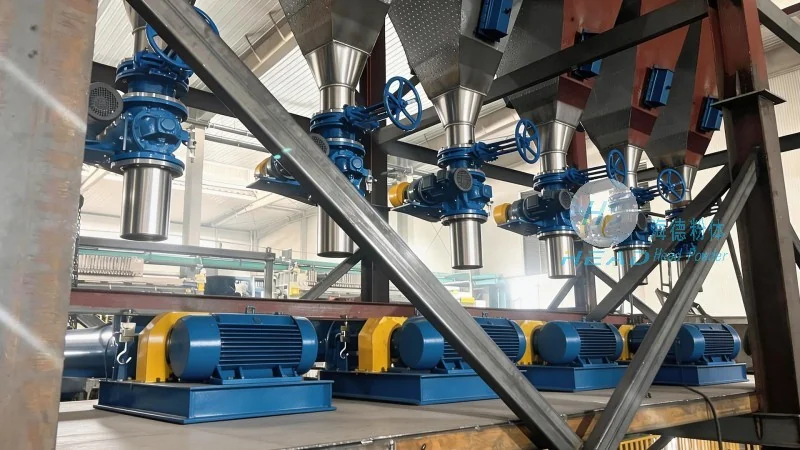
Ammonium nitrate pneumatic conveying systems consist of several interconnected components that work together to achieve efficient material transport. The primary components include a hopper, which serves as the storage vessel for the material, often equipped with a level indicator and discharge valve to control the flow rate. A feeder, such as a rotary valve or screw feeder, is used to meter the material from the hopper into the conveying line, ensuring a consistent and controlled feed. The blower or compressor provides the necessary air pressure and flow to move the material through the pipeline. This equipment is typically selected based on the required conveying capacity and pressure, with options ranging from positive displacement blowers for high-pressure applications to centrifugal compressors for lower-pressure systems. The pipeline network connects the feeder to the discharge point, with components like elbows, tees, and straight sections designed to minimize pressure loss and maintain material suspension. For ammonium nitrate, special considerations are often necessary due to its sensitivity to moisture and potential for dust explosion. Therefore, components like explosion-proof motors, dust collectors to capture and recycle fine particles, and moisture control systems to prevent material caking are commonly integrated into the design. The system may also include filters to remove contaminants from the air and maintain air quality, as well as pressure relief valves to prevent over-pressurization.
Advantages and Applications of Ammonium Nitrate Pneumatic Conveying
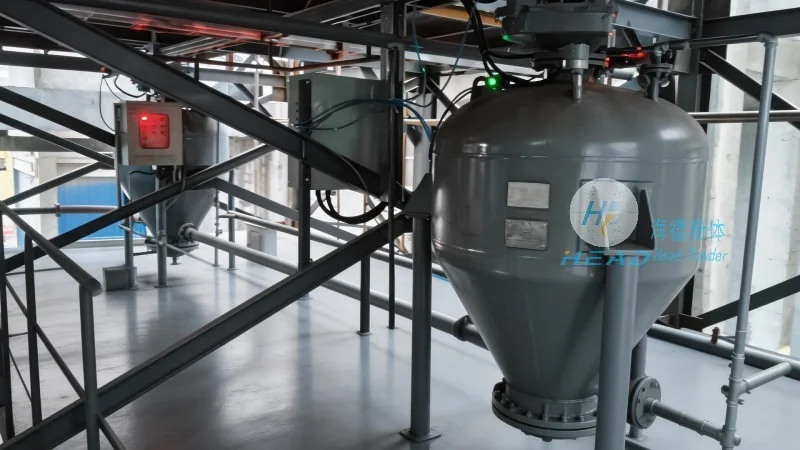
Pneumatic conveying systems for ammonium nitrate offer numerous advantages that make them a preferred choice for material handling in various industries. One of the key benefits is the ability to transport materials over long distances without the need for intermediate storage or manual handling. This is particularly valuable in fertilizer production, where ammonium nitrate is processed and transported from production facilities to storage silos or distribution centers. The technology also allows for precise control over the flow rate and material distribution, ensuring that the final product meets quality specifications. Another advantage is the reduction in dust exposure, which improves workplace safety and reduces the risk of respiratory issues for operators. Additionally, pneumatic conveying systems can handle varying material conditions, such as different particle sizes or moisture levels, by adjusting the conveying parameters accordingly. These systems are widely used in the chemical industry for processing and transporting ammonium nitrate, as well as in the explosives sector for handling raw materials and finished products. The flexibility and efficiency of pneumatic conveying make it an ideal solution for businesses seeking to streamline their material handling operations and enhance overall productivity.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer and supplier of pneumatic conveying systems and related equipment. With a strong commitment to innovation, quality, and customer satisfaction, the company specializes in providing customized solutions tailored to the specific needs of clients in the chemical, agricultural, and industrial sectors. HeadPowder's expertise in ammonium nitrate handling is built on years of experience and a deep understanding of the material's properties and handling challenges. The company's engineering team works closely with clients to design and develop systems that meet the highest safety and performance standards, ensuring reliable and efficient operation. HeadPowder's products are manufactured using advanced technology and quality control measures, adhering to international standards and regulatory requirements. The company's dedication to excellence has earned it a reputation as a trusted partner in the industry, with clients worldwide relying on their solutions to optimize material handling processes and improve operational efficiency.
Location and Contact Information
HeadPowder is headquartered in Shandong, China, with a state-of-the-art facility equipped with modern manufacturing equipment and a dedicated team of engineers, technicians, and quality control specialists. The company's location in Shandong provides easy access to key transportation networks, facilitating the delivery of products to clients across China and internationally. The facility is designed to support the entire product lifecycle, from research and development to production, testing, and after-sales service. HeadPowder's commitment to customer support includes providing technical assistance, installation guidance, and maintenance services to ensure that clients can maximize the performance and lifespan of their pneumatic conveying systems. By leveraging its expertise and local resources, HeadPowder continues to deliver high-quality solutions that meet the evolving needs of the industry.