

What is a Stone Powder Pneumatic Conveying Equipment? What Are Its Design Principles?
For industries dealing with bulk materials like stone powders, efficient and reliable material handling is crucial. A stone powder pneumatic conveying equipment is a specialized system designed to transport these powders through a pipeline using air pressure. This technology offers a clean, dust-free, and flexible solution for moving materials over short to medium distances. Understanding the design principles behind such equipment is essential for selecting the right system for specific industrial applications.
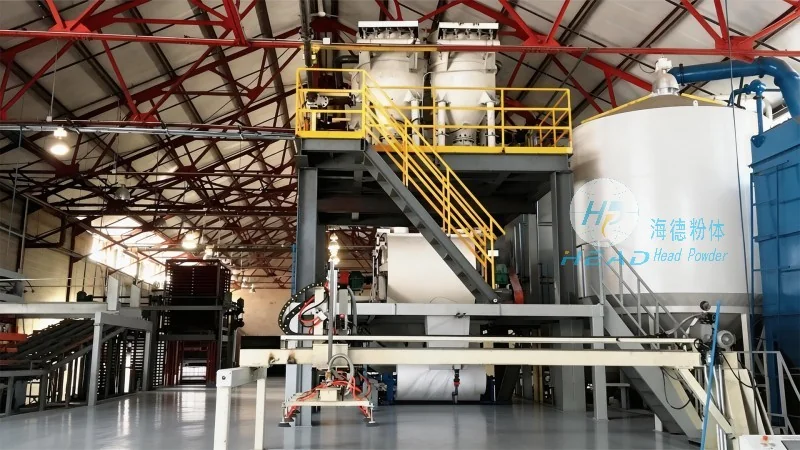
Introduction to Stone Powder Pneumatic Conveying Equipment
A stone powder pneumatic conveying system is a type of pneumatic transport equipment that utilizes compressed air or gas to move dry, fine materials like stone powders through a pipeline. Unlike traditional mechanical conveyors, this system eliminates the need for physical contact between the material and the conveyor, reducing wear and tear on equipment and minimizing the risk of contamination. The core components of a typical system include a hopper for material storage, a blower or compressor to generate airflow, a pipeline network, and a receiver or discharge unit for the material. The system operates by drawing the stone powder from the hopper into the pipeline, where it is suspended and carried by the airflow to the destination point.
HeadPowder: A Leading Manufacturer of Pneumatic Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a reputable company based in China specializing in the design, manufacturing, and supply of advanced pneumatic conveying equipment. With a strong focus on innovation and quality, HeadPowder has established itself as a trusted partner for industries requiring efficient material handling solutions. The company’s products are engineered to meet the unique demands of various applications, ensuring optimal performance and durability. HeadPowder’s commitment to customer satisfaction and technical excellence has made it a preferred choice for businesses seeking reliable pneumatic conveying systems.
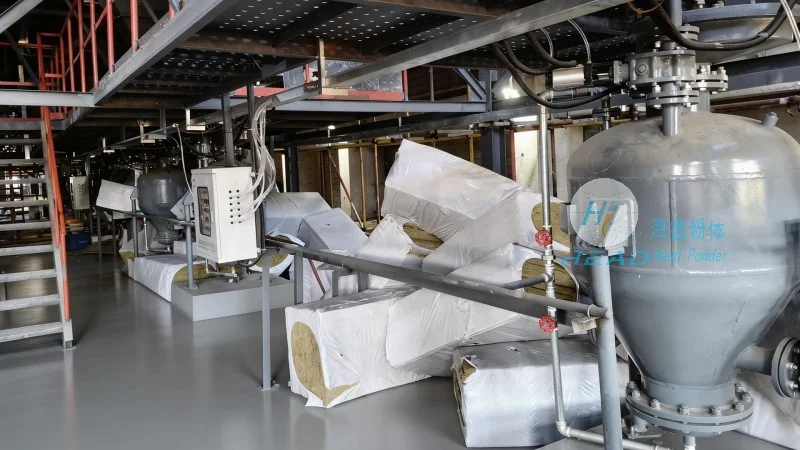
Design Principles of Pneumatic Conveying Systems
The design of a stone powder pneumatic conveying equipment is based on several key principles to ensure efficient and safe operation. The first principle is the selection of appropriate air velocity, which determines the material's suspension and transport. The air velocity must be high enough to keep the powder particles suspended in the air stream but not so high as to cause excessive pressure drops or energy consumption. The second principle is the proper sizing of the pipeline diameter and length, as these factors directly impact the system's capacity and efficiency. The third principle involves the use of appropriate components such as hoppers, blower systems, and filters to handle the specific characteristics of stone powders, including their particle size, density, and flowability.
Working Principle of the Stone Powder Pneumatic Conveying Equipment
The operation of a stone powder pneumatic conveying system begins with the material being fed into the hopper. The hopper is designed to provide a consistent flow of material to the system, preventing blockages and ensuring smooth operation. The blower or compressor then generates a high-pressure air stream, which is introduced into the pipeline. As the air flows through the pipeline, it creates a negative pressure zone that draws the stone powder from the hopper into the air stream. The powder particles are then suspended in the air and carried to the discharge point. The system may include features such as pulse jets or rotary valves to control the flow of material and maintain consistent pressure. The receiver or discharge unit at the end of the pipeline collects the material and discharges it into the desired location.
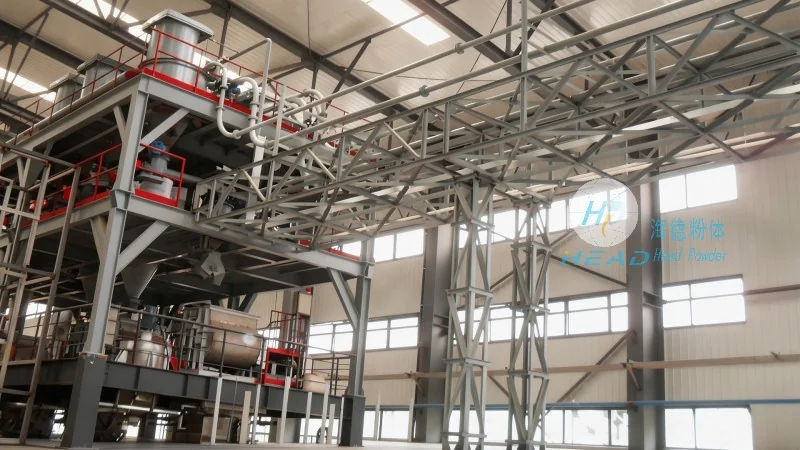
Advantages of Using Pneumatic Conveying for Stone Powders
There are several advantages to using a stone powder pneumatic conveying equipment over traditional methods. First, it provides a dust-free and clean environment, which is particularly important for industries where contamination is a concern. Second, the system is flexible and can be easily reconfigured to accommodate changes in material flow or process requirements. Third, it offers high efficiency and low maintenance costs compared to mechanical conveyors. Additionally, the system can handle a wide range of particle sizes and material types, making it suitable for various applications. The use of pneumatic conveying also reduces the risk of material degradation and improves overall process safety.
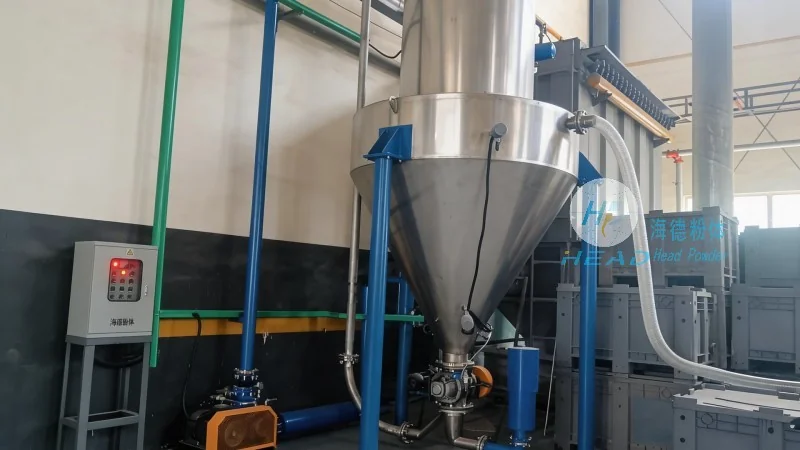
Applications of Stone Powder Pneumatic Conveying Equipment
Stone powder pneumatic conveying equipment is widely used in various industries, including mining, construction, and chemical processing. In the mining industry, it is used to transport crushed stone powders from processing plants to storage facilities or for further processing. In the construction industry, it is used to move materials such as cement, lime, and other powders to different parts of a construction site. In the chemical industry, it is used to transport various powders, including those used in pharmaceuticals and food processing. The versatility of the system makes it suitable for a wide range of applications, from small-scale operations to large industrial plants.
Conclusion and Contact Information
Stone powder pneumatic conveying equipment is an essential tool for industries dealing with bulk materials. The design principles and components of such systems are carefully engineered to ensure efficient and reliable material transport. HeadPowder, with its expertise and commitment to quality, offers advanced solutions tailored to the specific needs of its clients. For businesses seeking reliable pneumatic conveying systems, HeadPowder is a trusted partner that provides innovative and durable equipment. Located in Shandong, China, HeadPowder continues to lead the industry in providing high-quality pneumatic conveying solutions for various applications.