

Small Bag Weighing and Feeding Pneumatic Conveying System Equipment: What It Is and Its Design Princ
Small bag weighing and feeding pneumatic conveying systems represent a specialized technology used in material handling and processing industries. These systems are designed to efficiently transfer bulk materials from one location to another while ensuring precise weight measurement and controlled feeding rates. The equipment is particularly valuable in applications where material accuracy and consistency are critical, such as in pharmaceutical, food, and chemical processing sectors.
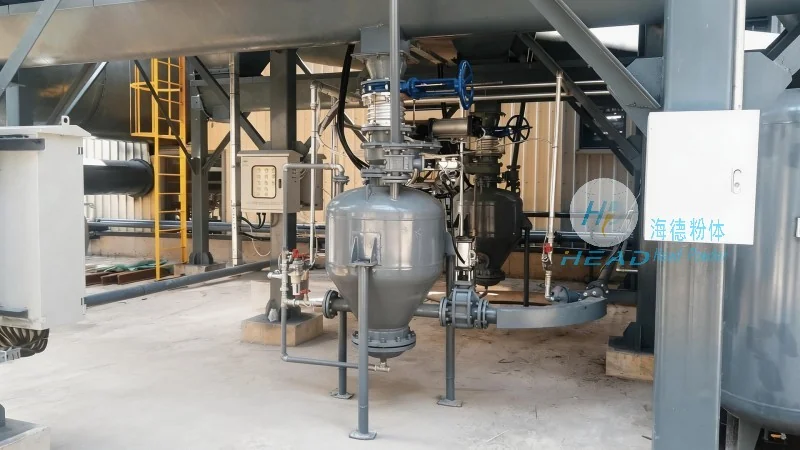
Introduction to Small Bag Weighing and Feeding Pneumatic Conveying Systems
The small bag weighing and feeding pneumatic conveying system is a sophisticated piece of equipment that integrates weighing technology with pneumatic conveying capabilities. It is typically used to handle materials in small bags, such as powders or granules, and transfer them to processing equipment or storage areas. The system operates by first weighing the contents of a bag, then feeding the material into a pneumatic conveyor for transport. This combination of functions makes it an essential tool for industries that require both accuracy and efficiency in material handling.
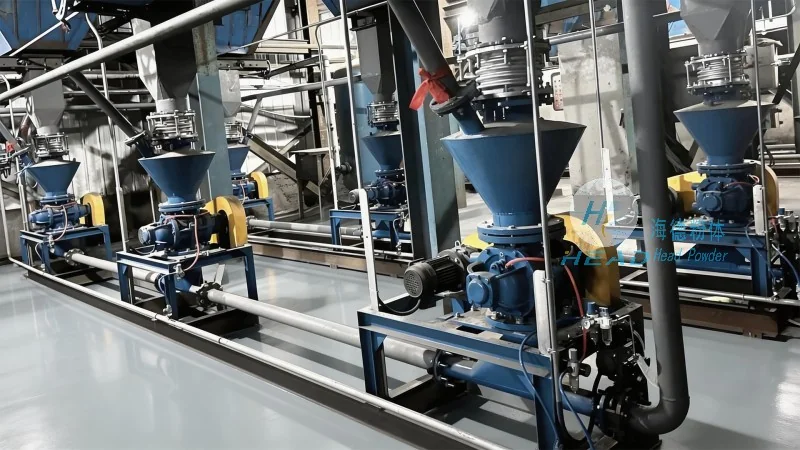
Key Components of the System
The core components of a small bag weighing and feeding pneumatic conveying system include a weighing hopper, a feeder mechanism, a pneumatic conveying line, and a control system. The weighing hopper is designed to hold the material from a small bag and accurately measure its weight. The feeder then dispenses the material at a controlled rate into the pneumatic conveying line. The pneumatic conveying line uses air pressure to transport the material to the desired destination. The control system manages the entire process, ensuring that the weighing and feeding operations are synchronized and that the material is transferred as per the set parameters.
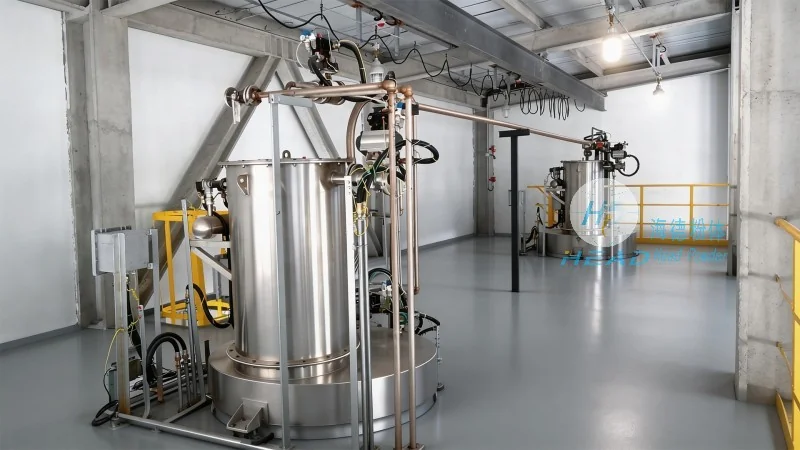
Design Principles and Operational Mechanisms
The design of the small bag weighing and feeding pneumatic conveying system is based on several key principles to ensure reliability and precision. First, the system must maintain a consistent air pressure and flow rate to achieve smooth material transport. Second, the weighing mechanism must be accurate and responsive, capable of measuring small variations in weight quickly. Third, the feeding mechanism must be able to handle a wide range of material properties, from fine powders to coarse granules, without clogging or damaging the equipment. The integration of these components allows the system to operate efficiently and reliably, even under varying conditions.
Application Scenarios and Benefits
Small bag weighing and feeding pneumatic conveying systems are widely used in various industries due to their versatility and efficiency. In the pharmaceutical industry, they are used to transfer active ingredients and excipients with high precision, ensuring that the final product meets strict quality standards. In the food industry, they help maintain hygiene and accuracy in handling ingredients, which is crucial for food safety. In the chemical industry, they enable the transfer of reactive materials with controlled rates, reducing the risk of accidents. The benefits of using such systems include improved material handling efficiency, reduced labor costs, and enhanced product quality through precise measurement and controlled feeding.
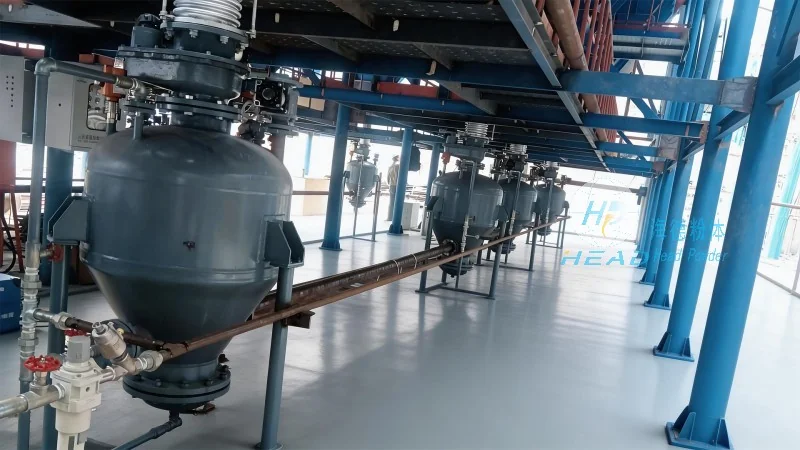
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of material handling equipment, including small bag weighing and feeding pneumatic conveying systems. The company is headquartered in Shandong, China, and has established itself as a trusted provider of high-quality industrial solutions. HeadPowder specializes in designing and manufacturing equipment tailored to meet the specific needs of various industries, ensuring that customers receive reliable and efficient solutions for their material handling challenges. The company's commitment to quality and innovation has made it a preferred choice for businesses seeking advanced material handling technologies.