

What is a Negative Pressure Powder Conveying System? What are its Design Principles?
For industries dealing with bulk powders, the efficient and safe transportation of materials is a critical operational challenge. A negative pressure powder conveying system, also known as a vacuum conveying system, offers a solution by utilizing a vacuum to draw powders from a source to a destination. This method is particularly advantageous for applications requiring gentle handling of delicate or abrasive powders, ensuring minimal product degradation and maintaining consistent quality throughout the process. The system operates by creating a low-pressure environment at the inlet, which pulls air and powder particles into the conveying line. This approach is widely used in sectors such as pharmaceuticals, food processing, and chemical manufacturing, where maintaining product integrity is essential.
The Design Principles of Negative Pressure Powder Conveying Systems
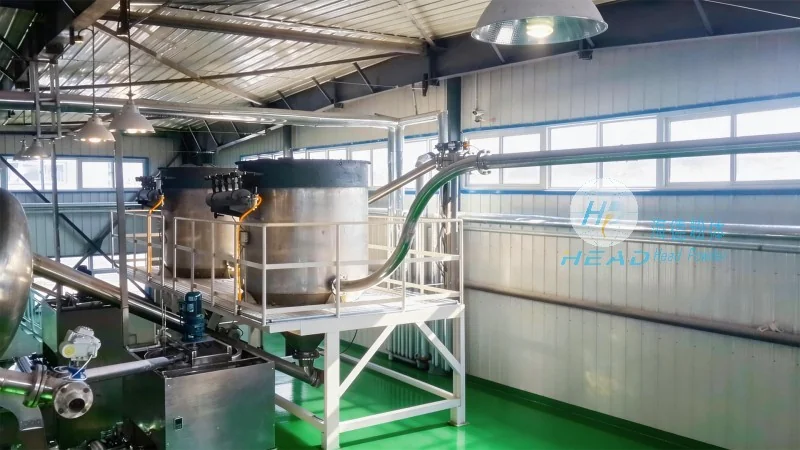
The core design of a negative pressure powder conveying system revolves around creating a vacuum at the inlet of the system. This vacuum is generated by a vacuum pump, which pulls air and the powder particles from the source container into the conveying line. The system typically includes several key components: a vacuum pump, a filter to separate the powder from the air, a receiver or destination vessel, and a conveying line. The design emphasizes the use of low air velocity to prevent particle attrition and ensure that the powder is transported without excessive stress. The system's layout can vary, with options for vertical, horizontal, or mixed configurations depending on the distance and layout of the material handling process. The choice of materials for the conveying line and components is also critical, often made from stainless steel or other corrosion-resistant materials to handle a wide range of powder types and prevent contamination. The design also incorporates pressure relief valves and safety interlocks to ensure operational safety and prevent over-pressurization.

HeadPowder: A Leader in Negative Pressure Powder Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a prominent manufacturer specializing in the design, development, and supply of advanced negative pressure powder conveying systems. With a strong presence in China, particularly in Shandong, the company leverages years of industry experience to deliver high-quality, reliable equipment tailored to the specific needs of various industries. HeadPowder's systems are engineered to meet stringent standards for efficiency, safety, and durability, ensuring that they can handle diverse powder characteristics while maintaining optimal performance. The company's commitment to innovation and customer satisfaction has positioned it as a trusted partner for businesses seeking effective powder handling solutions. HeadPowder's facilities in Shandong are equipped with state-of-the-art technology and skilled personnel, enabling the production of customized systems that meet the unique requirements of each client.
Key Advantages of Negative Pressure Powder Conveying Systems
Compared to positive pressure systems, negative pressure conveying offers several benefits. The primary advantage is the gentle handling of powders, which is essential for products that are sensitive to impact or compression. This method also reduces the risk of dust contamination and cross-contamination between different materials, as the powder is contained within the system. Additionally, negative pressure systems are often more energy-efficient, as they require less air volume and pressure to operate. The design allows for the safe and controlled transfer of powders over longer distances and varying elevations, making it suitable for complex material handling setups. These advantages make negative pressure powder conveying systems a preferred choice in pharmaceuticals, food processing, chemical manufacturing, and other industries where product integrity and safety are paramount. The systems are also designed to minimize noise and vibration, contributing to a safer and more comfortable working environment.
Applications and Industries Served by Negative Pressure Powder Conveying Systems
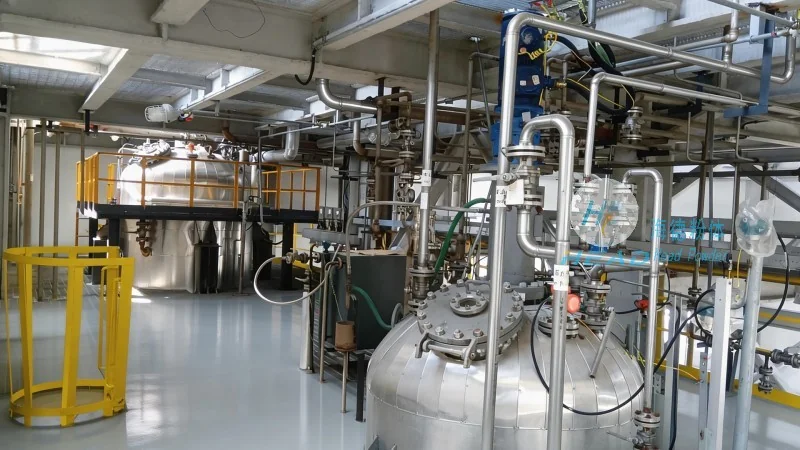
Negative pressure powder conveying systems are versatile and can be applied across a wide range of industries. In the pharmaceutical industry, these systems are used to transport active pharmaceutical ingredients (APIs) and excipients with precision, ensuring that the powders are handled without contamination or degradation. The food processing sector utilizes negative pressure conveying for handling powders like sugar, flour, and spices, maintaining the quality and safety of the final products. In chemical manufacturing, the systems are essential for transferring raw materials and intermediates, particularly those that are hazardous or sensitive to moisture. Other industries, such as cosmetics, ceramics, and agricultural products, also benefit from the gentle and efficient handling capabilities of these systems. The adaptability of negative pressure powder conveying systems makes them a valuable asset for any business dealing with bulk powders, providing a reliable solution for material transportation and processing.