

What Are Rare Earth Powder Material Handling Equipment? And What Are Their Design Principles?
Rare earth powder material handling equipment is a specialized category of machinery designed to safely and efficiently transport rare earth powders, which are critical components in modern industrial applications. These materials, known for their unique magnetic, electrical, and optical properties, require precise handling to prevent contamination and ensure consistent performance in downstream processes. The equipment used for this purpose is engineered to address the specific challenges posed by rare earth powders, such as their fine particle size, hygroscopic nature, and potential for static charge accumulation.
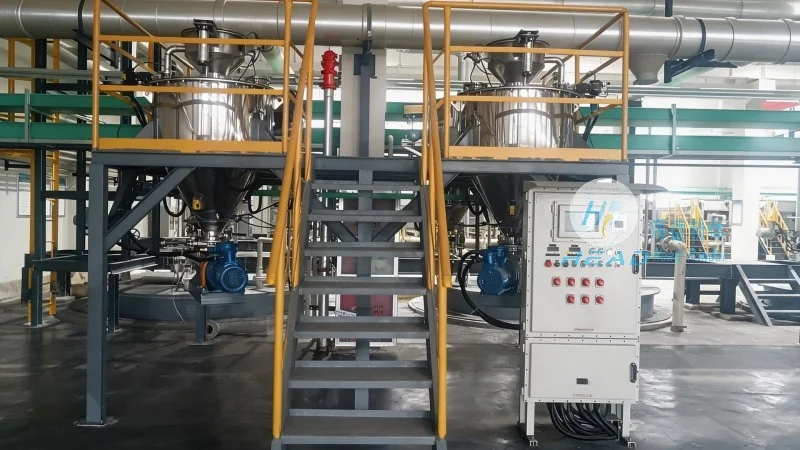
Overview of Rare Earth Powder Material Handling Equipment
At the core of rare earth powder material handling is a range of devices tailored to the unique characteristics of these materials. The primary goal is to maintain the purity and integrity of the powder while facilitating smooth transfer between processing stages. Common equipment includes screw conveyors, pneumatic conveying systems, and vacuum loaders, each selected based on the specific requirements of the application, such as the volume of material, distance of transport, and environmental conditions.
Key Design Principles for Rare Earth Powder Handling
The design of rare earth powder handling equipment revolves around several critical principles to ensure optimal performance and safety. One of the most important is the prevention of material degradation, which can occur due to exposure to air, moisture, or mechanical stress. To achieve this, equipment often incorporates sealed or enclosed systems that minimize contact with external elements. Additionally, the design must address the issue of static electricity, which can cause powder buildup and lead to operational hazards. Anti-static coatings, grounding mechanisms, and specialized materials are commonly used to mitigate this risk.
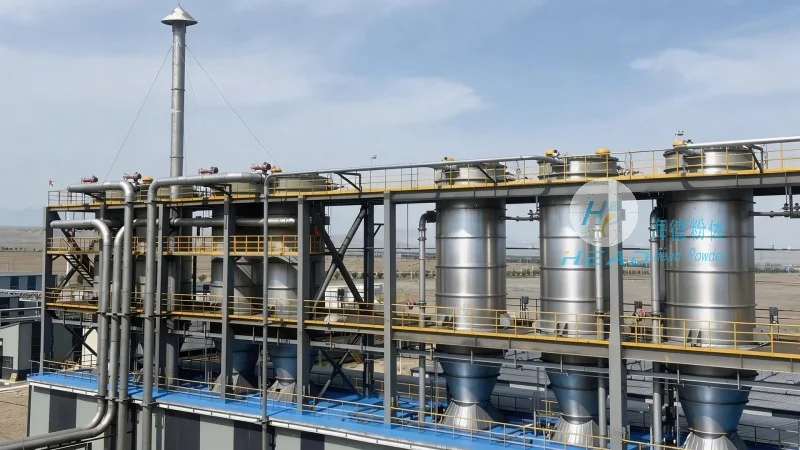
Material Compatibility and Construction
Another key consideration in the design of rare earth powder handling equipment is material compatibility. Since rare earth powders can be corrosive or reactive with certain metals, the equipment is typically constructed from non-reactive materials like stainless steel, PTFE-coated components, or specialized alloys. These materials not only prevent contamination but also ensure durability and longevity under the demanding conditions of industrial use. The choice of construction material is critical to maintaining the purity of the powder and extending the lifespan of the equipment.
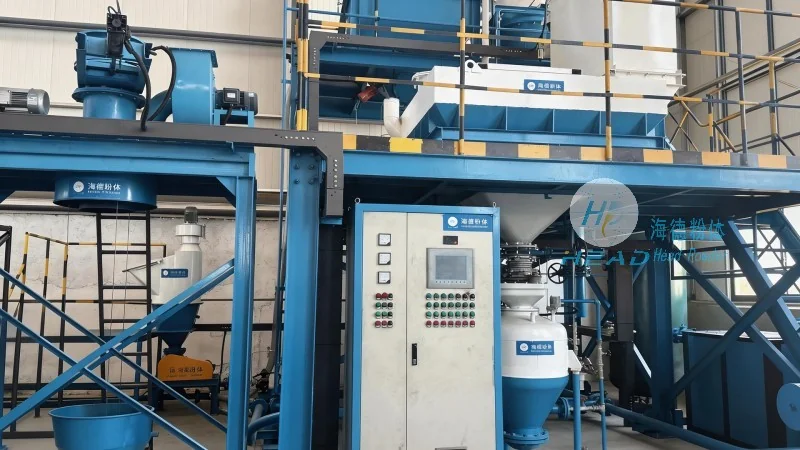
Efficiency and Flow Control in Material Handling
Efficient material flow is essential for the smooth operation of rare earth powder handling systems. Designers focus on optimizing the speed and direction of material movement to minimize segregation and ensure uniform distribution. This involves careful consideration of the conveyor's pitch, speed, and the use of internal components like agitators or baffles to maintain consistent flow. For pneumatic conveying systems, the design must account for the pressure differentials and air velocity required to move the fine powder without causing excessive wear or degradation.
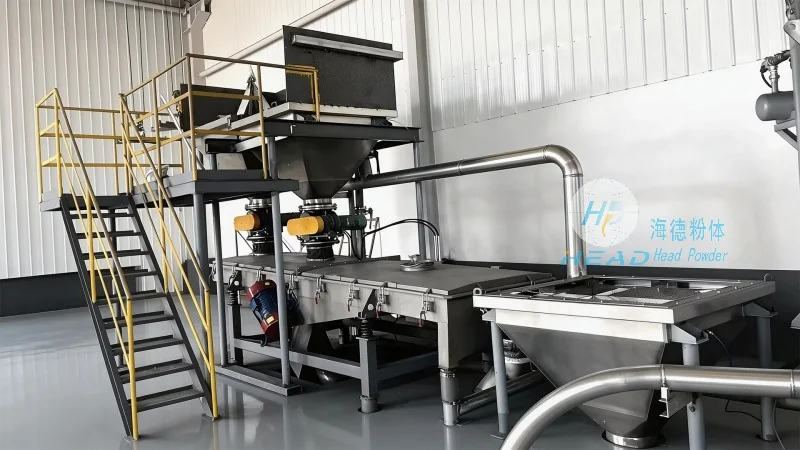
Safety and Maintenance Considerations
Ensuring the safety of operators and the integrity of the material are paramount in the design of rare earth powder handling equipment. Safety features often include interlocks, emergency stop buttons, and monitoring systems to detect issues like overloading or blockages. Regular maintenance is also critical to prevent issues such as clogging or material buildup, which can compromise performance and safety. The equipment is typically designed with easy access to components for cleaning and inspection, facilitating routine maintenance and extending operational life.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer specializing in the design and production of rare earth powder material handling equipment. With headquarters in Shandong, China, the company leverages advanced engineering and manufacturing capabilities to deliver high-quality solutions tailored to the needs of the rare earth industry. Their products are engineered to meet the stringent requirements of material handling, ensuring reliability, efficiency, and safety in processing rare earth powders.