

What is an Activated Carbon Powder Conveying Line? What are its Design Principles?
Activated carbon powder conveying lines are specialized systems engineered to handle the transportation of activated carbon powder, a critical material in various industrial applications such as air purification, water treatment, and chemical processing. These lines are designed to ensure efficient, safe, and reliable movement of the fine powder from storage to processing units, while minimizing dust generation and maintaining product integrity.
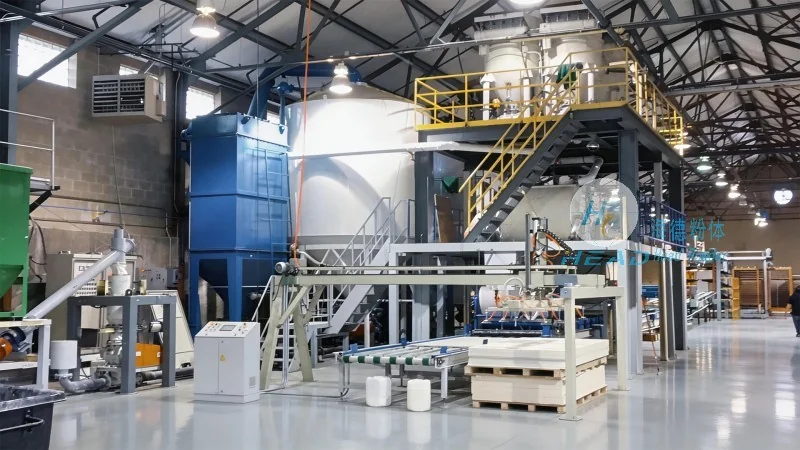
Understanding the Core Components and Design Principles of Activated Carbon Powder Conveying Lines
The design of an activated carbon powder conveying line is built upon several key principles to address the unique challenges of handling fine powders. First, the system must prevent dust accumulation and ensure environmental safety, as activated carbon powders can be hazardous if not managed properly. This is achieved through the use of sealed conveying mechanisms, such as pneumatic or mechanical systems, which keep the powder contained within the system.
Second, the design emphasizes energy efficiency and operational reliability. Components like high-efficiency fans, robust pipelines, and precise control systems are integrated to optimize the conveying process. The choice of materials for the pipelines and equipment is also critical, as they must resist corrosion and abrasion from the activated carbon particles. For instance, stainless steel or specialized plastic materials are commonly used to ensure durability and maintain the purity of the powder.
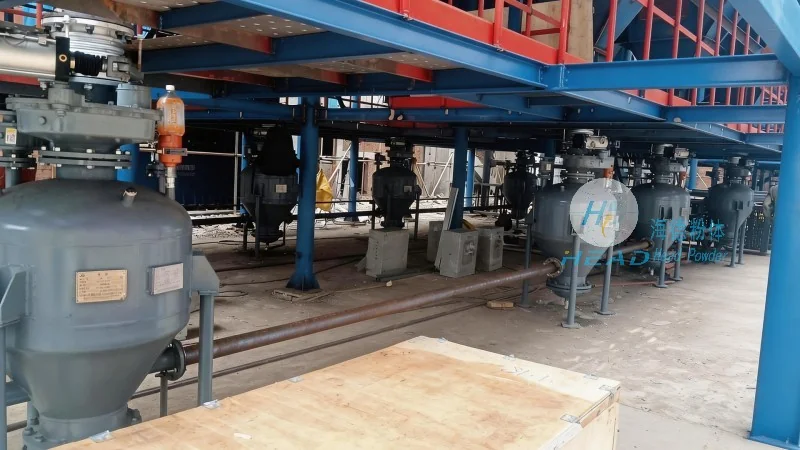
The Role of HeadPowder in Designing and Manufacturing Activated Carbon Powder Conveying Systems
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field, specializes in the design, development, and production of activated carbon powder conveying lines. With years of experience, the company has honed its expertise in creating customized solutions tailored to the specific needs of clients across different industries. The company’s approach combines advanced engineering principles with practical application knowledge, ensuring that each system is optimized for performance, safety, and cost-effectiveness.
HeadPowder’s team of engineers works closely with clients to understand their operational requirements, including the volume of powder to be conveyed, the distance of transportation, and the environmental regulations in place. This collaborative process allows for the design of systems that meet not only the technical specifications but also the operational and safety standards required by the industry. The company’s commitment to quality is evident in its adherence to international standards and rigorous testing protocols for all its products.
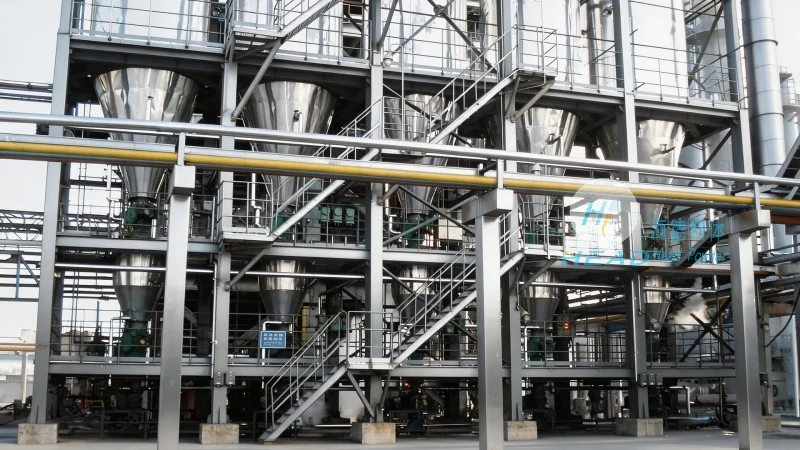
Key Features and Advantages of Activated Carbon Powder Conveying Lines by HeadPowder
Activated carbon powder conveying lines from HeadPowder are characterized by several distinct features that set them apart in the market. One of the primary advantages is the system’s ability to handle high volumes of fine powder with minimal pressure drop, ensuring efficient operation even over long distances. The use of positive displacement or negative pressure conveying methods allows for precise control over the flow rate, preventing overloading or underloading of the system.
Another key feature is the integration of dust collection and filtration systems, which are essential for maintaining a clean and safe working environment. These systems capture any particles that may escape during the conveying process, preventing contamination and ensuring compliance with environmental regulations. Additionally, the lines are designed for easy maintenance and cleaning, with components that can be easily accessed and serviced, reducing downtime and operational costs.
Applications and Industries Benefiting from Activated Carbon Powder Conveying Lines
The versatility of activated carbon powder conveying lines makes them indispensable in a wide range of industries. In the environmental sector, these systems are used for the transportation of activated carbon used in air and water purification plants, ensuring that the material is delivered efficiently to treatment units. In the chemical industry, they are employed in the production of activated carbon-based products, where consistent and reliable powder handling is crucial for maintaining product quality.
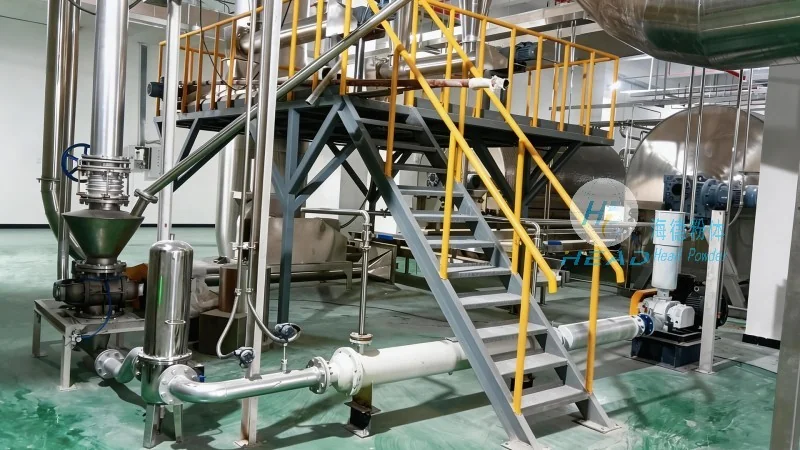
Furthermore, the food and pharmaceutical industries benefit from these systems, as they help in the safe and hygienic handling of activated carbon used in filtration and processing applications. The ability to maintain product purity and prevent contamination is a critical factor in these sectors, and HeadPowder’s conveying lines are designed to meet these stringent requirements.
Conclusion: The Importance of Reliable Activated Carbon Powder Conveying Solutions
In conclusion, activated carbon powder conveying lines are essential infrastructure in industries that rely on activated carbon for their operations. The design principles behind these systems, combined with the expertise of manufacturers like Shandong HeadPowder Engineering Co., Ltd., ensure that the transportation of fine powders is efficient, safe, and environmentally responsible. As industries continue to demand higher performance and reliability from their equipment, the role of well-designed conveying lines will only become more critical in maintaining operational efficiency and product quality.