

What is a Dry Pebble Powder Pneumatic Conveying Machine? What Are Its Design Principles?
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying systems, including the dry pebble powder pneumatic conveying machine. This equipment is specifically engineered to handle dry, granular, or powdery materials, such as pebbles, powders, and other fine particulates, ensuring efficient and reliable material transport in industrial settings.
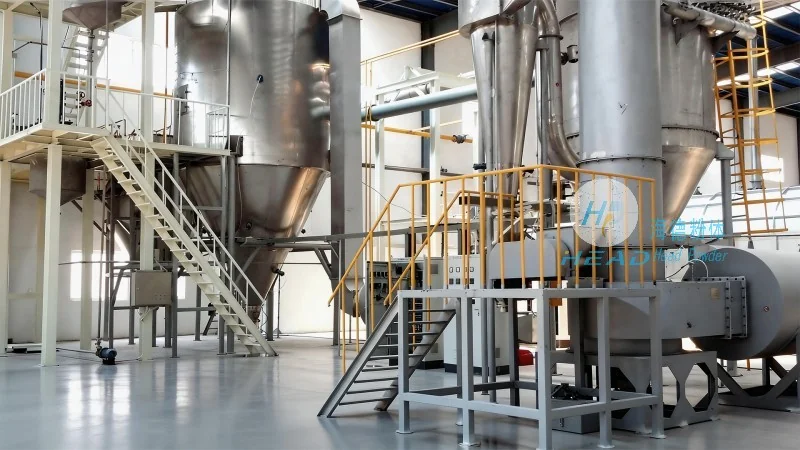
Understanding the Dry Pebble Powder Pneumatic Conveying Machine
The dry pebble powder pneumatic conveying machine is a sophisticated piece of industrial equipment designed to transport dry, non-abrasive or mildly abrasive powders and granules through a pressurized air system. Unlike traditional mechanical conveyors, this machine utilizes air pressure to move materials, eliminating the need for mechanical components that may wear out or require frequent maintenance. The system is particularly suitable for applications where material handling needs to be done in a clean, dust-free environment, or where long-distance transport is required without the risk of material degradation.
Key Components and Structure of the Machine
The dry pebble powder pneumatic conveying machine consists of several critical components that work in tandem to ensure efficient material transport. The main parts include the hopper, which serves as the material inlet, feeding the dry pebbles or powders into the system. The hopper is typically equipped with a feeder mechanism, such as a rotary valve or a screw feeder, to control the flow rate of the material. The conveying line, which is the central part of the machine, is made of durable materials like stainless steel or high-density polyethylene to withstand the abrasive nature of the pebbles and prevent material buildup or corrosion.
At the heart of the system is the air compressor, which generates the necessary pressure to move the material through the conveying line. The compressor is connected to a series of pipes and fittings that form the transport network. The line may include bends, elbows, and other fittings to direct the material to the desired destination. At the end of the line, a receiver or discharge hopper collects the material, allowing it to be discharged into a storage container or processing unit. The system also includes a filter and a dust collector to ensure that any fine particles are captured and returned to the system, maintaining a clean and safe working environment.
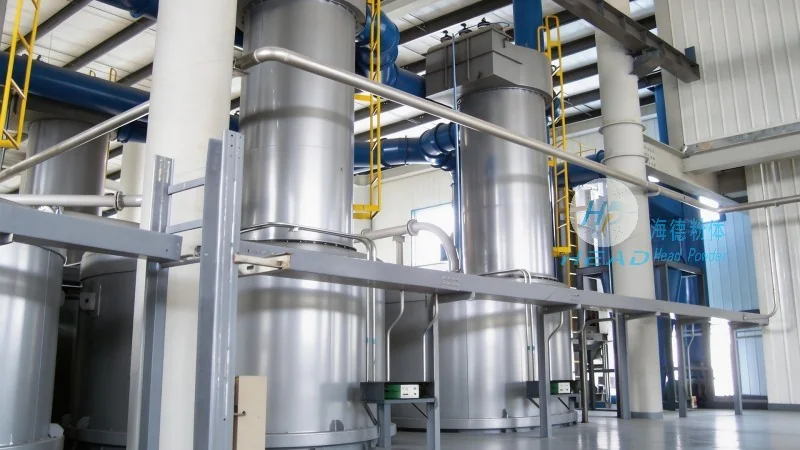
Design Principles and Operational Mechanism
The design principles of the dry pebble powder pneumatic conveying machine are centered around the efficient use of air pressure to move dry materials. The machine operates on the principle of pneumatic transport, where the material is suspended in a stream of air and carried through the conveying line. The key design considerations include the air velocity, which must be sufficient to lift and transport the material without causing excessive wear on the equipment, and the pressure drop, which determines the energy efficiency of the system. The machine is designed to handle a wide range of material sizes and densities, from fine powders to larger pebbles, by adjusting the air flow rate and pressure.
The operational mechanism involves the following steps: first, the dry pebbles or powders are fed into the hopper from a storage silo or a processing unit. The feeder mechanism then controls the flow rate, ensuring a consistent supply of material to the conveying line. The air compressor then generates the required pressure, and the air is introduced into the conveying line at the inlet. The material is then lifted and carried by the air stream, moving through the line to the discharge point. The air and material mixture is then separated at the receiver, where the material is collected and the air is filtered and returned to the system. This cycle repeats continuously, allowing for the continuous transport of materials over long distances.
Advantages and Applications of the Dry Pebble Powder Pneumatic Conveying Machine
The dry pebble powder pneumatic conveying machine offers several advantages over traditional mechanical conveyors, making it an ideal choice for many industrial applications. One of the primary advantages is its ability to transport materials in a clean and dust-free environment, which is crucial for industries such as food processing, pharmaceuticals, and electronics, where contamination must be minimized. The machine also eliminates the need for mechanical components like belts, chains, or screws, reducing the risk of material contamination and the need for frequent maintenance.
Another advantage is the flexibility of the system, which can be easily adjusted to handle different materials and transport distances. The machine can be configured with different hopper sizes, feeder types, and conveying line lengths to suit the specific needs of the application. Additionally, the system is compact and can be installed in a variety of locations, making it suitable for both new and existing industrial facilities.
The dry pebble powder pneumatic conveying machine is widely used in various industries, including mining, construction, food processing, and chemical manufacturing. In the mining industry, it is used to transport ore and pebbles from the mine to processing plants. In construction, it is used to transport sand, gravel, and other construction materials to job sites. In food processing, it is used to transport flour, sugar, and other dry ingredients to processing units. In chemical manufacturing, it is used to transport powders and granules to reactors and other processing equipment.
Conclusion
The dry pebble powder pneumatic conveying machine is a highly efficient and reliable piece of industrial equipment designed to transport dry materials in a clean and safe manner. With its advanced design principles and operational mechanism, the machine offers several advantages over traditional mechanical conveyors, making it an ideal choice for many industrial applications. HeadPowder, with its expertise in pneumatic conveying systems, provides high-quality machines that meet the specific needs of its customers, ensuring efficient and reliable material transport in various industrial settings.