

Working Principle and Features of Gelatin Pneumatic Conveying Equipment
For industrial applications involving gelatin, efficient and reliable material handling is crucial. One of the key technologies in this field is the gelatin pneumatic conveying machine, which offers a solution for transporting gelatin in a controlled manner. This article explores the working principle and key features of such equipment, providing insights into how it operates and why it is a preferred choice in the industry.
Understanding the Working Principle of Gelatin Pneumatic Conveying Machines
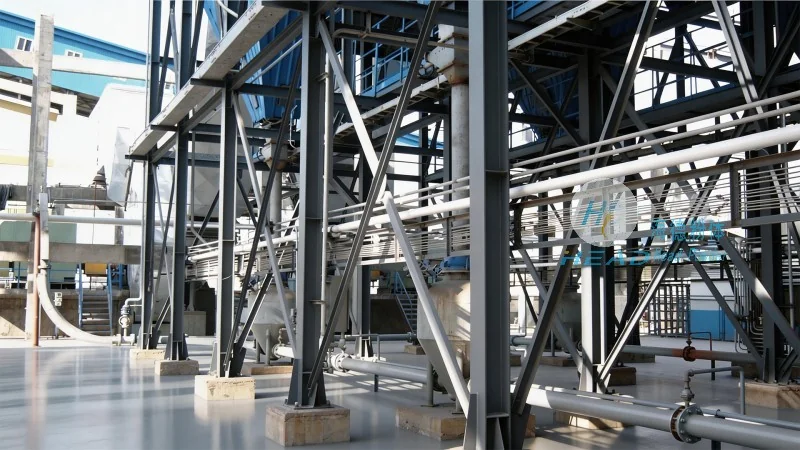
The core function of a gelatin pneumatic conveying machine is to transport gelatin powder or granules through a pipeline using air pressure. The process typically involves several key components, including a hopper for material storage, a conveyor tube, a blower or air compressor to generate the necessary airflow, and a control system to regulate the operation. The material is fed from the hopper into the conveyor tube, where it is mixed with the air stream. The air pressure pushes the gelatin particles through the pipeline to the destination point, such as a storage silo or processing unit. The system may use either positive pressure (where air is forced into the system) or negative pressure (where air is drawn out), depending on the specific application and the distance the material needs to travel.
Key Features of Gelatin Pneumatic Conveying Equipment
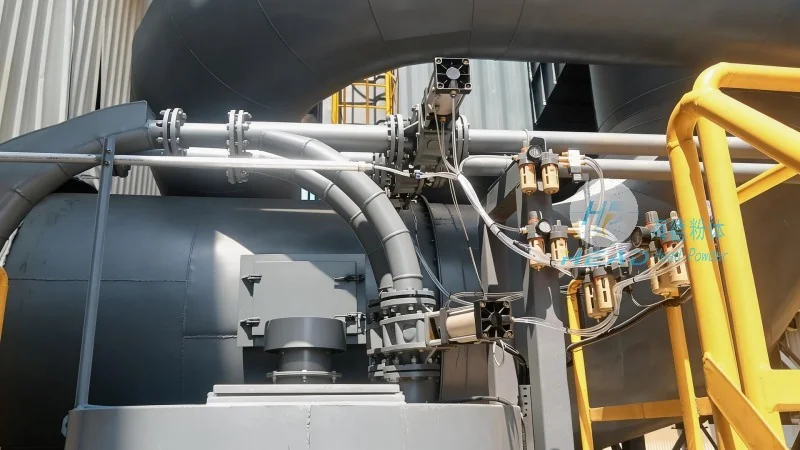
Several features make gelatin pneumatic conveying machines particularly suitable for handling gelatin. Firstly, they provide a dust-free and hygienic environment, which is essential for food-grade materials like gelatin. The enclosed system prevents contamination and ensures compliance with industry standards. Secondly, these machines offer high efficiency in terms of material transport, with minimal loss and consistent flow rates. This is achieved through precise control of air pressure and material feed, which can be adjusted based on the specific requirements of the process. Thirdly, the equipment is designed for easy maintenance and cleaning, with components that can be disassembled and sanitized to maintain hygiene standards. Additionally, the system can handle different forms of gelatin, including powder, granules, or even liquid gelatin under certain conditions, providing flexibility in material handling. The use of stainless steel and other food-grade materials in the construction of the machine further enhances its suitability for handling sensitive products like gelatin.
Company Information: Shandong HeadPowder Engineering Co., Ltd.
As a leading manufacturer in the field, Shandong HeadPowder Engineering Co., Ltd. specializes in the design, production, and supply of pneumatic conveying equipment tailored for various industrial applications. With a focus on quality and innovation, the company provides customized solutions that meet the specific needs of clients in the food and pharmaceutical industries. HeadPowder's expertise in material handling technology ensures that their gelatin pneumatic conveying machines are built to the highest standards, offering reliability, efficiency, and durability. The company is located in Shandong, China, and has established a strong presence in the industry with its commitment to customer satisfaction and product excellence. The company's comprehensive support, from design and installation to after-sales service, ensures that clients receive reliable and effective solutions for their material handling needs.
Conclusion: The Advantages of Using Gelatin Pneumatic Conveying Machines
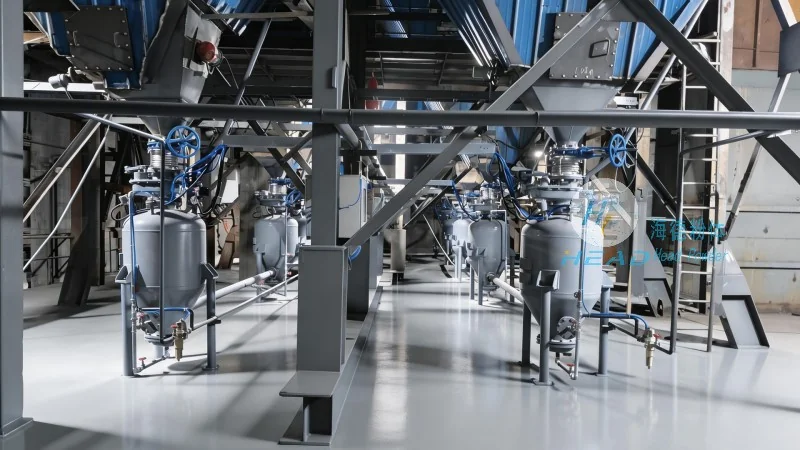
In conclusion, gelatin pneumatic conveying machines represent an advanced solution for the efficient and hygienic transport of gelatin in industrial settings. By understanding the working principle and leveraging the key features of such equipment, businesses can enhance their material handling processes, improve product quality, and ensure compliance with industry regulations. With the support of experienced manufacturers like Shandong HeadPowder Engineering Co., Ltd., companies can access reliable and customized solutions that meet their specific requirements, contributing to improved operational efficiency and overall success in their respective industries.