

Working Principle and Features of Bulk Bag Powder Pneumatic Conveying Systems
Welcome to HeadPowder, a leading engineering company based in Shandong, China. Specializing in advanced material handling solutions, our expertise lies in the design and implementation of bulk bag powder pneumatic conveying systems. These systems are critical for efficiently transporting bulk powders from storage to processing units, ensuring minimal dust, high transfer rates, and operational reliability.
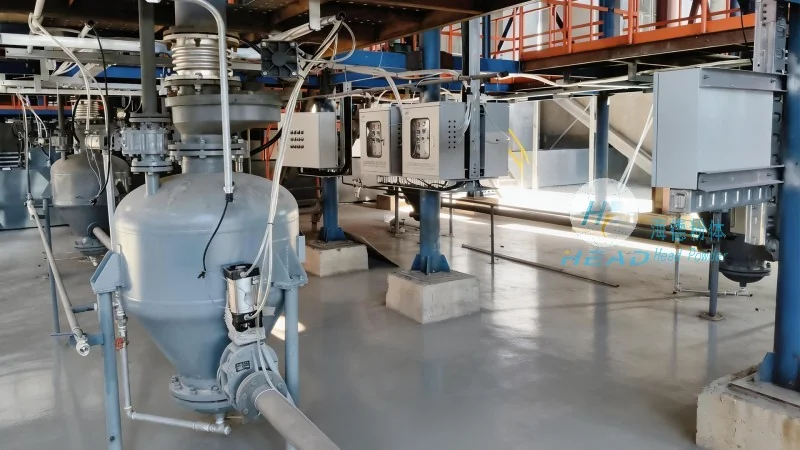
Introduction to Bulk Bag Powder Pneumatic Conveying Systems
Bulk bag powder pneumatic conveying systems are engineered to handle the transportation of dry powders, granules, and other bulk materials from bulk bags (also known as super sacks or big bags) into processing equipment or storage silos. This technology combines the advantages of bulk bag storage with the efficiency of pneumatic conveying, offering a seamless solution for industries such as food, pharmaceuticals, chemicals, and mining. The system's design focuses on safety, efficiency, and adaptability to various material characteristics and operational requirements.
The Working Principle of Bulk Bag Powder Pneumatic Conveying Systems
The core of a bulk bag powder pneumatic conveying system is the pneumatic transport mechanism, which utilizes air pressure to move material through a pipeline. The process typically involves several key steps: first, the bulk bag is positioned at the loading station, where a discharge spout or valve is opened to allow the material to flow into the conveying line. Air is then introduced into the system, either under pressure (positive pressure) or by creating a vacuum (negative pressure), depending on the system design. The air and material mixture travels through the pipeline to the discharge point, where the material is separated from the air and deposited into the target container or processing equipment. The air is then filtered and recycled back into the system to maintain efficiency and reduce environmental impact.
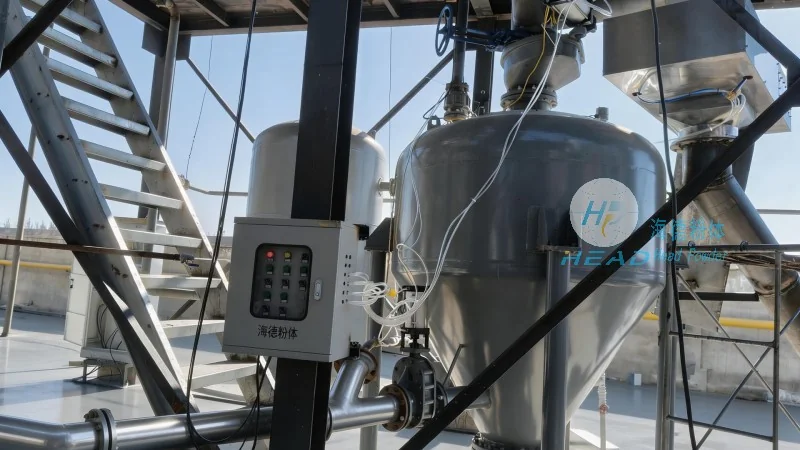
Key Components and Their Functions
Several critical components work in tandem to ensure the smooth operation of a bulk bag powder pneumatic conveying system. These include: bulk bag unloaders or discharge units, which facilitate the controlled release of material from the bag; air blowers or vacuum pumps, which generate the necessary pressure or vacuum for material transport; conveying pipelines, which provide the path for material and air; dust filters or cyclones, which separate the material from the air stream and collect it for reuse or disposal; and control systems, which regulate the flow of material and air to maintain optimal performance. Each component is designed to handle the specific characteristics of the material being transported, such as particle size, moisture content, and flowability.
Advantages of Bulk Bag Powder Pneumatic Conveying Systems
Bulk bag powder pneumatic conveying systems offer numerous advantages over traditional material handling methods. One of the most significant benefits is the reduction of dust exposure, which is crucial for maintaining a safe and healthy working environment, especially in industries dealing with hazardous or fine powders. The enclosed system also minimizes product contamination, ensuring that the material remains pure and free from external particles. Additionally, these systems provide high transfer rates, allowing for rapid and continuous material movement, which can improve overall production efficiency. The flexibility of the system allows for easy integration with existing processing lines and can be adjusted to accommodate different material types and quantities. Furthermore, the use of bulk bags offers cost-effective storage and transportation of materials, as they are lightweight, durable, and can hold large volumes of material compared to traditional containers.
Features and Customization Options
HeadPowder's bulk bag powder pneumatic conveying systems are designed with a range of features to meet the diverse needs of our clients. These features include adjustable air pressure and flow rates to optimize material transfer, automatic control systems for unattended operation, and modular designs that allow for easy expansion or modification. The systems can be customized to handle a wide variety of materials, from fine powders like cement and flour to bulkier granules like plastic resin and agricultural products. The company also offers options for different conveying methods, such as positive pressure, negative pressure, or a combination of both, depending on the specific requirements of the application. Additionally, the systems are equipped with safety features, including pressure relief valves and emergency shut-off mechanisms, to prevent accidents and ensure operational safety.
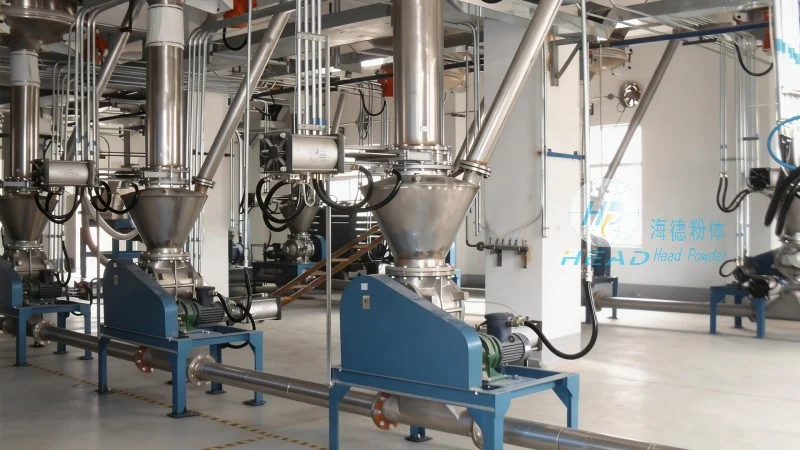
Applications and Industries
Bulk bag powder pneumatic conveying systems are widely used across various industries due to their versatility and efficiency. In the food and beverage industry, these systems are used to transport ingredients like flour, sugar, and spices from bulk bags to processing equipment, ensuring a clean and hygienic transfer process. The pharmaceutical industry relies on these systems for the handling of active pharmaceutical ingredients (APIs) and other sensitive materials, where contamination control is paramount. The chemical industry uses them to transport raw materials such as powders and granules, while the mining and mineral processing sectors utilize them for the handling of ores and other bulk materials. Additionally, the agricultural sector benefits from these systems for the transport of fertilizers and other agricultural products. In each of these applications, the bulk bag powder pneumatic conveying system provides a reliable and efficient solution for material handling.
Conclusion and Company Commitment
At HeadPowder Engineering Co., Ltd., we are committed to providing high-quality, reliable bulk bag powder pneumatic conveying systems that meet the evolving needs of our clients. Our systems are designed with advanced technology and engineering expertise to ensure optimal performance, safety, and efficiency. By leveraging our experience and innovation, we help our clients improve their material handling processes, reduce operational costs, and enhance overall productivity. Whether you are in the food, pharmaceutical, chemical, or mining industry, our bulk bag powder pneumatic conveying systems offer a superior solution for your material transport needs. Contact us today to learn more about how our systems can benefit your operations.